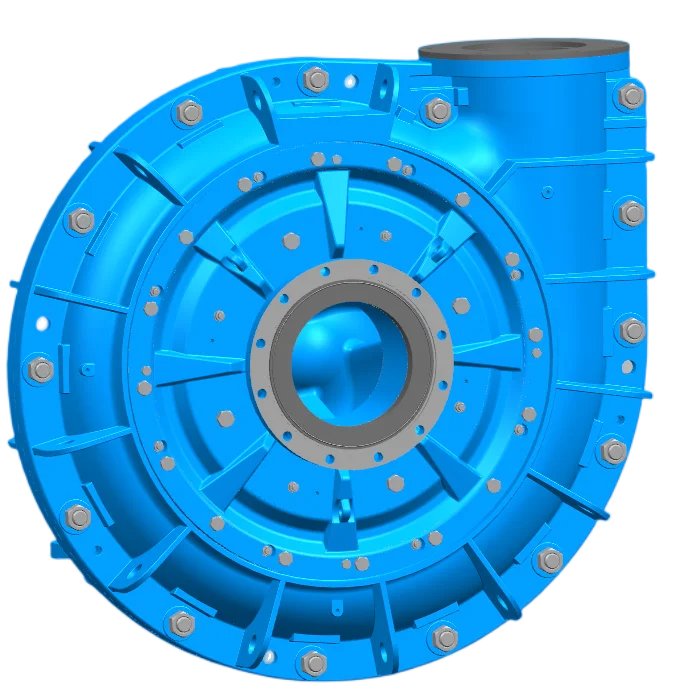
In the demanding landscape of mineral processing and industrial slurry management, the efficiency of fluid transport determines the overall productivity of a plant. Among the specialized equipment used, the froth pump stands as a critical component designed to handle the complex mixtures of air and solids typically found in flotation cells. These machines are engineered to transport highly aerated slurries without losing prime or suffering from cavitation, ensuring a steady flow of material through the processing circuit.
The global demand for efficient mineral extraction has pushed the evolution of pumping technology toward more compact and durable designs. Modern industrial operations require equipment that minimizes footprint while maximizing uptime, leading to the development of specialized horizontal configurations. By integrating advanced materials and optimized hydraulics, the industry has moved toward solutions that reduce energy consumption and simplify the grueling maintenance cycles associated with abrasive slurry handling.
Understanding the technical nuances of a froth pump is essential for engineers looking to optimize their operational costs. Whether managing mine tailings or chemical processing fluids, selecting a pump that balances wear resistance with hydraulic efficiency can significantly extend the mean time between failures (MTBF). This guide explores the technical specifications, advantages, and applications of these specialized machines in today's industrial environment.

The Technical Design of Horizontal Froth Pumps
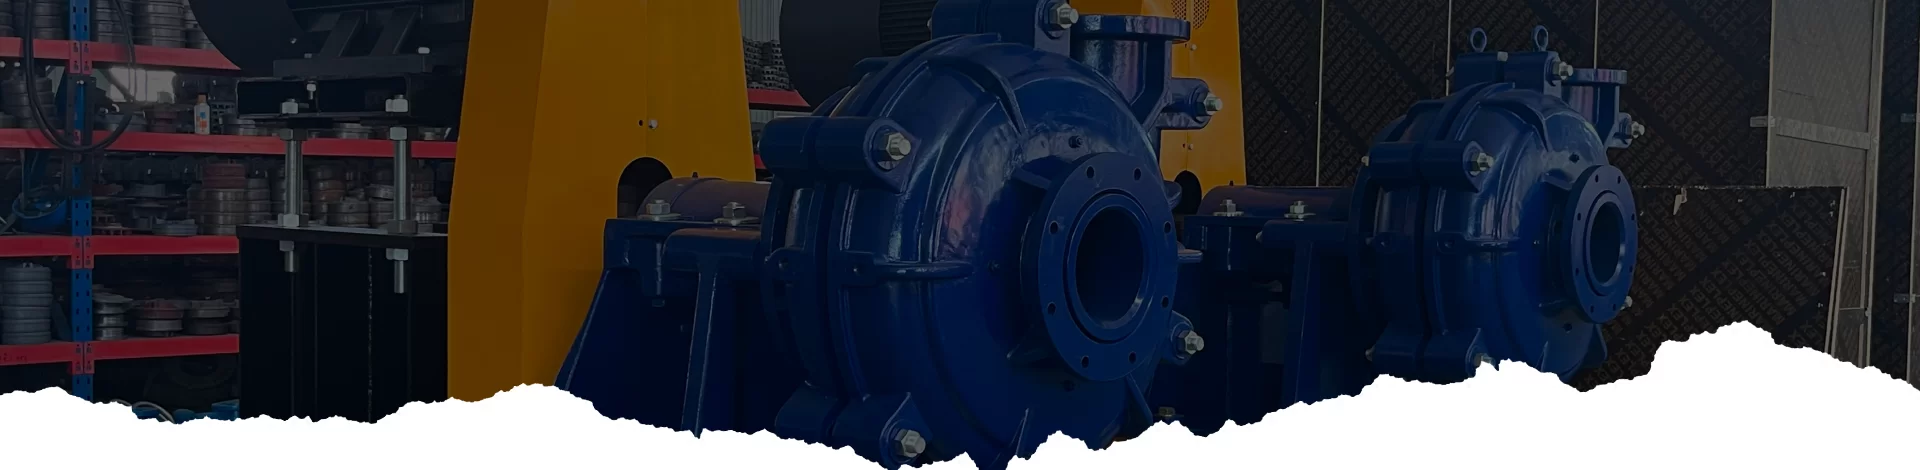
The CNSME® LF series represents a significant shift in the design of the froth pump, prioritizing a lightweight horizontal configuration. Unlike traditional vertical units that require deep pits and extensive overhead structures, the horizontal design allows for a more compact equipment arrangement. This transition not only saves valuable floor space in the plant but also lowers the center of gravity for the entire installation, enhancing overall stability.
Beyond spatial advantages, the horizontal architecture inherits the proven reliability of double casing slurry pumps. This design ensures that the pump can maintain a consistent vacuum and flow rate even when dealing with high concentrations of air bubbles. The streamlined flow path minimizes turbulence, which is critical for preventing the collapse of the froth phase before it reaches the discharge point, thereby maintaining the integrity of the mineral concentrate.
Material Composition and Wear Resistance
Durability in a froth pump is primarily determined by the materials used in the wet-end components. To combat the dual threats of abrasion from solid particles and corrosion from chemical reagents, the 4E-AHF model utilizes high-grade corrosion-resistant rubber or specialized metal alloys. The choice between these materials depends on the specific slurry chemistry and the size of the abrasive particles being transported.
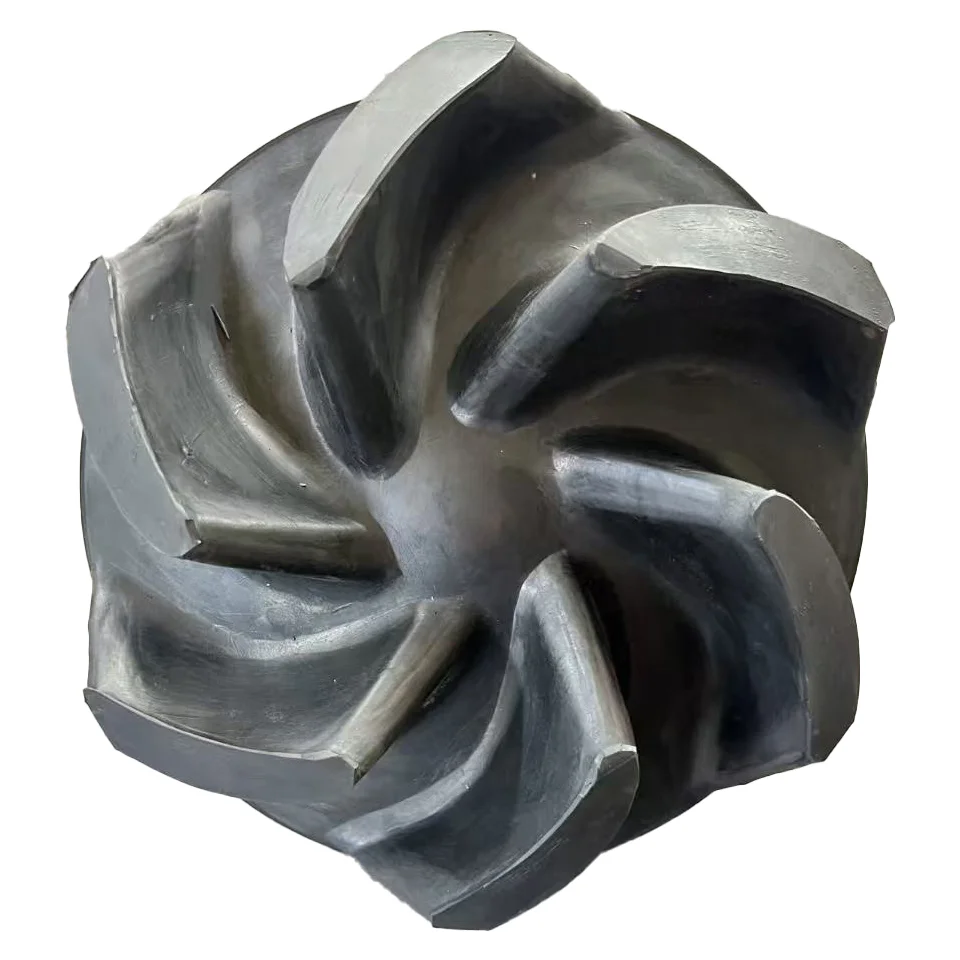
The impeller, which is the most vulnerable part of the pump, is available in either wear-resistant high chromium metal or rubber. High chromium alloys are ideal for high-impact, coarse-particle environments where hardness is paramount, while rubber impellers offer superior performance in finer, more corrosive slurries. This versatility ensures that the pump can be tailored to the specific mineralogy of the site.
By optimizing the metallurgy and polymer science of these components, the equipment achieves a longer service life. This reduces the frequency of shutdowns for liner replacements, which is one of the highest costs in slurry management. The strategic use of materials ensures that the pump maintains its hydraulic profile for a longer period, preventing the efficiency drops that typically occur as internals wear down.
Operational Efficiency and Space Optimization
One of the primary drivers for adopting a horizontal froth pump is the drastic reduction in installation complexity. By eliminating the need for deep sumps required by vertical models, operators can implement more flexible piping layouts. This agility allows plants to expand or modify their processing lines without the need for massive civil engineering projects or costly excavation.
Efficiency is not just about space; it is also about power. The LF horizontal series is engineered for low power consumption while maintaining a high discharge capacity. This is achieved through an optimized impeller geometry that reduces internal recirculation and friction losses. For large-scale operations, the cumulative energy savings from using a high-efficiency froth pump can be substantial, impacting the overall carbon footprint of the facility.
Furthermore, the reliable operation of these pumps ensures that the flotation process remains balanced. Inconsistent flow from a failing pump can lead to "surging" in the flotation cells, which disrupts the air-to-liquid ratio and reduces the recovery rate of the target mineral. By providing a stable, low-pulsation flow, the horizontal froth pump directly contributes to the quality of the final concentrate.
Comparative Performance Metrics
When evaluating the performance of different pumping strategies, it is clear that the horizontal approach offers a superior balance of accessibility and throughput. The ability to handle flow rates up to 4550m³/hr makes it suitable for everything from boutique mining operations to massive global industrial complexes. The versatility in discharge sizes, ranging from 50mm to 550mm, allows for precise scaling based on the production volume.
The critical metric for any froth pump is its ability to handle "frothy" media without losing prime. While standard slurry pumps often struggle with air entrainment, these specialized units are designed to maintain a steady head of up to 37m, ensuring that the material moves efficiently from the cell to the thickener or the next stage of processing.
Performance Efficiency Comparison of Froth Pump Configurations
Global Industrial Applications
The application of the froth pump spans across various continents, particularly in regions with heavy mining activity such as Australia, Chile, and Canada. In these remote industrial zones, the ease of installation provided by the horizontal LF series is a major advantage, as it reduces the need for heavy construction machinery and specialized onsite civil engineering teams.
Beyond mining, these pumps are utilized in chemical processing plants where aerated slurries are common during the separation of organic and inorganic compounds. The ability to customize the wet-end materials means that a single pump design can be adapted for highly acidic environments or for transporting abrasive mineral concentrates, making it a versatile tool for global industrial engineers.
Maintenance and Installation Simplification
Maintenance is often the Achilles' heel of slurry pumping systems. However, the horizontal froth pump is designed to simplify these processes. Because the pump is positioned at ground level rather than deep in a sump, technicians have immediate access to the casing and impeller. This eliminates the need for hazardous confined-space entry, significantly improving workplace safety.
The double casing structure allows for the replacement of internal liners without needing to dismantle the entire piping system. This "plug-and-play" approach to maintenance means that downtime is reduced from days to hours. By simplifying the mechanical path to the wear parts, CNSME® has ensured that the 4E-AHF model remains operational for longer periods.
Furthermore, the lightweight nature of the LF series makes initial installation more straightforward. The reduced weight reduces the requirements for heavy-duty support foundations, allowing for faster commissioning. When combined with the reliable operation and low power consumption, the total cost of ownership is significantly lowered over the life of the equipment.
Technical Parameter Analysis
To fully appreciate the capability of a modern froth pump, one must look at the hard data. The range of discharge sizes from 2 inches to 22 inches ensures that the pump can be matched to any flow requirement. With a maximum flow rate of 4550m³/hr, these pumps can handle the output of multiple flotation cells simultaneously, streamlining the plant's hydraulic circuit.
The head capacity of up to 37m is specifically tuned for the low-density, high-volume nature of froth slurries. Unlike high-pressure pumps used for tailings disposal, the froth pump focuses on maintaining volume and preventing air separation. This specialized hydraulic profile ensures that the "froth" remains as a stable mixture during transport.
By analyzing the correlation between impeller material and flow efficiency, operators can optimize their pump selection. For instance, a rubber impeller might offer better efficiency in low-pressure, high-corrosion scenarios, whereas high chrome is the gold standard for maximum durability in abrasive environments.
Core Technical Specifications of LF Horizontal Froth Pumps
| Model Variant |
Material Type |
Max Flow (m³/hr) |
Max Head (m) |
| LF-Small |
Natural Rubber |
500 |
25 |
| LF-Medium |
High Chrome |
1500 |
30 |
| LF-Large |
Polyurethane |
3000 |
35 |
| LF-Extra Large |
High Chrome |
4550 |
37 |
| LF-Custom A |
Rubber Lined |
2000 |
28 |
| LF-Custom B |
Stainless Steel |
1200 |
32 |
FAQS
Horizontal froth pumps offer a much smaller footprint and eliminate the need for deep sumps, which drastically reduces civil engineering costs. They also provide significantly easier access for maintenance, as technicians do not need to enter confined spaces to service the impeller or liners, thereby improving safety and reducing downtime.
The choice depends on your slurry characteristics. High chromium metal impellers are best for highly abrasive, coarse-particle slurries where hardness and impact resistance are critical. Rubber impellers are preferred for finer particles and corrosive chemical environments where flexibility and corrosion resistance are more important than extreme hardness.
Yes, the CNSME® LF series is designed for scalability. It can handle discharge sizes from 50mm up to 550mm, with maximum flow capacities reaching up to 4550m³/hr (20,000 GPM), making it suitable for the largest industrial flotation circuits in the world.
Unlike standard slurry pumps, these are specifically engineered with a hydraulic profile that can handle high air-to-liquid ratios. The internal structure is optimized to maintain a consistent flow of aerated slurry, preventing the air bubbles from coalescing and creating an air lock that would otherwise stop the pump.
The LF horizontal series can achieve a head of up to 37 meters (120 feet). This is specifically designed to efficiently move froth concentrate from the flotation cells to the next stage of the process without requiring excessive energy or risking the breakdown of the froth phase.
Yes, by selecting the corrosion-resistant rubber material for the wet-end parts, these pumps can be used in environments with aggressive chemical reagents. The variety of material options allows the pump to be tailored to the specific pH and chemical composition of the slurry.
Conclusion
The adoption of a horizontal froth pump represents a strategic upgrade for any mineral processing facility. By combining the durability of high-chrome and rubber materials with a space-saving horizontal design, these pumps solve the dual challenges of operational wear and installation complexity. From their ability to handle massive flow rates of 4550m³/hr to their simplified maintenance protocols, they ensure that the critical transport of aerated slurries is achieved with maximum reliability and minimum energy expenditure.
Looking forward, the trend toward more automated and sustainable mining will only increase the demand for high-efficiency pumping solutions. Investing in equipment that reduces downtime and optimizes power consumption is no longer optional but a necessity for remaining competitive in the global market. We recommend a detailed hydraulic analysis of your current circuit to determine the optimal material and size configuration for your specific application. Visit our website: www.qualityslurrypump.com