In the demanding landscape of industrial mining and mineral processing, maintaining peak operational efficiency is a constant struggle. The search for a reliable warman slurry pump replacement often stems from the need to reduce unplanned downtime and combat the aggressive wear caused by abrasive slurries. When critical pumping systems fail, the ripple effect on production can be financially devastating, making the selection of high-performance alternative components a strategic necessity for plant managers.
Globally, the shift toward more sustainable and cost-effective mining operations has put a spotlight on the longevity of wear parts. By optimizing the materials used in a warman slurry pump replacement, industries can significantly extend the mean time between maintenance (MTBM) and lower the total cost of ownership. This is particularly vital in remote industrial zones where logistics for spare parts are complex and expensive, requiring components that can withstand extreme conditions without frequent intervention.
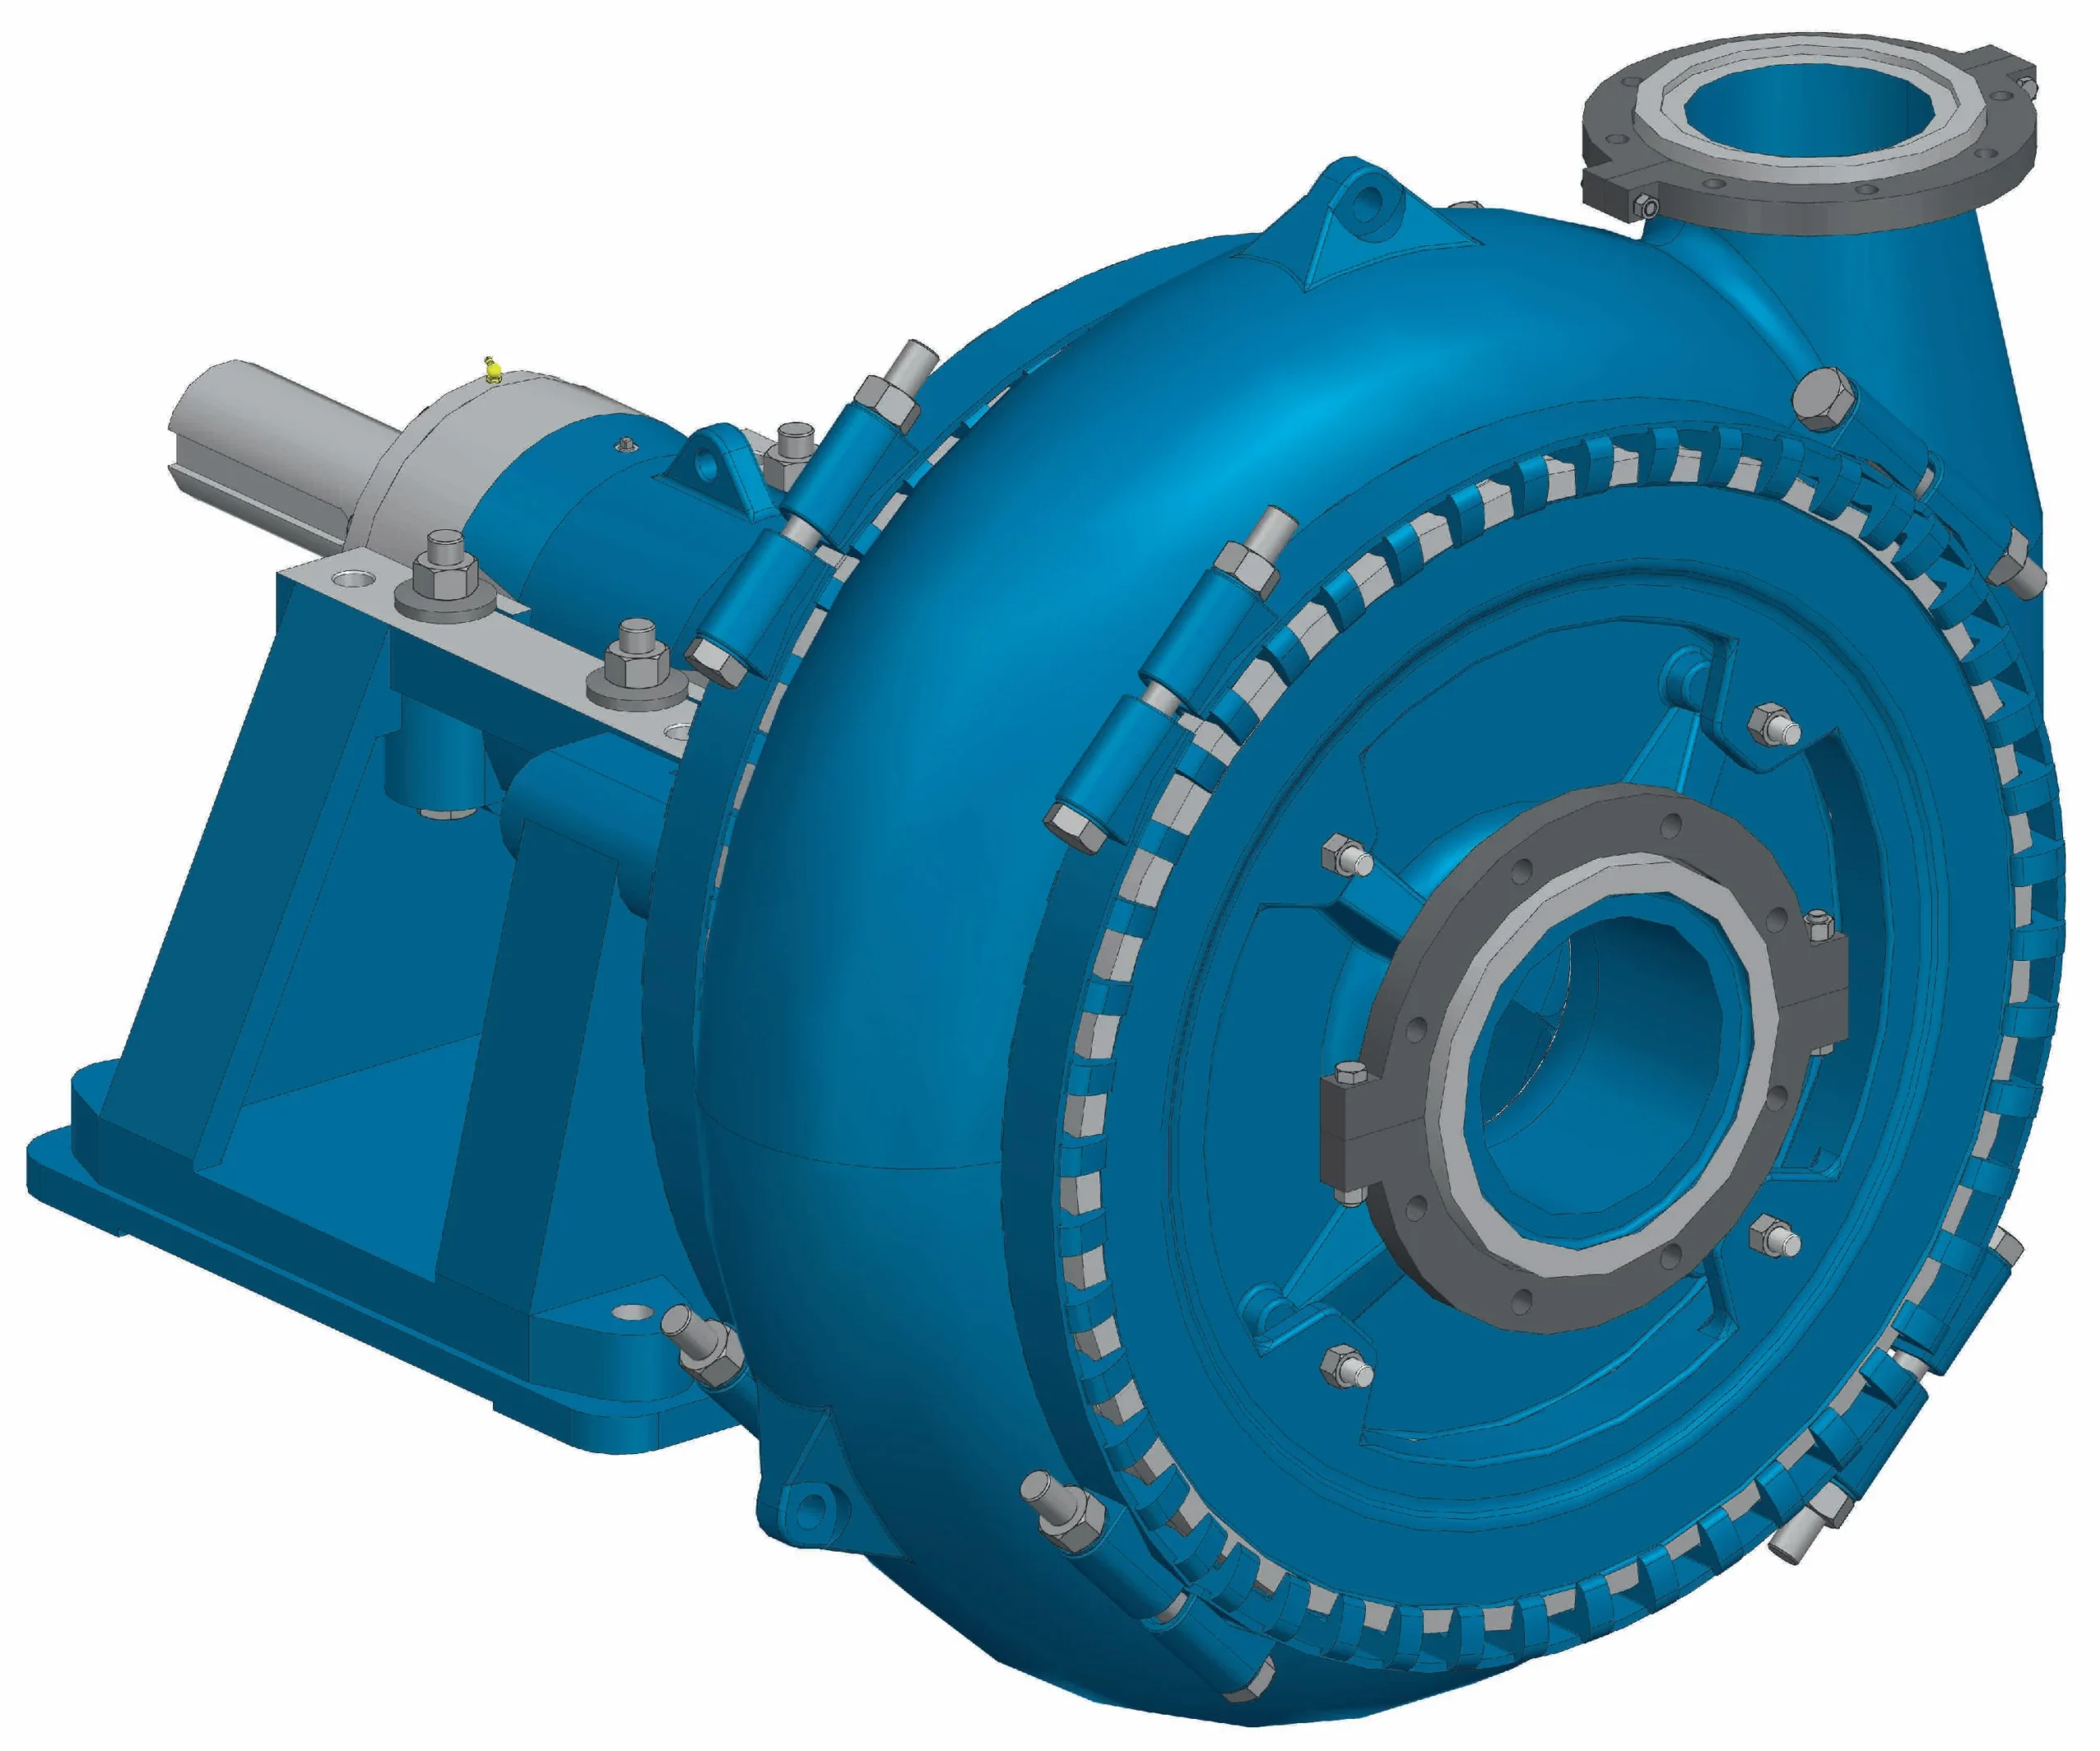
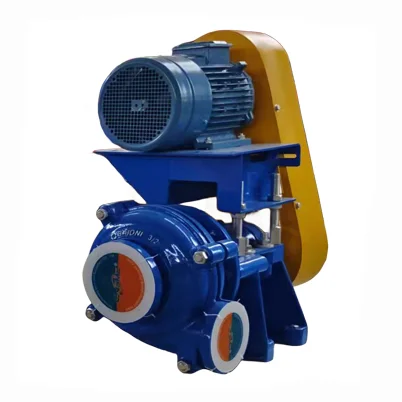
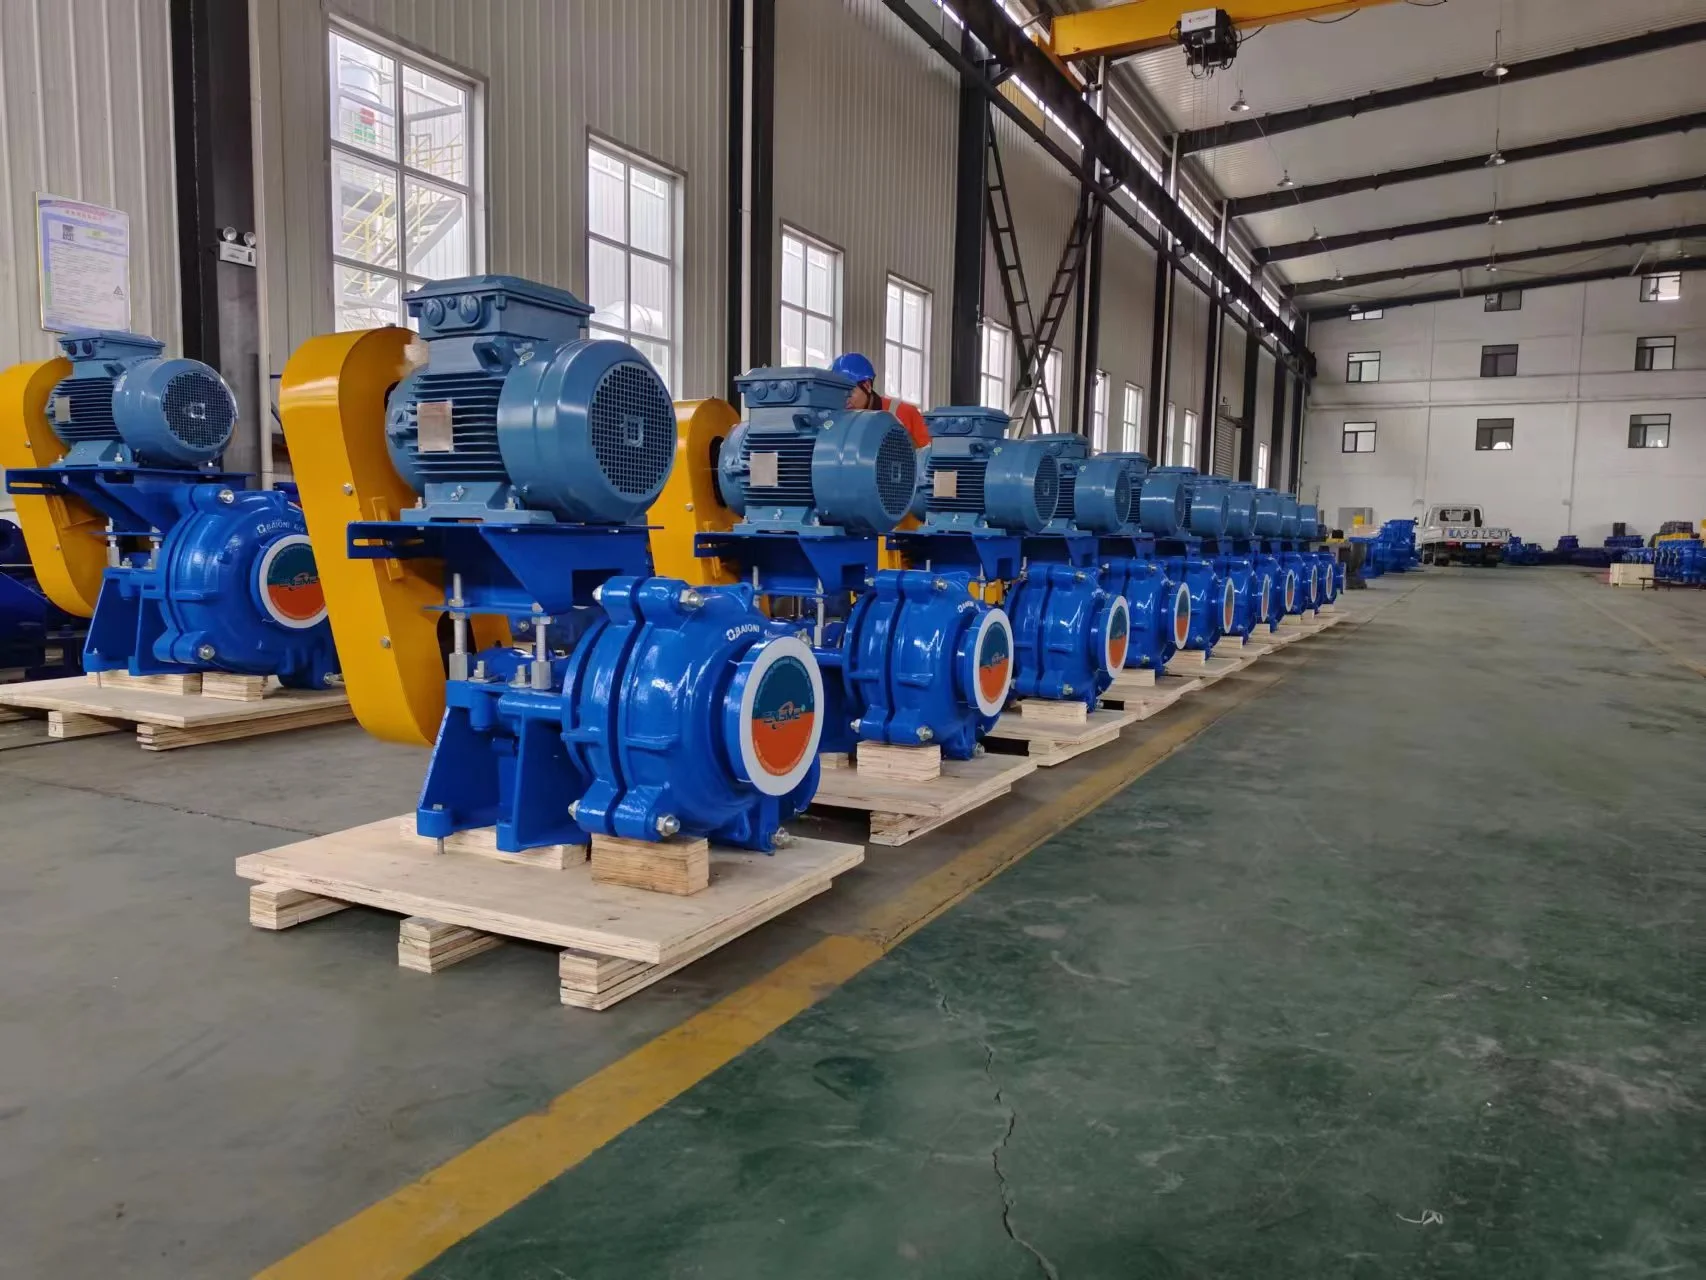
Integrating advanced engineering solutions, such as the 100PE-PCH Single Shell Slurry Pump, allows operators to move beyond simple maintenance toward systemic optimization. For those seeking a high-performance warman slurry pump replacement, focusing on high-lift capacity and corrosion resistance ensures that the system remains robust against the most challenging fluids, from hot water to corrosive chemical slurries.

Understanding the Impact of warman slurry pump replacement
Choosing the right warman slurry pump replacement is not merely about finding a part that fits; it is about enhancing the hydraulic efficiency of the entire system. The 100PE-PCH Single Shell Slurry Pump, for example, offers a head capacity of up to 140m, which provides an unmatched pumping performance. This allows operators to transfer large volumes of liquids across long distances or move fluids vertically to significant heights with ease.
By focusing on cutting-edge engineering, these replacement solutions ensure reliable operation even in the most demanding conditions. The integration of a thin oil frame further enhances performance by reducing friction, which directly translates to lower energy consumption and an extended pump lifespan, effectively maximizing productivity across the facility.
Technical Dimensions of Performance and Durability
Durability is the cornerstone of any effective warman slurry pump replacement strategy. In environments where corrosive chemicals and abrasive particles are present, the structural integrity of the pump shell and impeller determines the frequency of maintenance shutdowns. High-performance models are engineered to withstand these harsh environments, utilizing specialized materials that resist degradation.
Scalability in pumping operations requires equipment that can handle varying flow rates and pressures without losing efficiency. The high-lift capabilities of modern single-shell designs allow for greater flexibility in plant layout, as pumps can be positioned further from the discharge point while still maintaining the required pressure to keep solids in suspension.
Cost efficiency is realized through the balance of initial investment and long-term maintenance. While lower-grade replacements may seem attractive upfront, the reduction in downtime and energy savings provided by a high-efficiency thin oil frame makes premium replacements far more economical over the equipment's total lifecycle.
Material Innovation in warman slurry pump replacement
The evolution of materials has revolutionized the approach to warman slurry pump replacement. Historically, standard alloys were sufficient, but the modern demand for higher throughput and more aggressive medium handling has led to the development of specialized corrosion-resistant materials.
One of the most critical advancements in a warman slurry pump replacement is the ability to pump high-temperature mediums effortlessly. Whether handling hot water or corrosive chemical mixtures, the 100PE-PCH design ensures that extreme temperatures do not compromise the mechanical properties of the pump, eliminating the fear of heat-induced failure.
Furthermore, the synergy between abrasion resistance and corrosion resistance ensures that the pump does not easily degrade. This dual-protection approach is essential for industries where the pumped slurry contains both chemically active agents and hard mineral particles, ensuring long-term reliability.
Operational Efficiency and Energy Consumption
Energy consumption represents one of the largest operational costs in slurry transport. A strategic warman slurry pump replacement focuses on reducing internal friction and optimizing flow paths. The implementation of thin oil frames in modern designs reduces the drag on moving parts, which significantly cuts the kilowatt-hour requirement per cubic meter of slurry moved.
By optimizing the hydraulic profile of the pump, operators can achieve a higher head capacity without increasing the motor size. This efficiency not only reduces the carbon footprint of the operation but also minimizes the thermal stress on the motor and bearings, further extending the overall service life of the assembly.
Operational Performance Rating for warman slurry pump replacement
Global Industrial Applications and Use Cases
In the mining sectors of Australia and Canada, the application of a high-performance warman slurry pump replacement is critical for tailings management. The ability to handle high-density solids over long distances allows these mines to optimize their tailings storage facilities, reducing the environmental footprint and increasing safety.
Similarly, in chemical processing plants across Southeast Asia, pumps that can handle high-temperature corrosive mediums are indispensable. The use of 100PE-PCH pumps ensures that hazardous chemicals are transported efficiently without the risk of leaks or shell failure, protecting both the workforce and the surrounding environment.
Overcoming Challenges in Slurry Transport
One of the primary challenges in slurry transport is the rapid wear of the impeller and liner. When selecting a warman slurry pump replacement, engineers must analyze the particle size and velocity of the slurry. Overcoming this requires the use of specialized high-chrome or rubber-lined materials that can absorb the impact of large particles.
Another common issue is the energy loss associated with high-viscosity fluids. By utilizing pumps with optimized internal geometries and reduced friction frames, plants can overcome these fluid dynamics challenges, ensuring a steady flow and preventing the settling of solids within the pipeline, which often leads to costly blockages.
Finally, the challenge of high-temperature operation often leads to premature seal failure. Modern replacements address this by incorporating advanced sealing mechanisms and heat-resistant alloys, ensuring that the pump remains operational in extreme thermal environments without requiring frequent seal replacements.
Strategic Comparison of Pump Replacement Options
When evaluating a warman slurry pump replacement, it is essential to compare the specific technical parameters against the operational requirements. A high-lift pump like the 100PE-PCH is ideal for applications requiring a 140m head, whereas light-duty pumps are more suited for low-pressure transfers.
The decision-making process should include an analysis of the medium's temperature and chemical composition. For instance, high-temperature mediums require materials that maintain their hardness at elevated temperatures, while purely abrasive slurries benefit more from high-chrome alloys.
Ultimately, the goal of any replacement strategy is to maximize the uptime of the production line. By investing in a pump that combines durability, efficiency, and high-lift capacity, companies can ensure a stable production cycle and a significant return on investment.
Comparative Analysis of warman slurry pump replacement Technical Specifications
| Pump Model/Type |
Max Head Capacity |
Wear Resistance |
Thermal Stability |
| 100PE-PCH Single Shell |
140m |
Excellent (High Chrome) |
High-Temperature Ready |
| Standard Rubber Lined |
60m |
Good (Soft Abrasion) |
Moderate |
| ZGB Heavy Duty |
100m |
Superior (Hard Rock) |
Moderate |
| SL(R) Light Duty |
40m |
Fair |
Low |
| Stainless Steel Option |
80m |
Moderate |
Excellent (Corrosion) |
| SH Hard Metal |
120m |
Extreme |
Moderate |
FAQS
For high-temperature applications, you should prioritize pumps like the 100PE-PCH, which are specifically engineered to handle heat without compromising material strength. Ensure the replacement specifies heat-resistant alloys and advanced seal materials to prevent thermal degradation and leakage, as standard rubber linings may fail at elevated temperatures.
Yes, by selecting a warman slurry pump replacement with optimized hydraulic efficiency and features like a thin oil frame, you can reduce internal friction. This allows the pump to achieve the required head capacity with less power consumption, leading to lower electricity bills and reduced wear on the drive motor.
A single shell design, such as that found in the 100PE-PCH, simplifies the pump structure, reducing the number of potential leak points and making maintenance more straightforward. It often provides a more robust casing that can better handle the pressures associated with high-lift pumping operations.
The frequency depends on the abrasiveness of the slurry. However, monitoring the flow rate and pump head is key. A drop in performance usually indicates wear. Using high-chrome materials can extend the replacement interval, but regular inspections every 3-6 months are recommended for high-wear environments.
Absolutely. In most cases, a warman slurry pump replacement involves replacing the wear parts (impeller and liner). However, if the pump casing is severely eroded or if you need to upgrade to a higher head capacity (like 140m), replacing the entire pump unit is the more sustainable long-term solution.
The thin oil frame reduces the friction between moving components and optimizes lubrication. This prevents overheating and reduces the mechanical stress on the bearings and shaft, which significantly extends the operational life of the pump and reduces the need for frequent emergency repairs.
Conclusion
Investing in a high-quality warman slurry pump replacement is a critical decision that impacts the efficiency, durability, and profitability of industrial slurry transport. By prioritizing advanced engineering features—such as the 140m head capacity, thin oil frames for energy efficiency, and materials capable of withstanding high temperatures and corrosive environments—operators can transform a maintenance burden into a competitive advantage. The 100PE-PCH Single Shell Slurry Pump exemplifies this shift, offering a robust solution that maximizes uptime and minimizes operational costs.
Looking forward, the integration of more resilient materials and energy-efficient designs will continue to redefine the standards of slurry transport. We recommend that plant managers conduct a comprehensive audit of their current pumping systems to identify bottlenecks where a high-performance replacement could yield the highest ROI. For those ready to elevate their operations and ensure long-term reliability, we invite you to explore our specialized range of slurry solutions. Visit our website: www.qualityslurrypump.com