The transportation of abrasive materials in industrial environments requires specialized equipment capable of overcoming significant resistance and elevation. A high head slurry pump is engineered specifically for these demanding conditions, ensuring that thick, abrasive fluids can be moved efficiently over long distances or to elevated discharge points without compromising system integrity.
In global mining and mineral processing, the ability to maintain high pressure per stage is critical for operational throughput. By utilizing advanced metallurgy and hydraulic design, these pumps minimize the need for excessive booster stations, thereby reducing both the initial capital expenditure and the long-term energy costs associated with slurry transport.
Understanding the technical specifications of a high head slurry pump, such as the SBH/50D model, allows engineers to optimize flow rates and head pressures for specific applications in coal washing or metallurgy.

Engineering Design of the High Head Slurry Pump
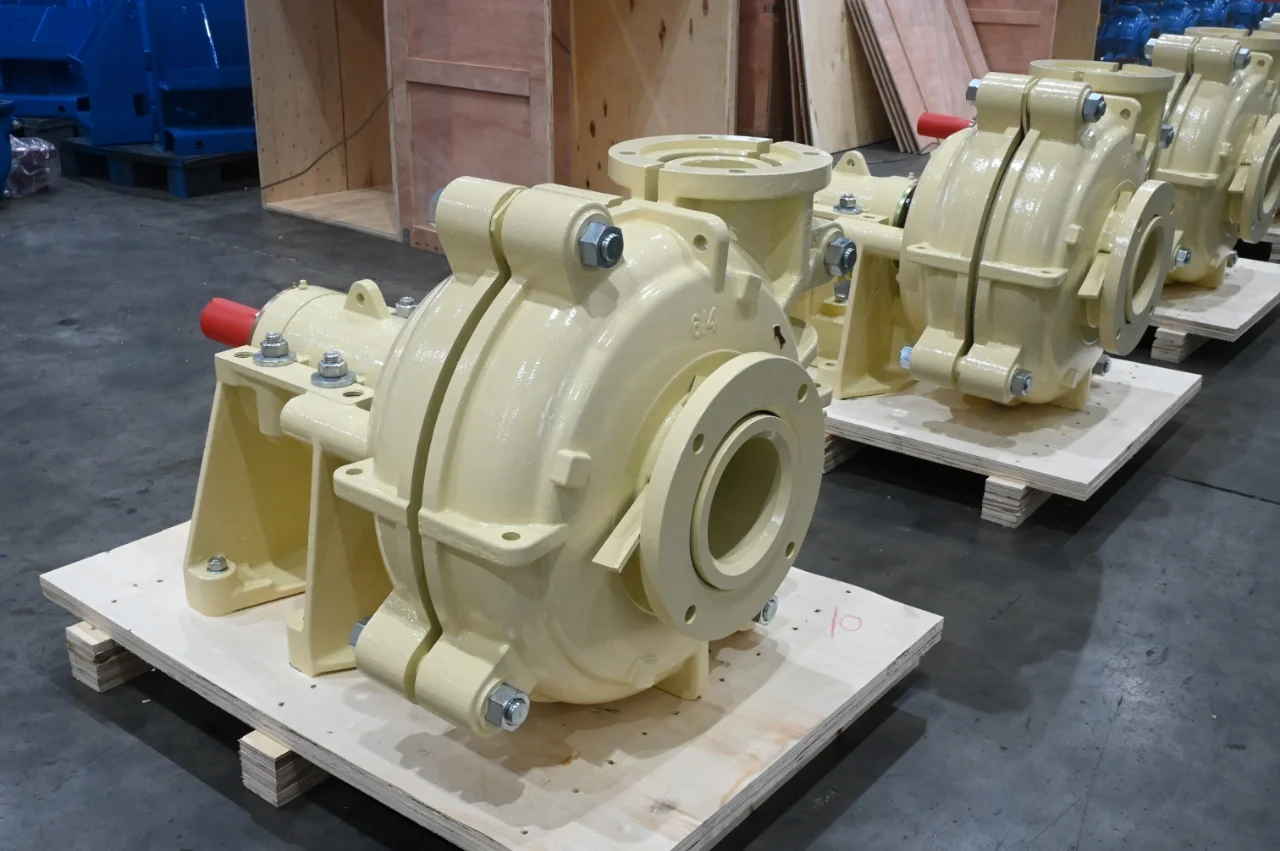
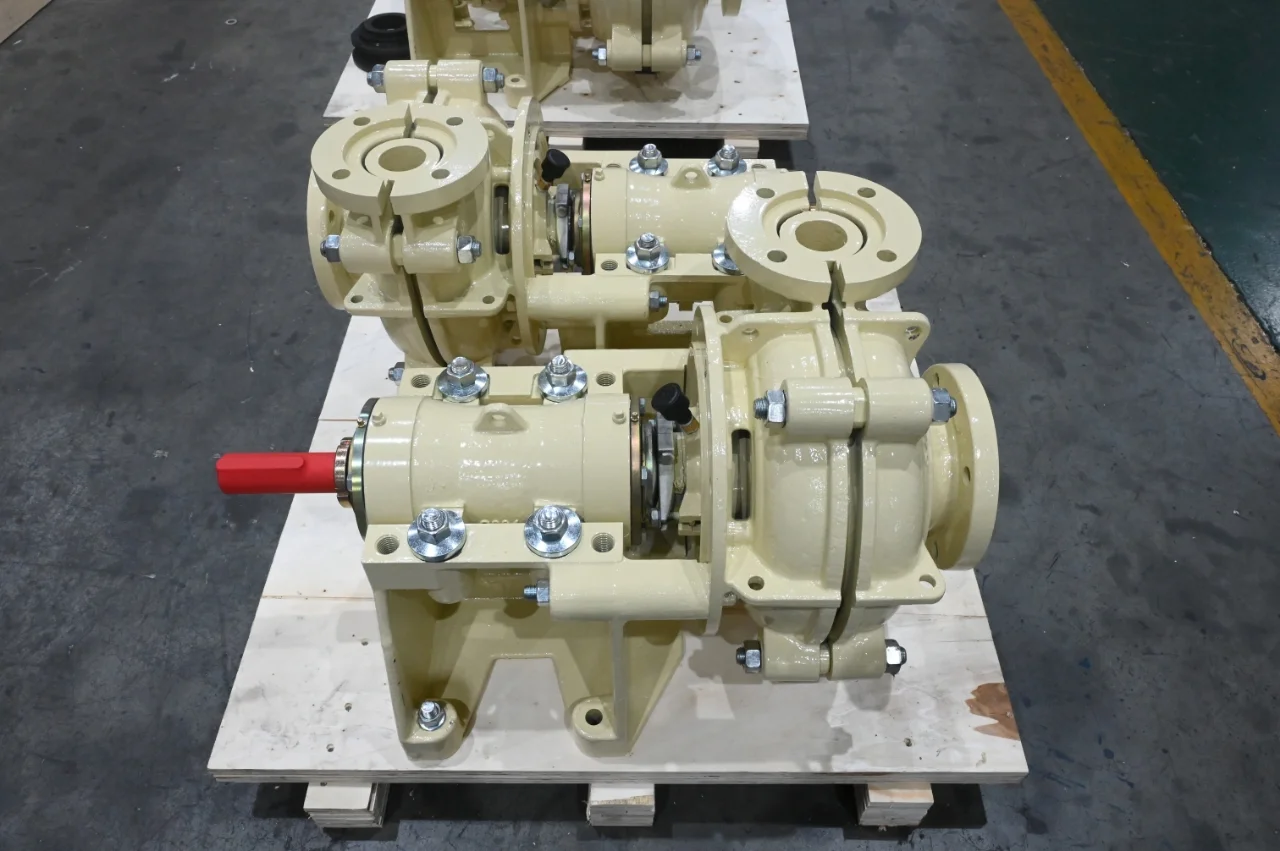
The SBH/50D, also known as the 3/2D-HH, represents a sophisticated approach to high-pressure fluid dynamics. Designed as a 2” discharge high head slurry pump, its primary architectural goal is to deliver high head per stage. This capability is essential for applications where slurry must be transported over vast distances or where the system requires multiple pumps arranged in series to achieve the necessary discharge pressure.
From a mechanical perspective, the integration of a 5-vane closed type impeller with a vane diameter of 457mm ensures a powerful kinetic energy transfer to the fluid. This design minimizes turbulence and maximizes the pressure lift, making it an ideal choice for heavy-duty industrial environments where reliability is non-negotiable.
Material Construction for Extreme Abrasion
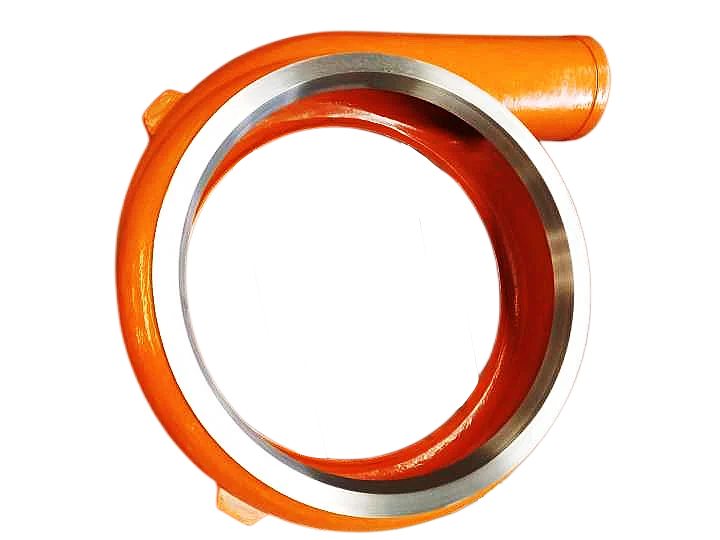
The longevity of a high head slurry pump is dictated by its resistance to wear. For the SBH series, the wet-end spare parts—including the impeller, volute liner, front liner, and back liner—are constructed from high chrome alloy. This material, similar to ASTM A532, is a specialized white iron that provides exceptional resistance to both abrasion and erosion, ensuring the pump maintains its hydraulic efficiency even when handling harsh mineral slurries.
Versatility in construction is further provided through alternative material options for the casing and shaft. While grey iron is standard for outer casings, ductile iron is available for higher structural strength. Similarly, shafts can be upgraded from carbon steel to SS304 or SS316 to prevent corrosion in chemically aggressive environments.
To protect the most vulnerable points of the pump, the shaft sleeve is available in SS304, SS316, Ceramic, or Tungsten Carbide. These high-hardness materials prevent the shaft from wearing down due to particle leakage, while the choice between expeller seals, gland packing, or mechanical seals allows users to tailor the pump to their specific leak-tolerance and maintenance requirements.
Core Operational Parameters and Efficiency
Operating a high head slurry pump requires a precise balance between flow rate and discharge head. The SBH/50D is designed to handle a flow rate ranging from 68.4 to 136.8 m3/hr, providing a substantial volume of movement while maintaining a head between 25 and 87 meters.
To achieve these performance metrics, the pump operates at speeds between 850 and 1400 rpm. A critical specification for handlers is the maximum passage size of 31mm, which determines the maximum particle size the high head slurry pump can transport without clogging the impeller.
With a maximum efficiency of 47%, the pump is optimized for the dense and viscous nature of slurry. While this may seem lower than clear-water pumps, it is highly competitive for high-pressure slurry applications, ensuring that energy is effectively converted into the pressure needed for long-distance transport.
Global Industrial Applications of High Head Systems
The utility of a high head slurry pump extends across several critical global industries. In mineral processing and metallurgy, these pumps are indispensable for moving tailings and concentrates through processing plants. The ability to handle high-pressure discharge allows these facilities to optimize their layout, moving materials across different elevation levels without requiring numerous intermediate pump stations.
Beyond mining, the SBH series is widely utilized in flue gas desulphurization (FGD) and coal washing. In FGD systems, the pump handles abrasive gypsum slurries, where the high chrome alloy construction prevents premature wear. In coal washing, the ability to move abrasive coal particles at high pressure ensures efficient cleaning and separation processes.
Performance Suitability of High Head Slurry Pump Models
Long-Term Value and Maintenance Reliability
The long-term value of investing in a high-quality high head slurry pump lies in the reduction of unplanned downtime. By utilizing high chrome alloy and providing options for tungsten carbide shaft sleeves, the SBH series significantly extends the Mean Time Between Failures (MTBF). This reliability is critical in 24/7 operations where a single pump failure can halt an entire production line.
Furthermore, the use of standardized bearing assemblies, such as the DAM005M, and compatible brands like SKF, Timken, and NSK, ensures that maintenance teams can source replacement parts quickly. The modular design of the wet-end liners allows for rapid replacement without needing to dismantle the entire pump housing, thereby reducing labor costs and increasing overall plant availability.
Future Innovations in Slurry Transport Technology
As the industry moves toward "Industry 4.0," the integration of smart monitoring into the high head slurry pump ecosystem is becoming a priority. Real-time vibration analysis and wear-sensing liners are being developed to predict failure before it occurs. This shift from reactive to predictive maintenance will further optimize the operational costs of high-pressure slurry systems.
Sustainability is also driving innovation in impeller geometry. Computational Fluid Dynamics (CFD) is being used to refine the vane angles of the SBH series to increase the maximum efficiency beyond 47%, reducing the carbon footprint of the energy-intensive process of moving high-density solids.
Moreover, the development of new nano-composite materials for liners promises even greater abrasion resistance than traditional high chrome alloys. These advancements will allow pumps to handle even more aggressive slurries at higher pressures, expanding the possibilities for deep-mine drainage and ultra-long-distance tailings transport.
Challenges and Technical Solutions in Pumping
One of the primary challenges when operating a high head slurry pump is the phenomenon of slurry settling. If the flow velocity drops below a critical threshold, solids can precipitate, leading to pipe blockages. The solution lies in the careful calculation of the critical velocity and the selection of a pump with sufficient head to maintain turbulent flow throughout the pipeline.
Another common issue is the rapid wear of the shaft seal. In the SBH series, this is addressed by offering expeller seals, which utilize centrifugal force to move the slurry away from the seal area, drastically reducing the wear on the packing or mechanical seal. This technical solution ensures that the pump can operate under high pressure without leaking hazardous slurry into the environment.
Finally, cavitation can occur if the Net Positive Suction Head (NPSH) is insufficient. By optimizing the suction intake and ensuring the pump is installed at the correct elevation relative to the slurry source, operators can prevent the formation of vapor bubbles that would otherwise pit the impeller and reduce the efficiency of the high head system.
Technical Analysis of SBH/50D High Head Slurry Pump Components
| Component |
Standard Material |
Alternative Material |
Performance Impact |
| Impeller |
A05A33 |
A49 High Chrome |
Increased Abrasion Resistance |
| Outer Casing |
Grey Iron |
Ductile Iron |
Higher Structural Integrity |
| Shaft |
Carbon Steel |
SS316 Stainless |
Corrosion Protection |
| Shaft Sleeve |
SS304 |
Tungsten Carbide |
Maximum Wear Resistance |
| Shaft Seal |
Expeller Seal |
Mechanical Seal |
Leakage Control |
| Bearings |
ZWZ |
SKF / Timken |
Enhanced Load Capacity |
FAQS
The SBH/50D is classified as a high head slurry pump because it is specifically engineered to generate significant pressure per stage, with a maximum head reaching 87 meters. This allows it to move abrasive materials over longer distances or higher elevations compared to standard slurry pumps, reducing the need for multiple booster stations in a pipeline.
The SBH/50D has a maximum passage size of 31mm. While it can technically handle particles up to this size, it is recommended to ensure that the majority of the solids in the slurry are well below this limit to maintain maximum efficiency (47%) and prevent potential clogging or accelerated wear on the 5-vane closed impeller.
For environments where corrosion is a primary concern alongside abrasion, we recommend SS316 or Ceramic sleeves. However, for the most extreme abrasive conditions, Tungsten Carbide is the superior choice due to its immense hardness, which prevents the shaft from scoring and extends the life of the seals.
Yes, it is highly suitable. The use of high chrome alloy (similar to ASTM A532) for the wet-end parts ensures that the pump can withstand the erosive nature of gypsum slurries typically found in FGD applications, while the high head capability ensures the slurry is moved effectively through the system.
An expeller seal uses a specialized impeller design to create a centrifugal force that pushes the slurry away from the shaft area, reducing the pressure at the seal. A mechanical seal provides a tighter, more positive closure. Expeller seals are often preferred in high-head slurry applications to reduce wear and maintenance on the sealing components.
The SBH/50D is designed for a flow rate range of 68.4 to 136.8 m3/hr. The exact flow rate will depend on the operating speed (850-1400rpm) and the total dynamic head of the system, allowing it to be flexible for various industrial requirements.
Conclusion
The SBH/50D high head slurry pump is a critical asset for industries requiring the efficient transport of abrasive materials under high-pressure conditions. By combining high chrome alloy metallurgy with a high-head hydraulic design, it successfully addresses the dual challenges of material erosion and energy efficiency in long-distance slurry transport.
Looking forward, the integration of smart monitoring and the adoption of advanced nano-materials will continue to push the boundaries of what these pumps can achieve. For operators seeking to maximize uptime and reduce operational costs, selecting a pump with a proven track record in mineral processing and metallurgy is the most strategic path toward industrial sustainability. Visit our website: www.qualityslurrypump.com