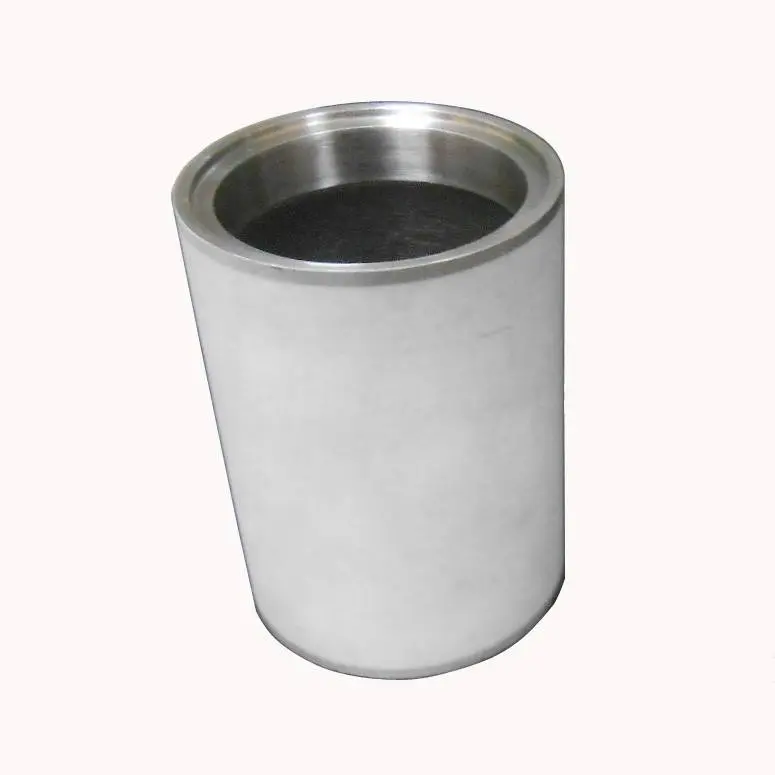
Ceramic Coated (J04, J05) Shaft Sleeve; Optional: Tungsten Carbide (J32) Shaft Sleeve
Oct 31,25
How to select the appropriate slurry pump model parameters
May 11,26
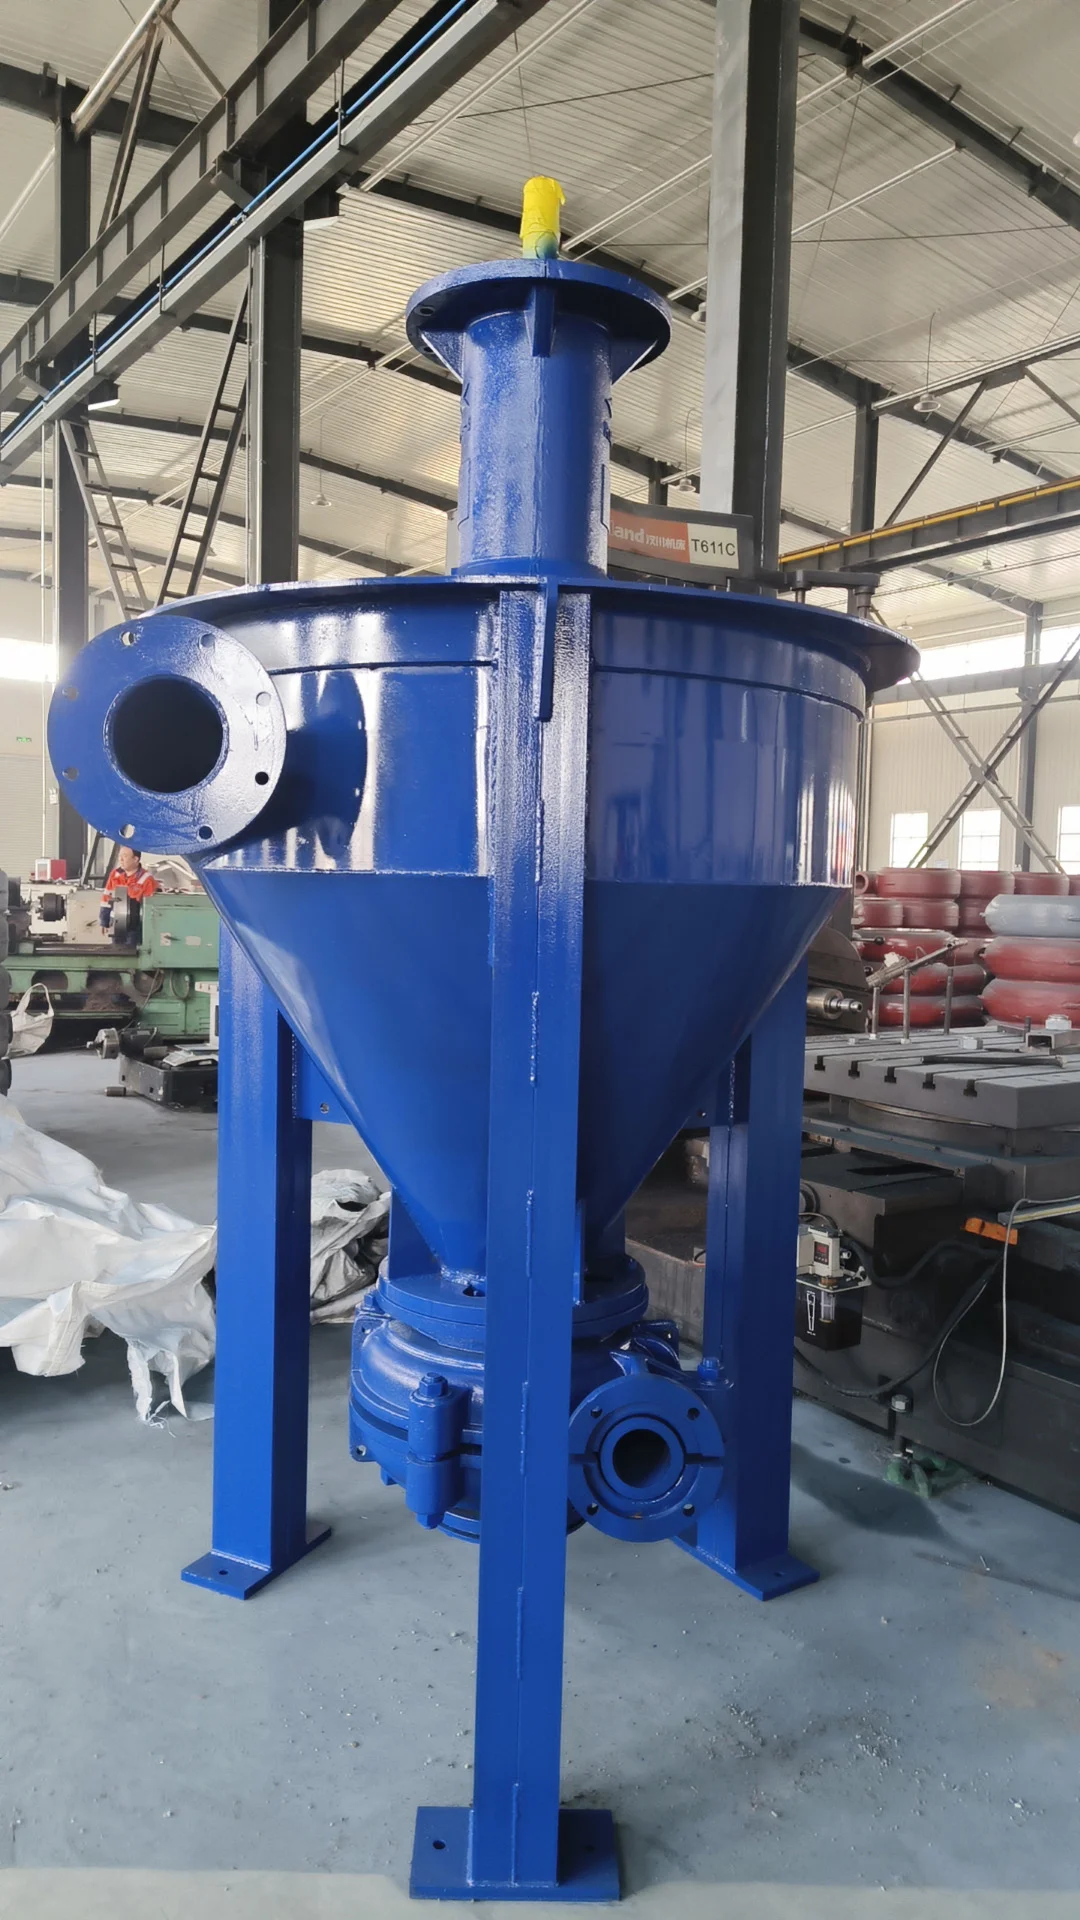
High Efficiency Froth Slurry Pump for Mineral Processing
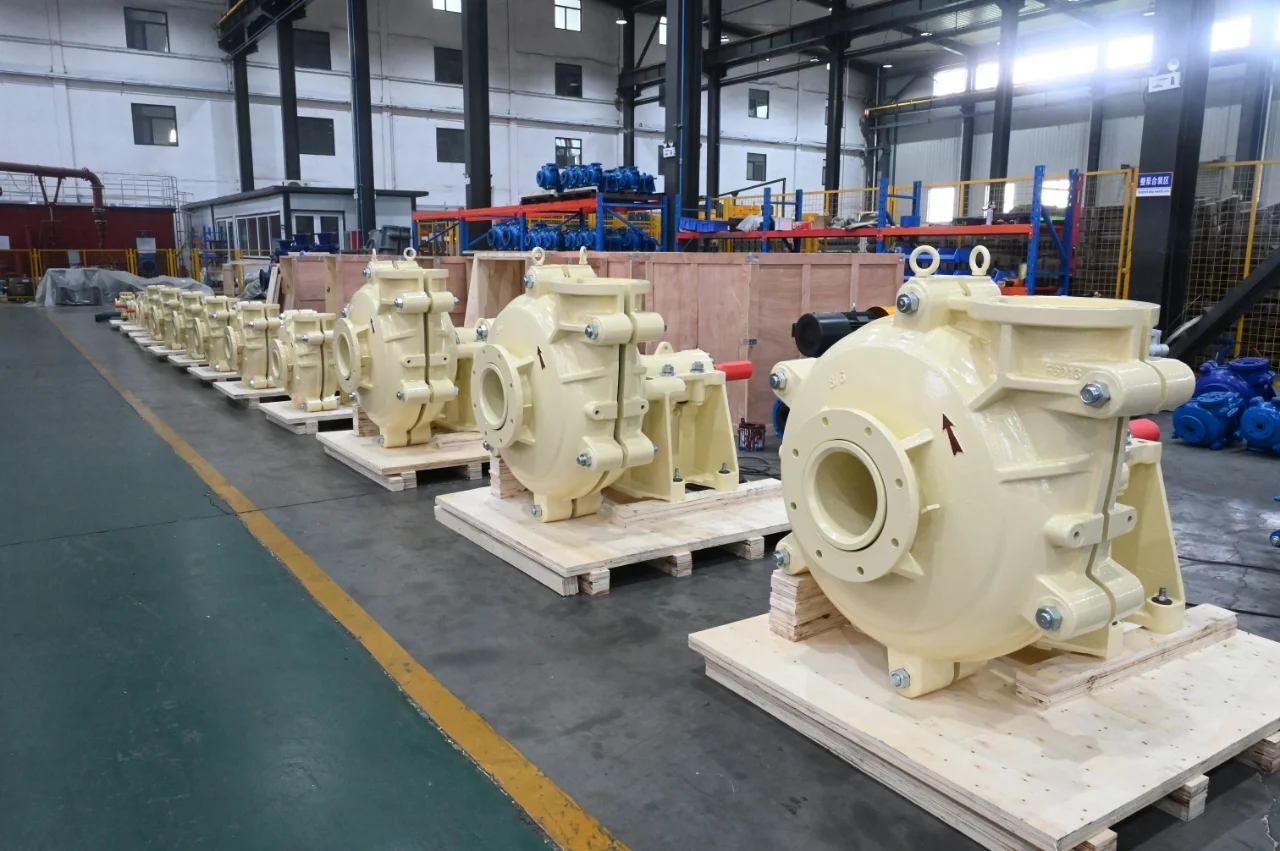
In the demanding world of mineral processing and chemical manufacturing, the movement of air-entrained liquids presents a unique engineering challenge. A froth slurry pump is specifically designed to handle these volatile mixtures, ensuring that the valuable froth layer often containing concentrated minerals is transported efficiently without collapsing or losing its structural integrity. The global demand for high-efficiency mineral recovery has pushed the evolution of pumping technology toward specialized designs that can withstand extreme abrasion while managing gas-liquid interfaces. Without a dedicated froth slurry pump, industrial operations often face severe cavitation, inconsistent flow rates, and premature equipment failure, leading to significant downtime
Feb 26,26
Comprehensive Guide to OEM Slurry Pump Volute Liner Supplier Selection
Finding a reliable OEM slurry pump volute liner supplier is critical for maintaining the efficiency and longevity of your slurry pumping systems.
Dec 05,25
Vietnam Client Visit Update | On-Site Discussion for Vertical Slurry Pump Project Optimization
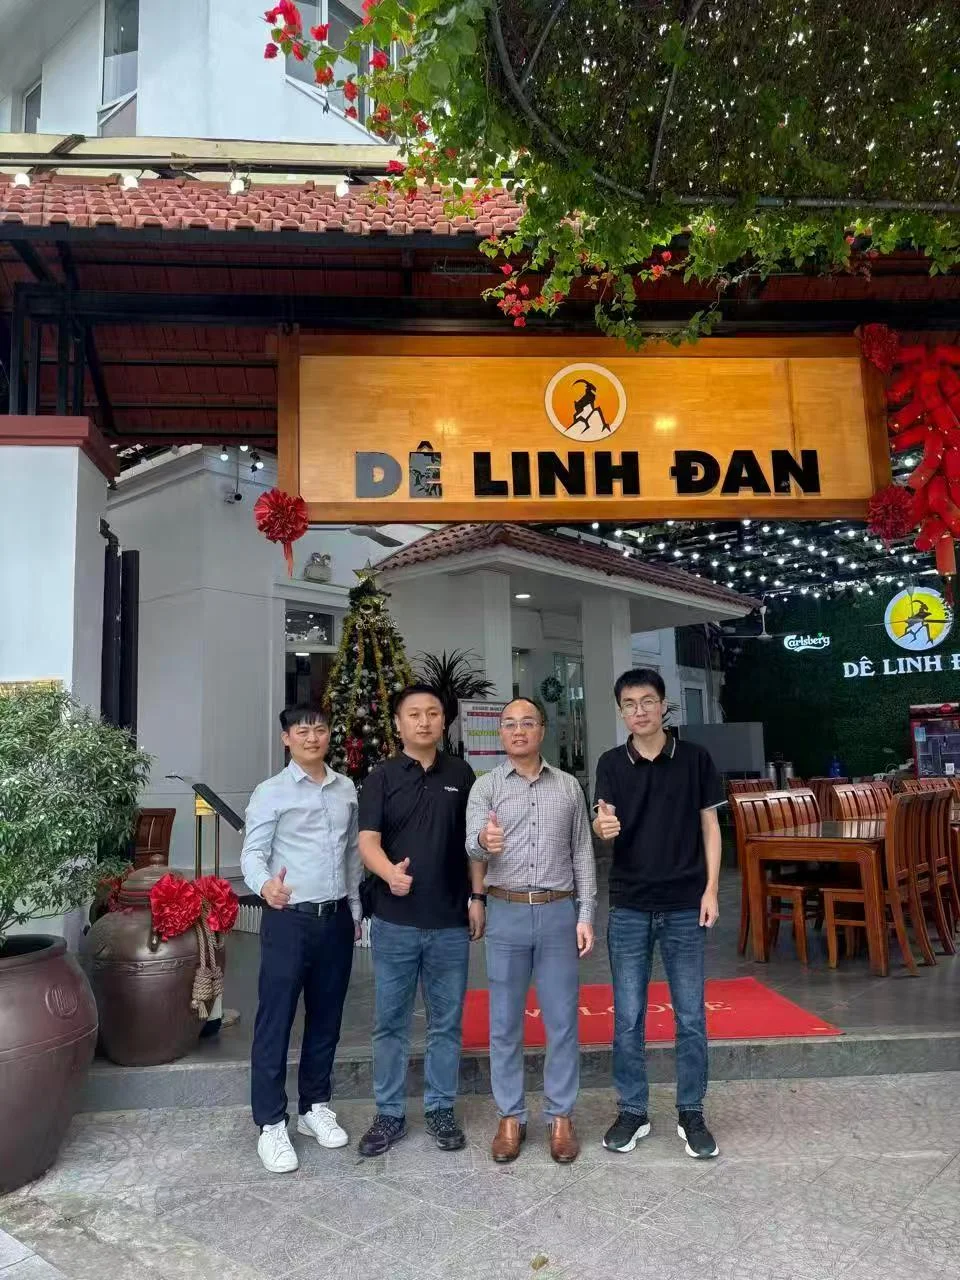
On November 30, 2025, our technical and service team began a 10-day business visit to Vietnam, meeting mining clients face to face to review the operation of vertical sump pumps and discuss technical optimization for upcoming projects.
Feb 13,26
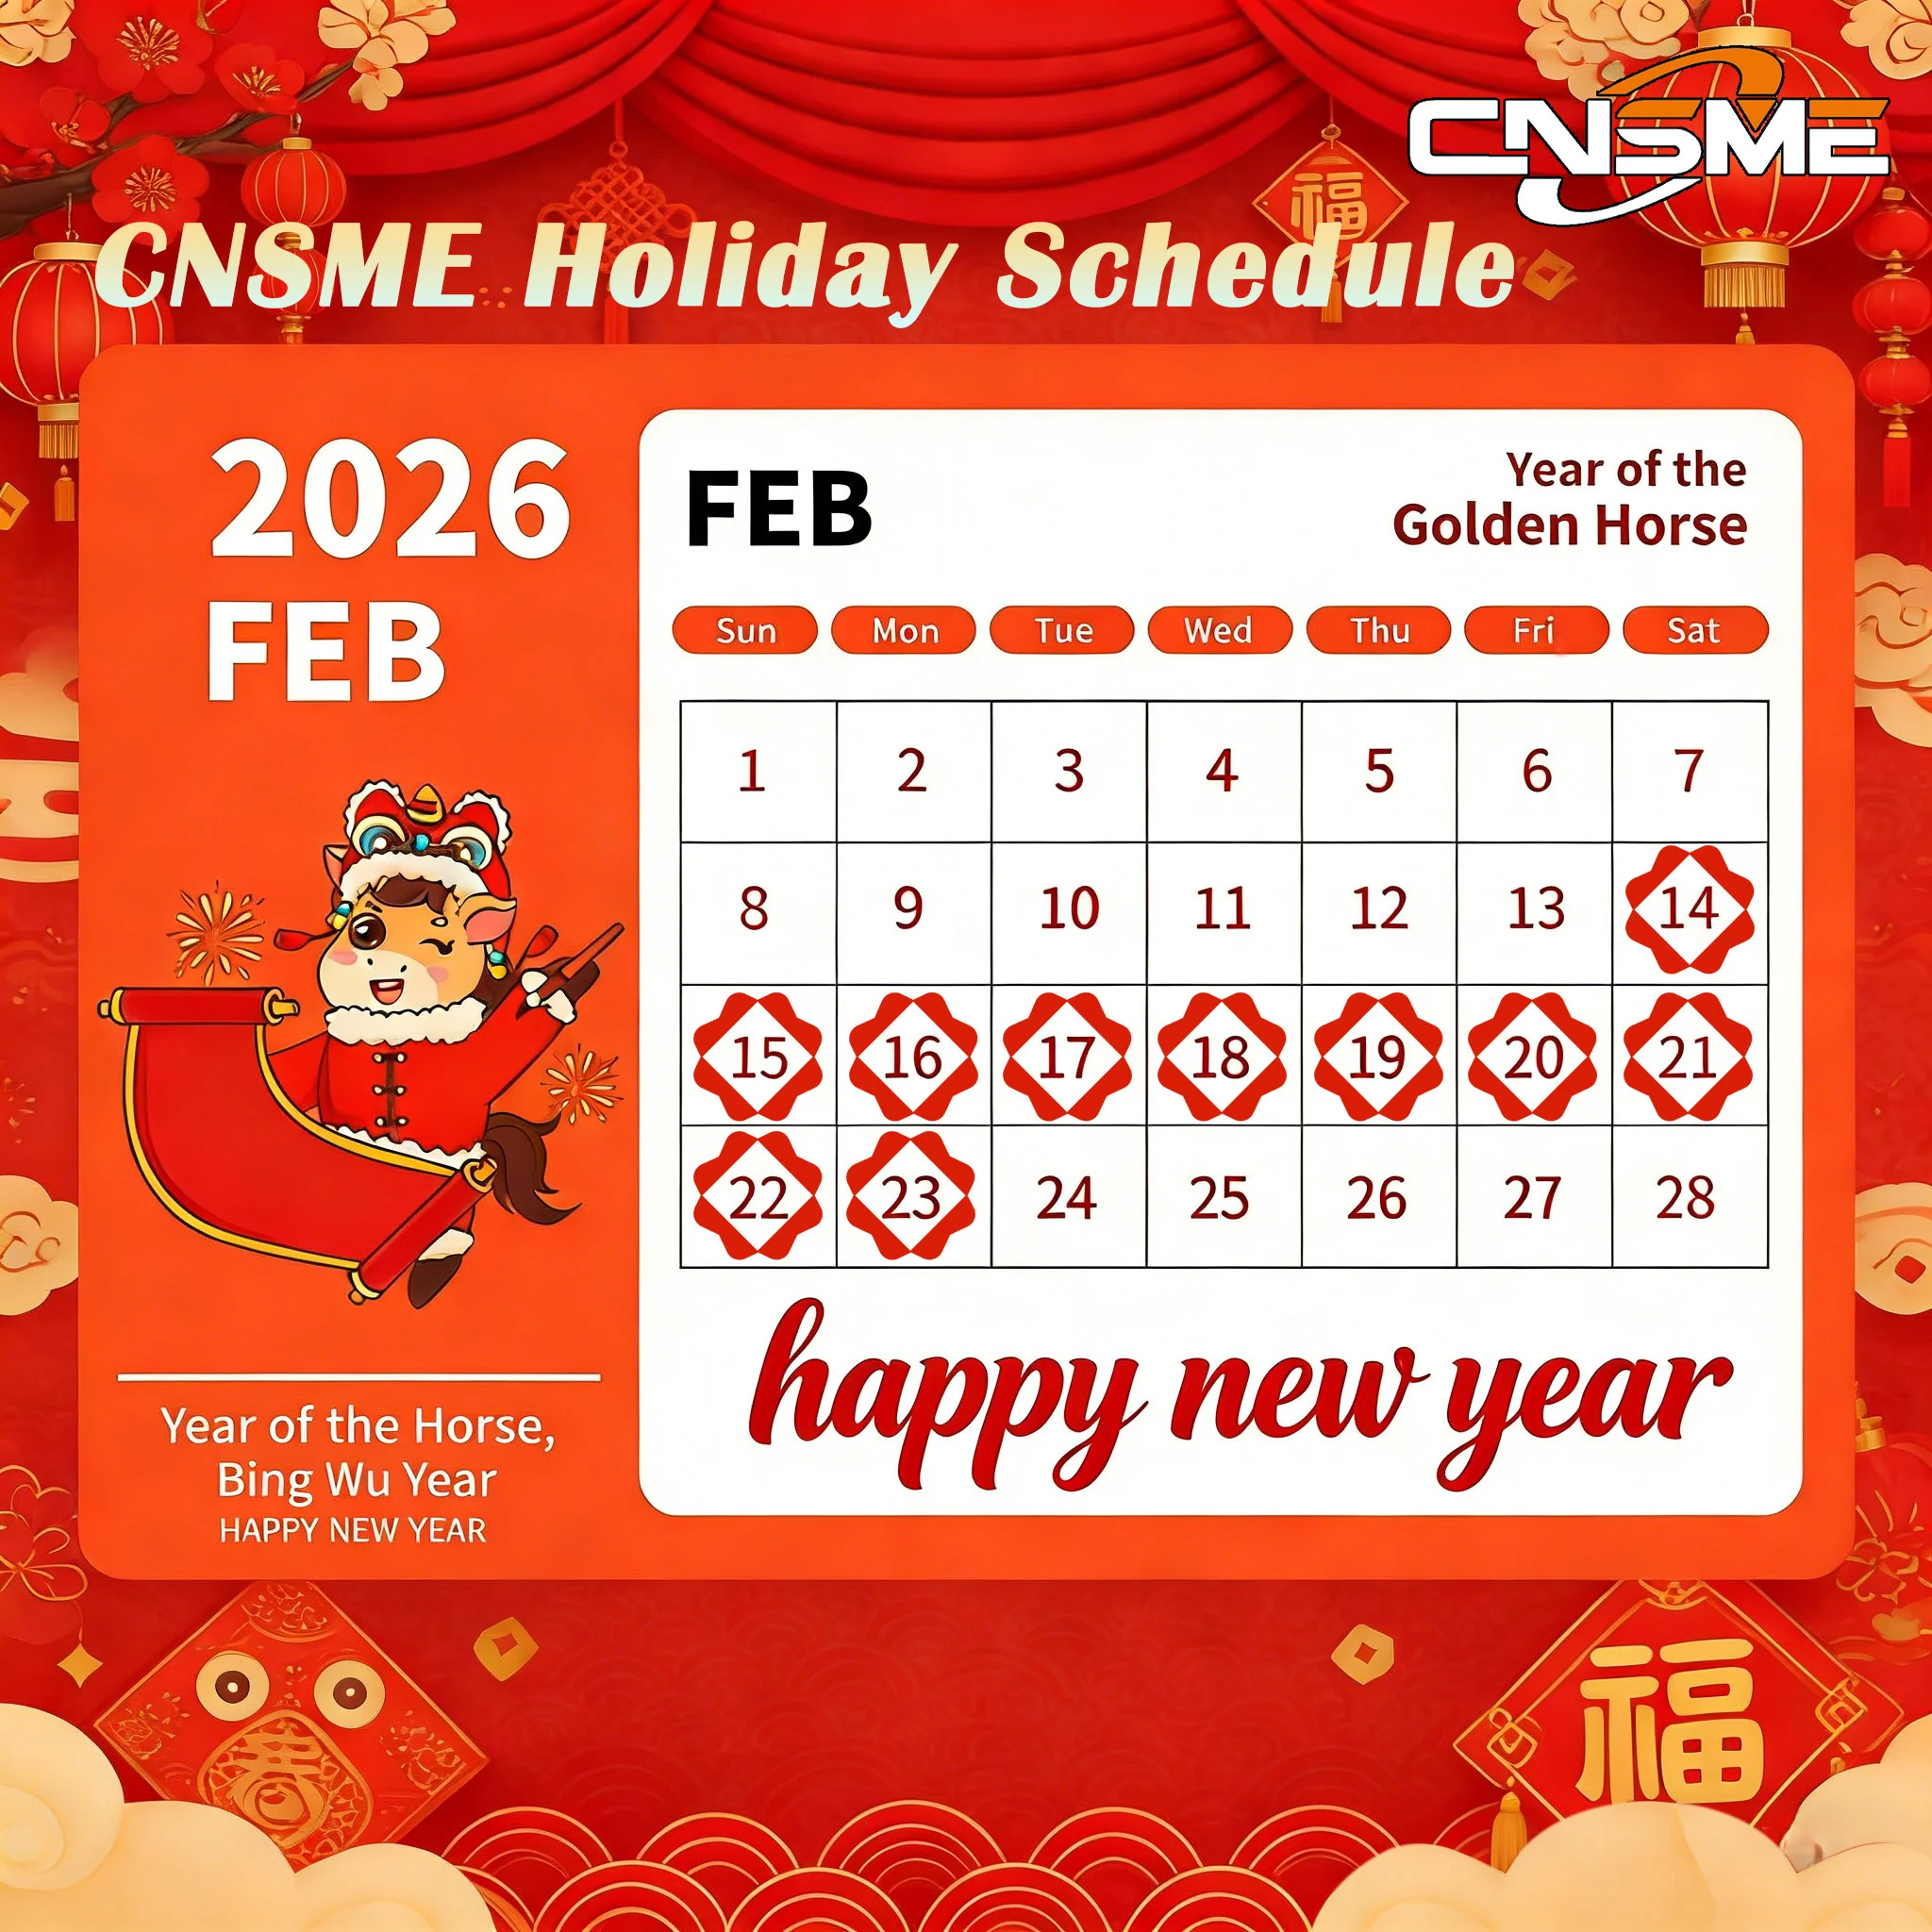
CNSME 2026 Chinese New Year Holiday Notice – Year of the Horse
As the 2026 Chinese New Year approaches, CNSME would like to extend our sincere greetings and best wishes to our global customers, partners, and team members. In celebration of the Year of the Horse, please find below our official holiday schedule and service arrangements to help you plan your business in advance.
Oct 31,25
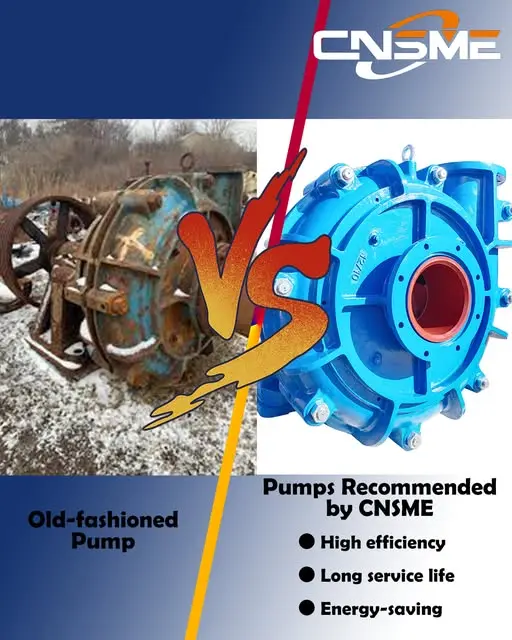
-40℃ Ultimate Challenge? CNSME Recommends AH/AHR Heavy Duty Slurry Pump!
bscribe newslette