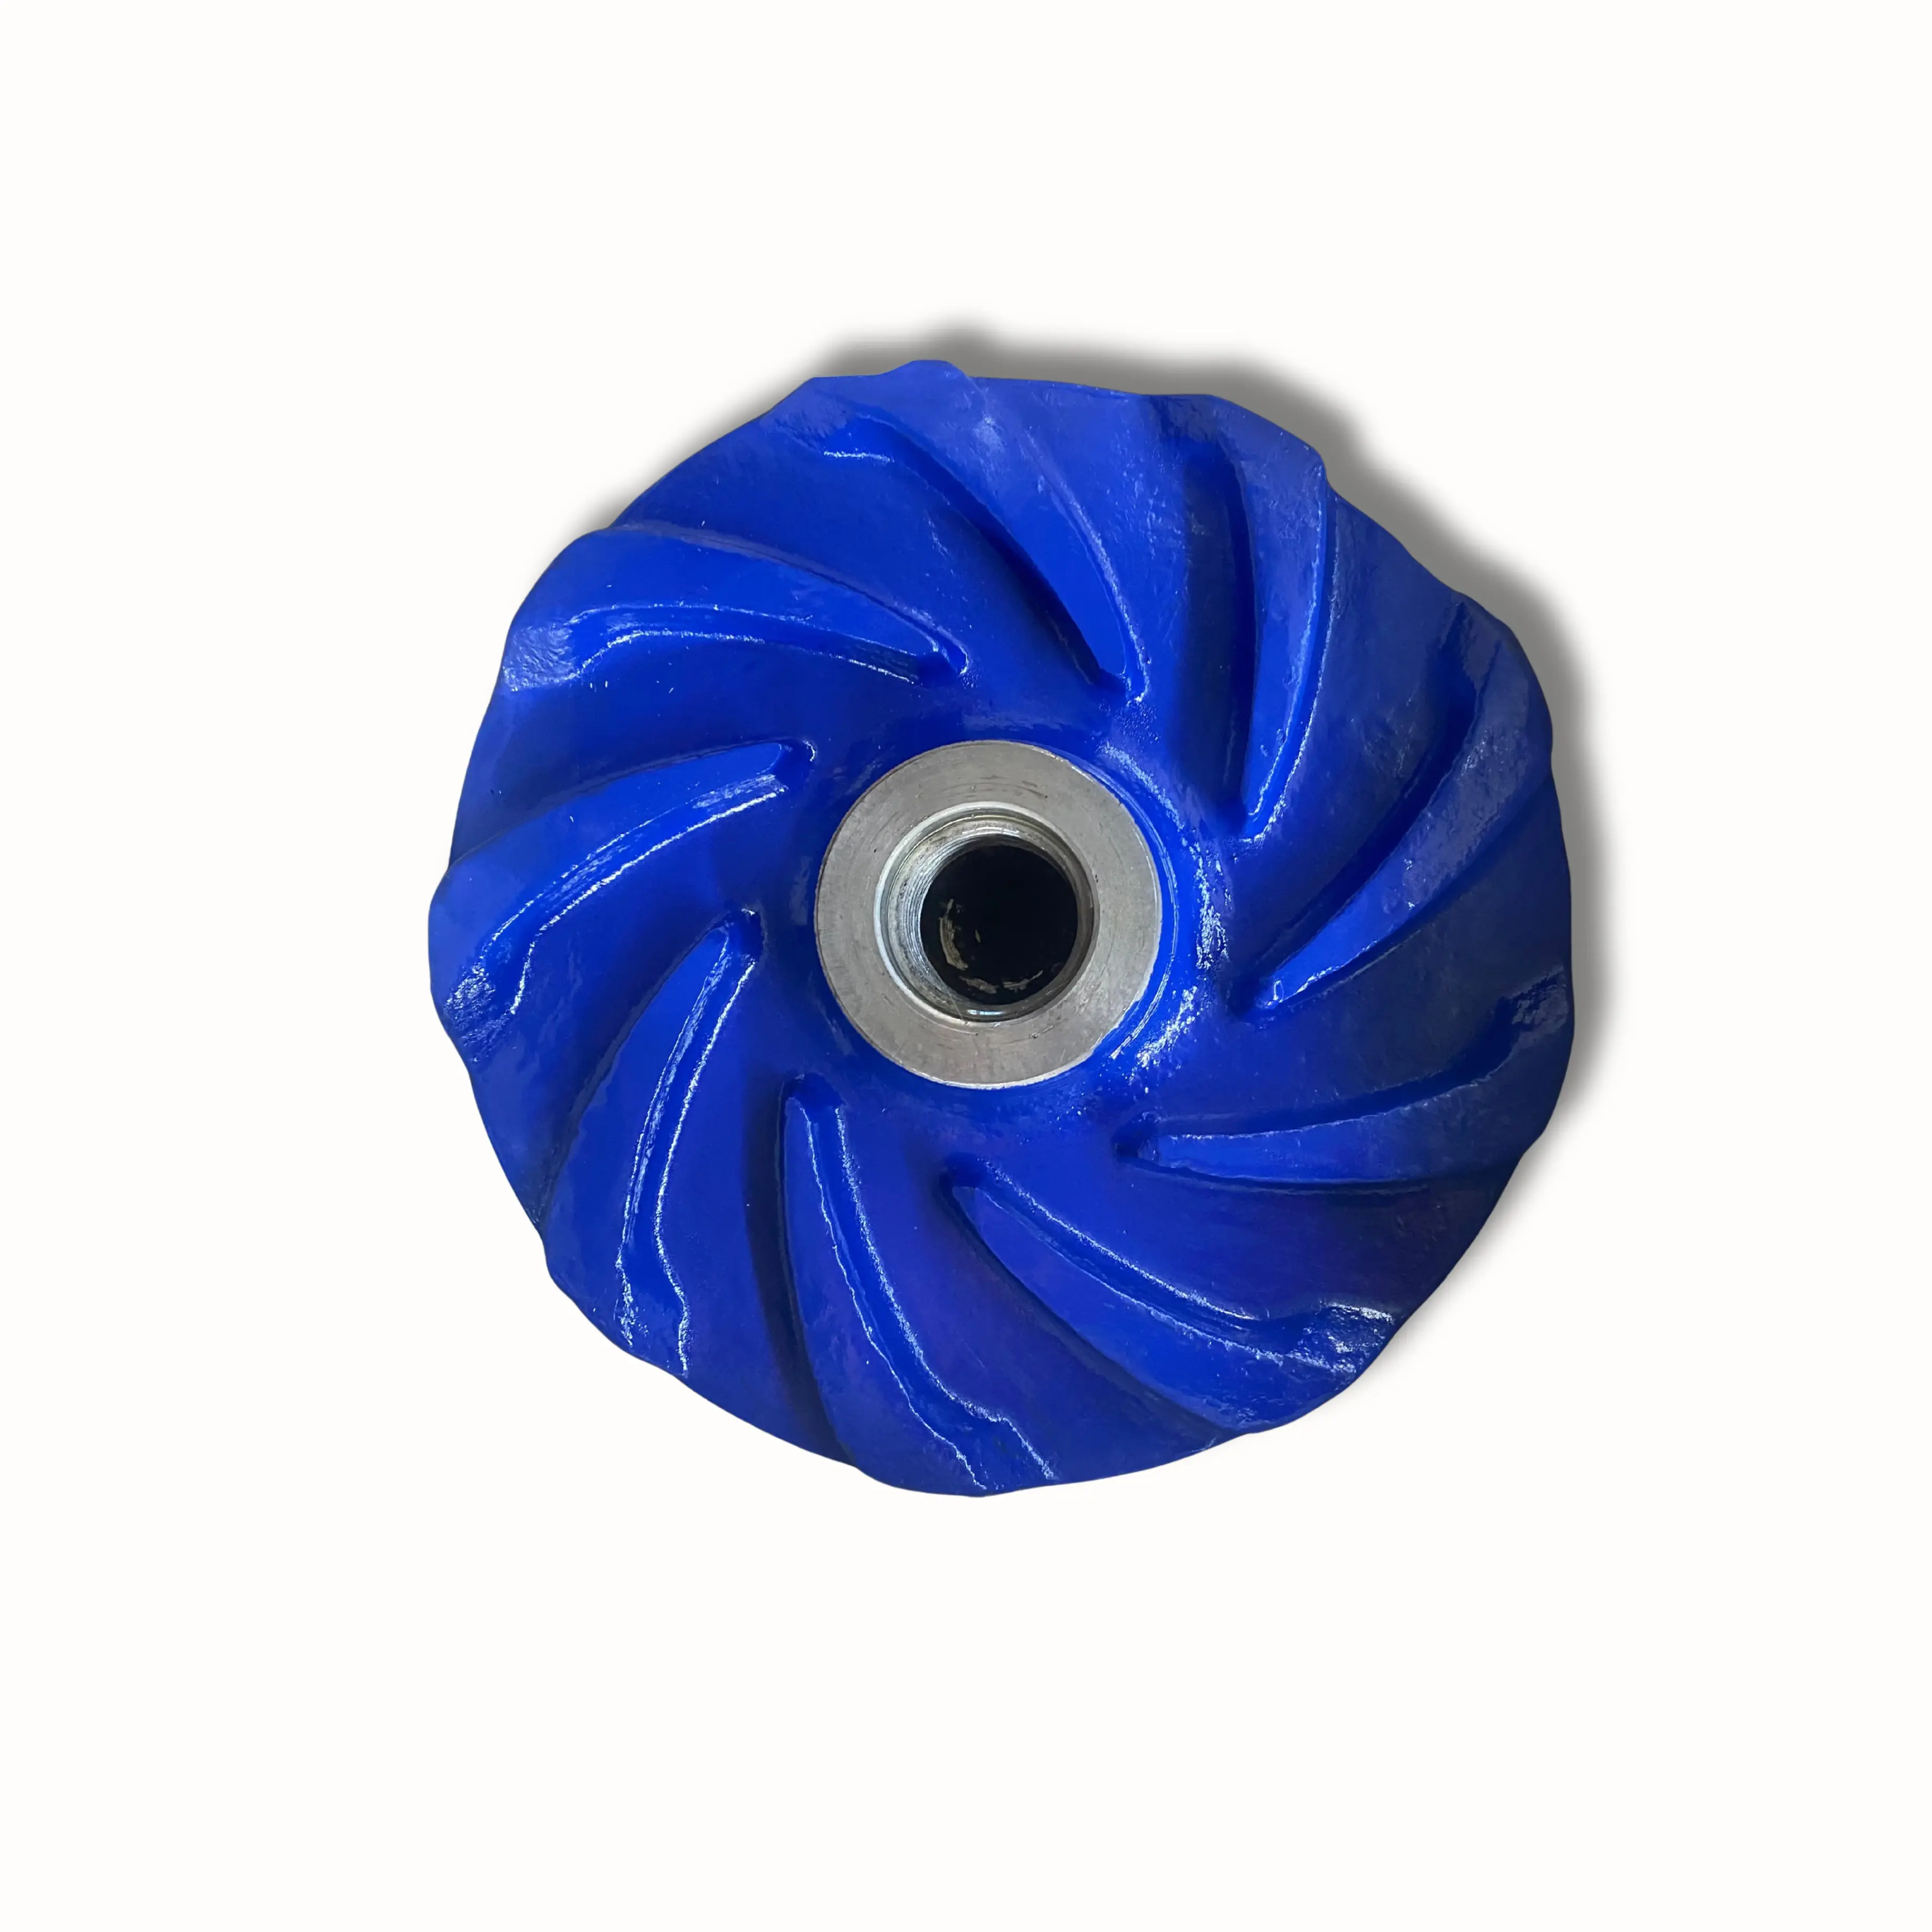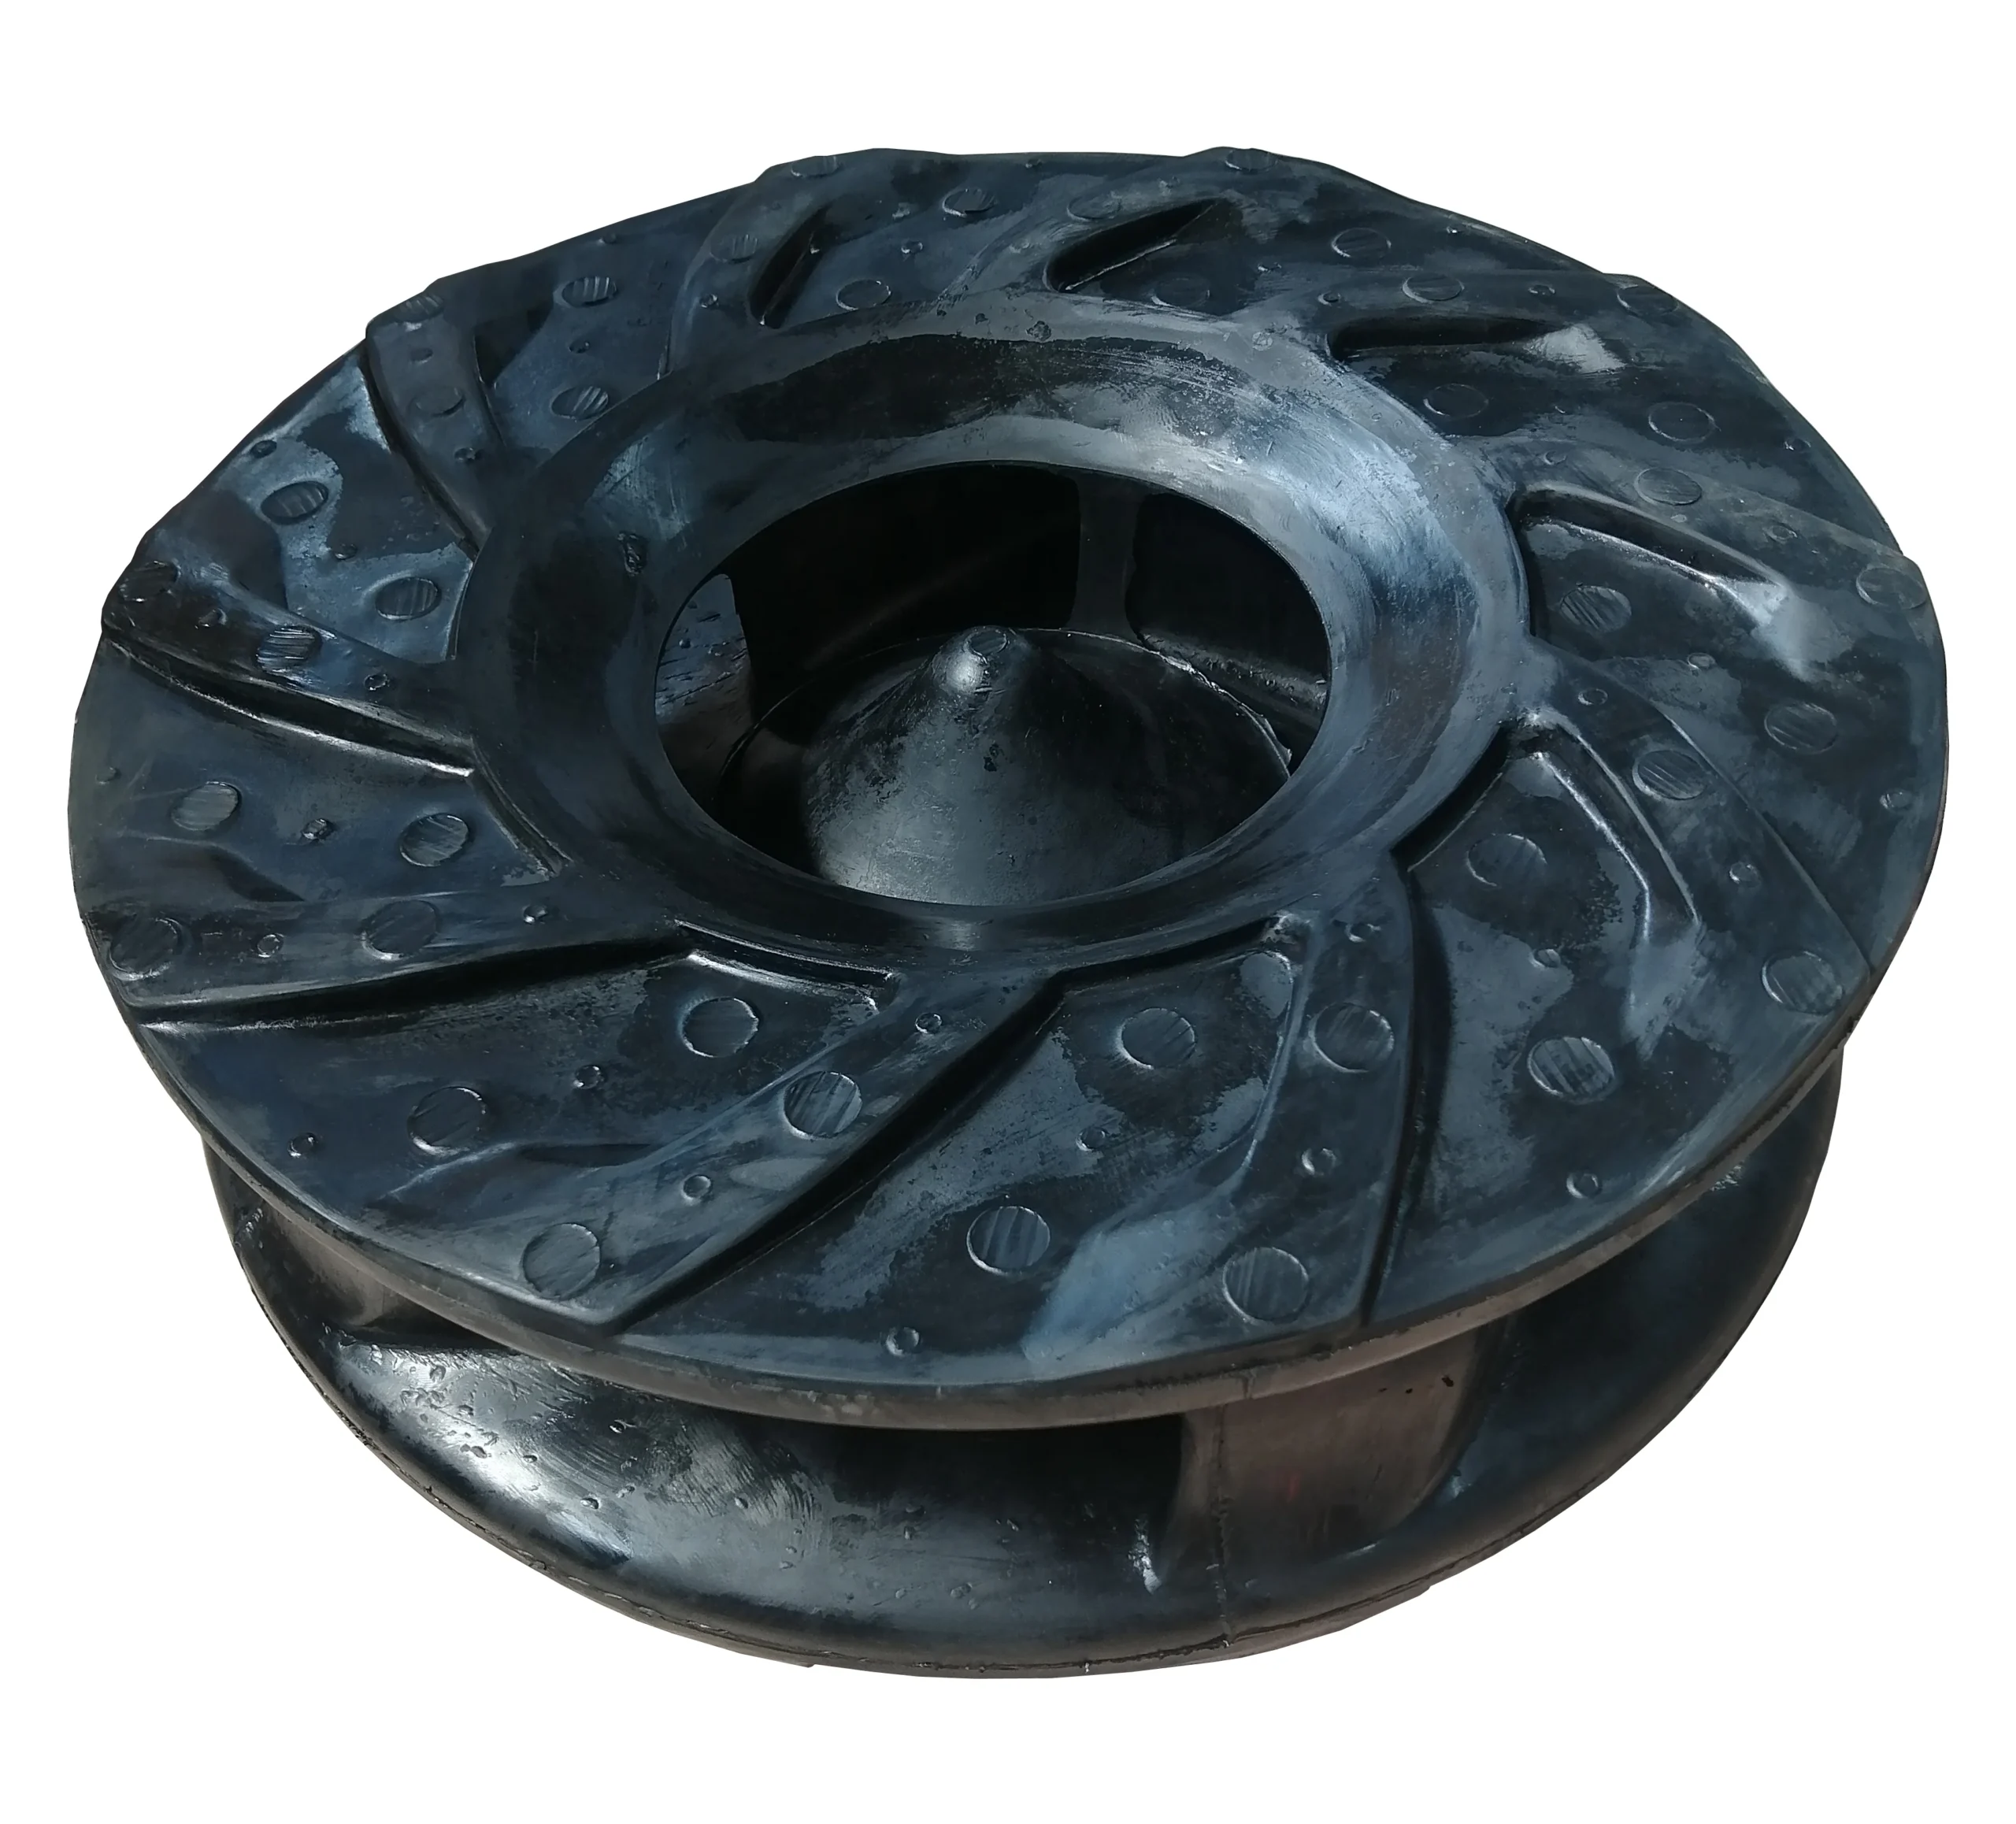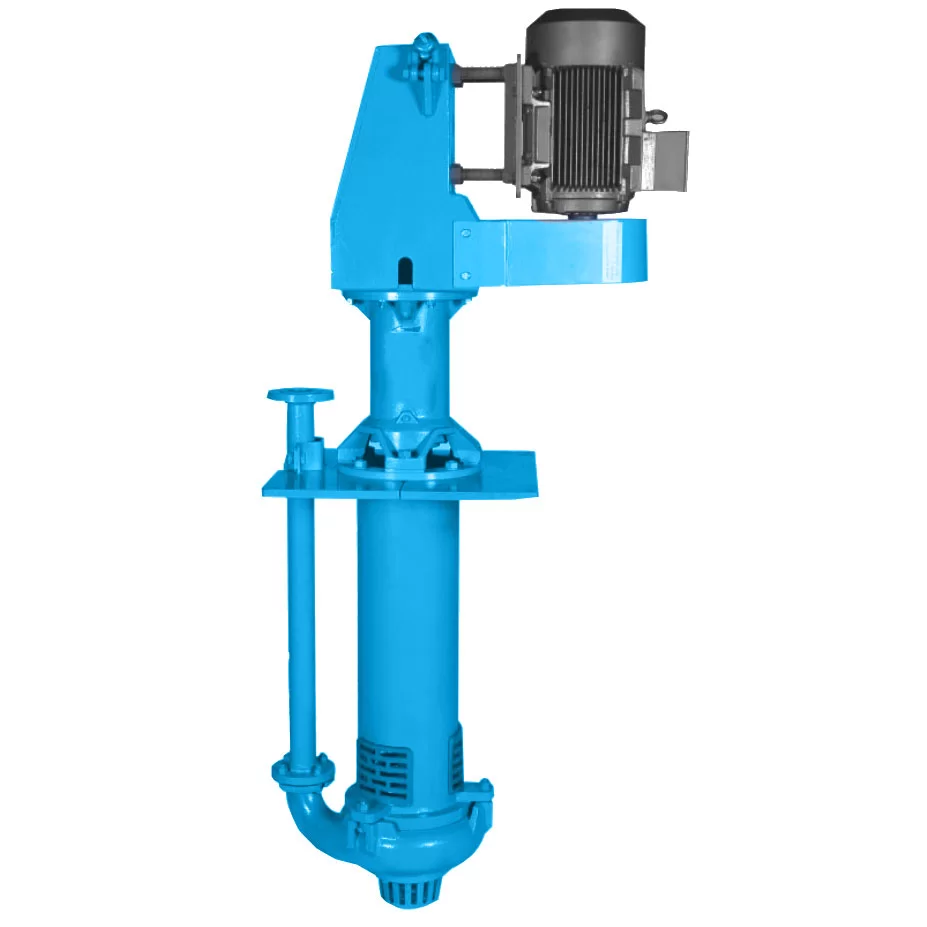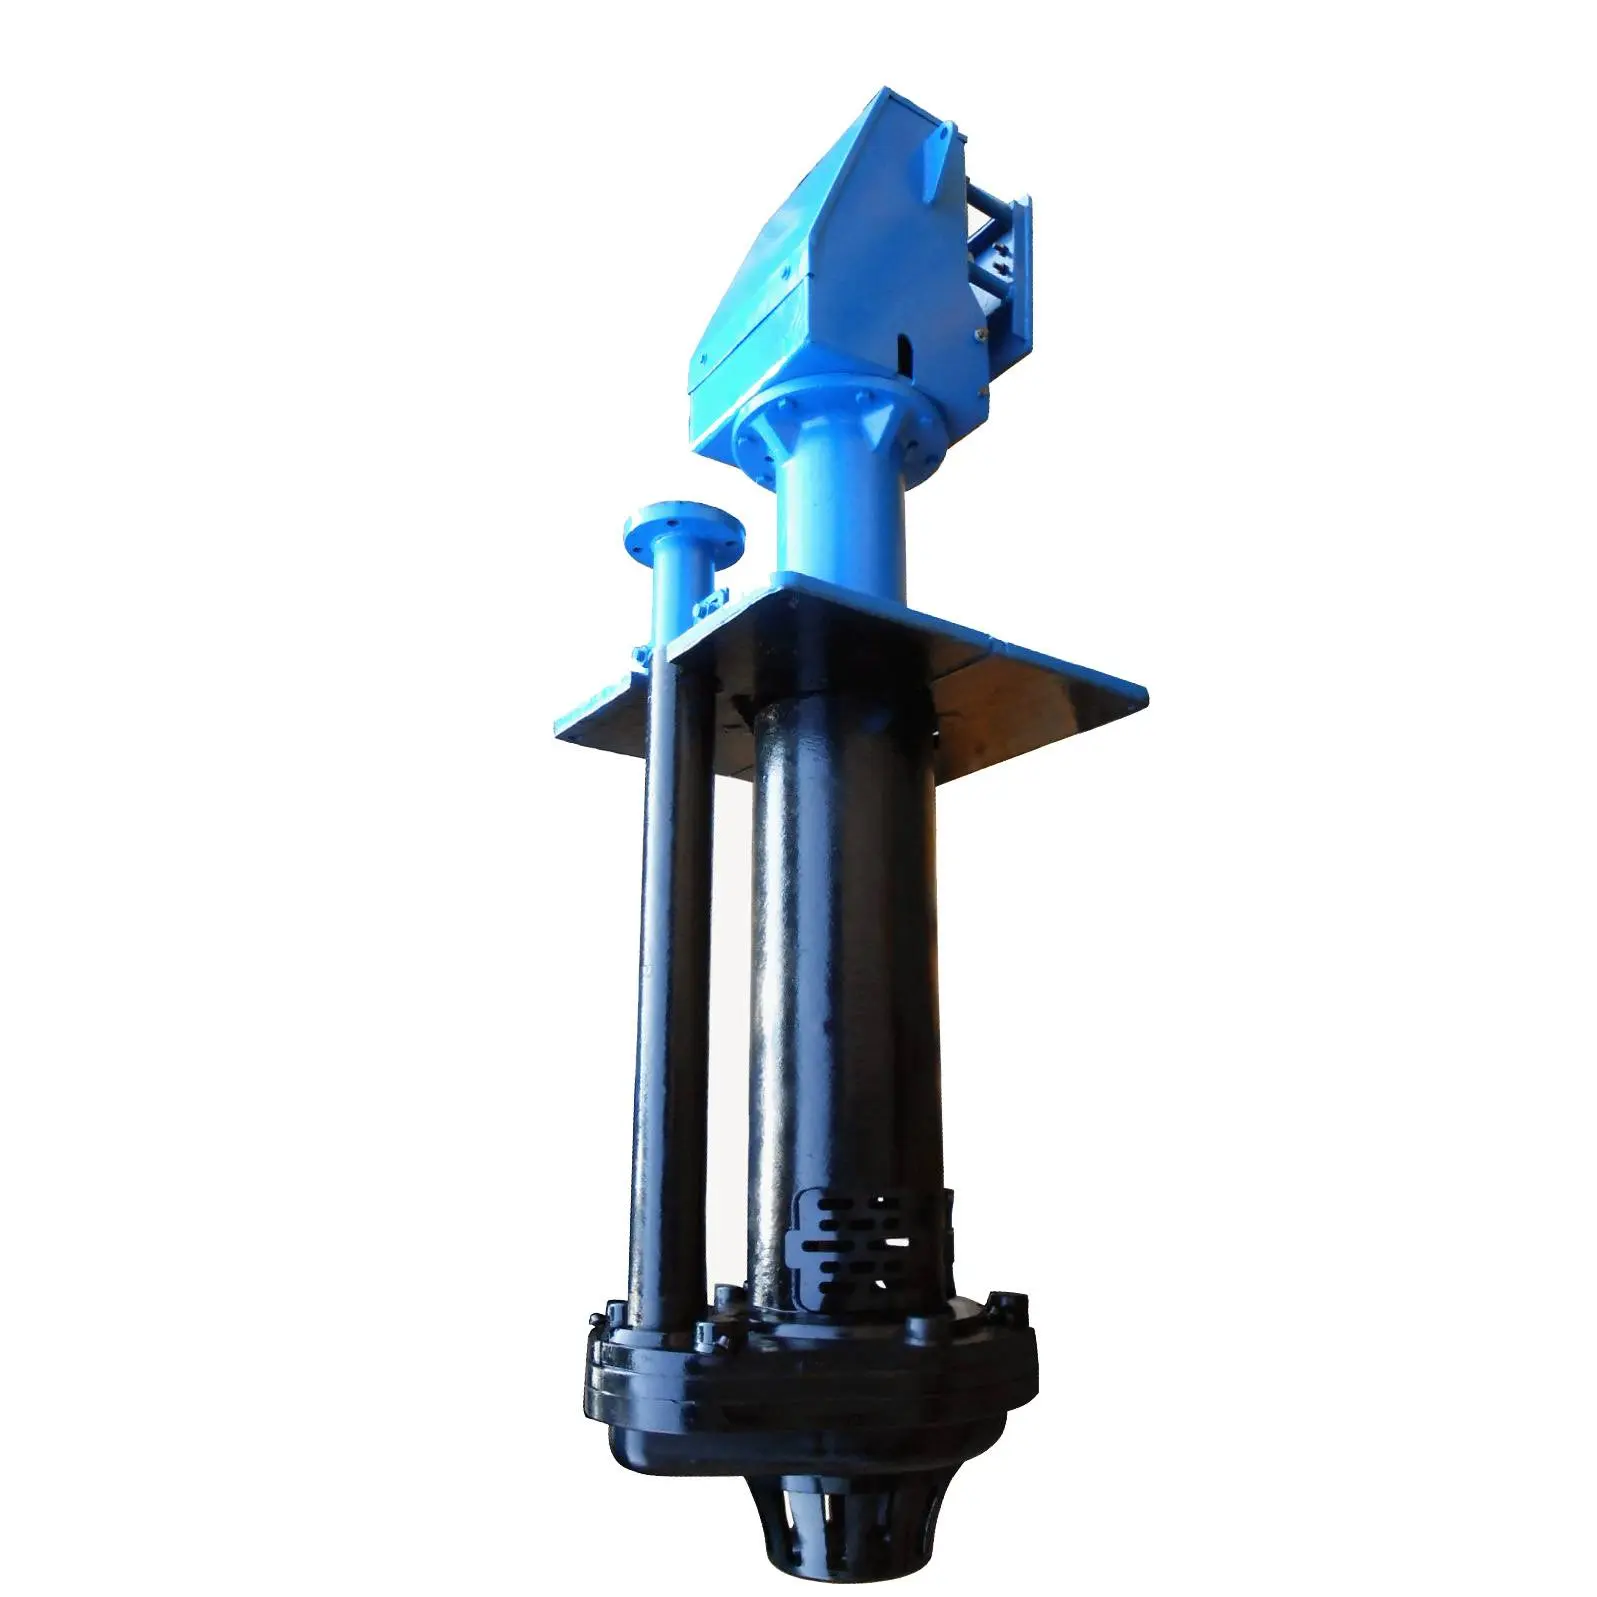
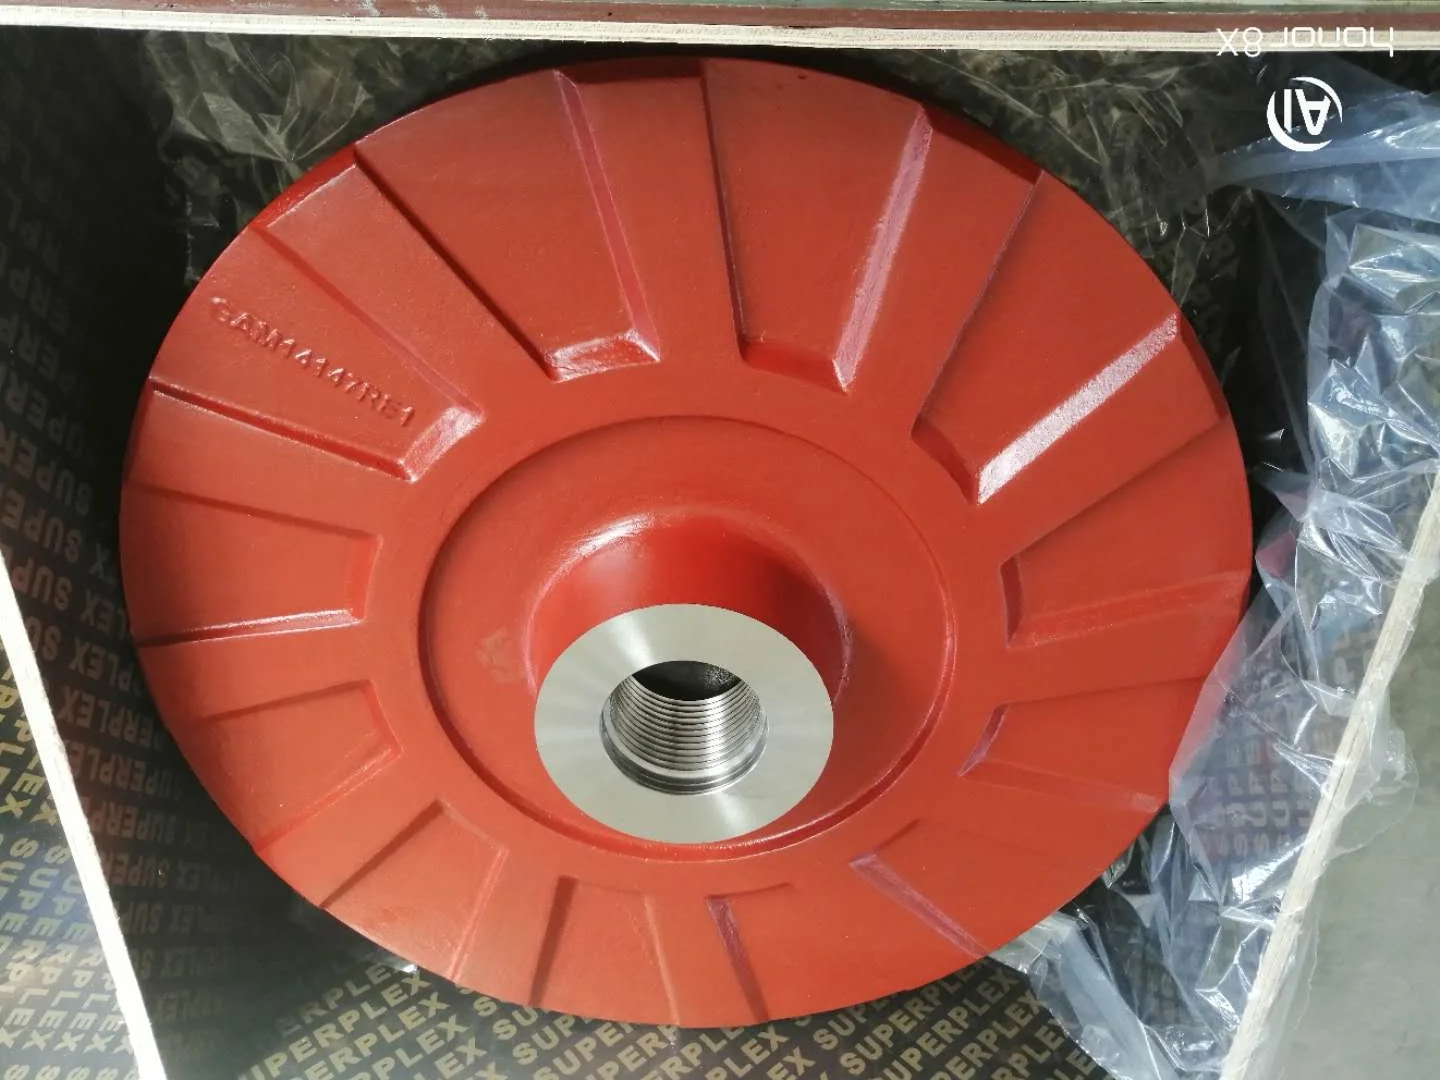
Finding a reliable China slurry pump expeller supplier is crucial for maintaining efficient operations in industries dealing with abrasive materials. Slurry pump expellers play a vital role in preventing leakage and ensuring the longevity of your pump. This article delves into the key considerations when sourcing expellers from China, exploring materials, applications, and the benefits of choosing a quality supplier like Quality Slurry Pump. We'll cover everything from understanding expeller types to ensuring compatibility with your existing pump systems.
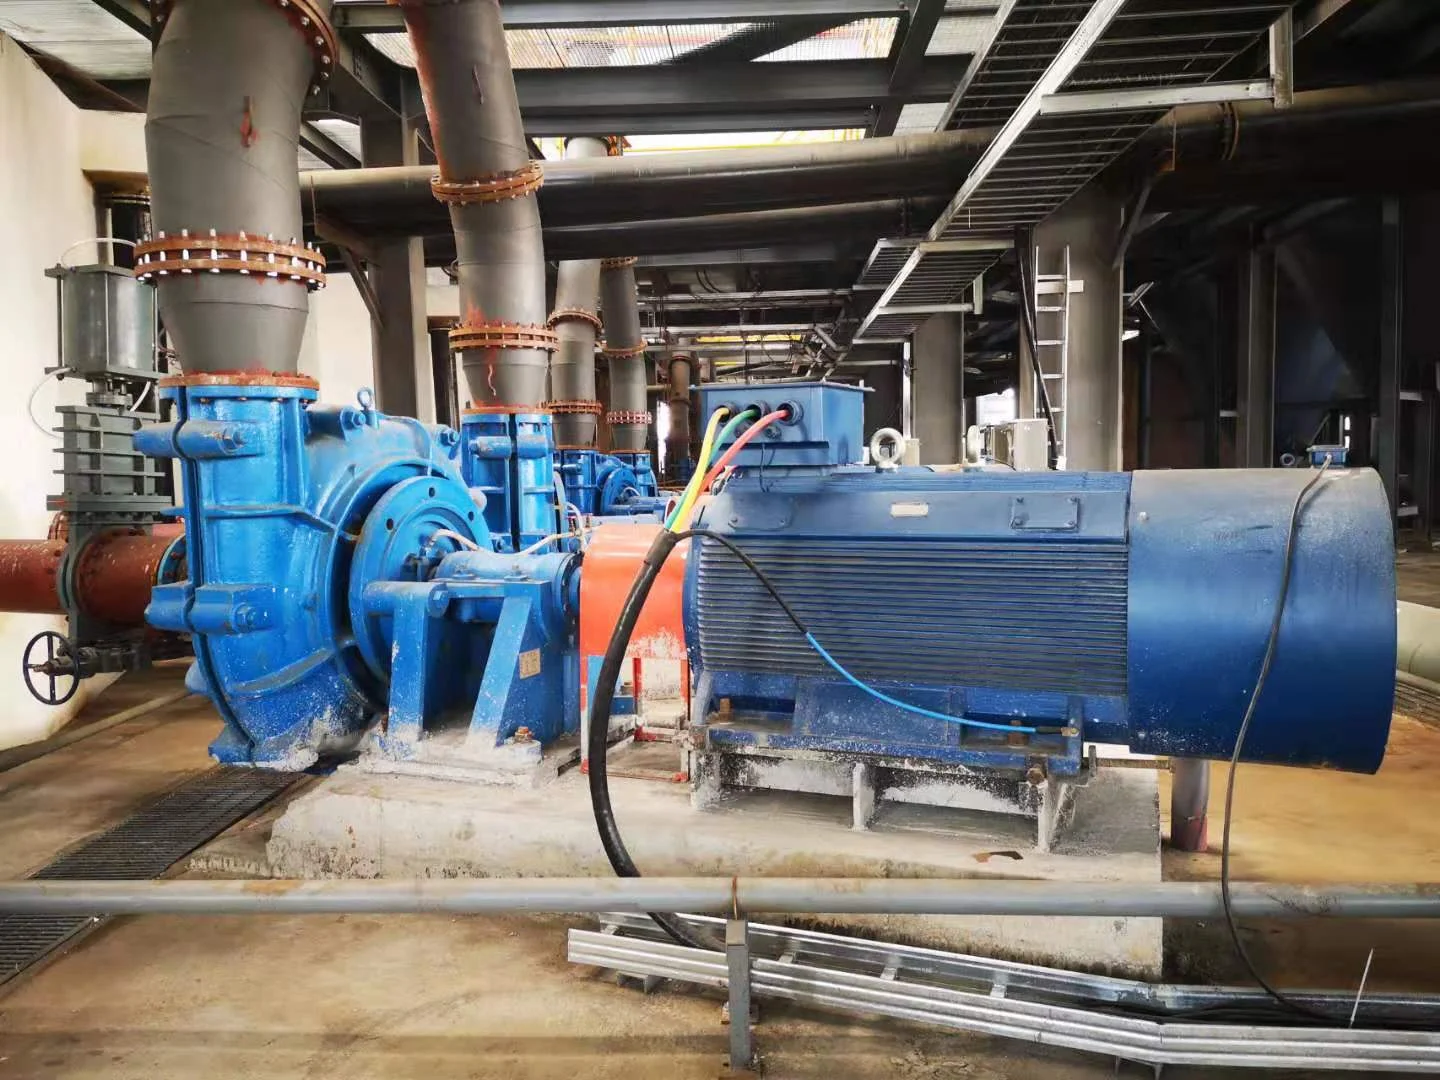
In the demanding landscape of mineral processing and industrial fluid transport, the efficiency of particle separation depends heavily on the precision of the feed system. A high-performance slurry pump for cyclone feed is essential for maintaining the constant pressure and flow rates required for hydrocyclones to operate at peak separation efficiency. Without a reliable pump, the entire classification circuit can suffer from instability, leading to poor product quality and increased waste. Globally, the demand for advanced slurry handling solutions has surged as mining operations move toward lower-grade ores, requiring higher throughputs and more rigorous processing stages.
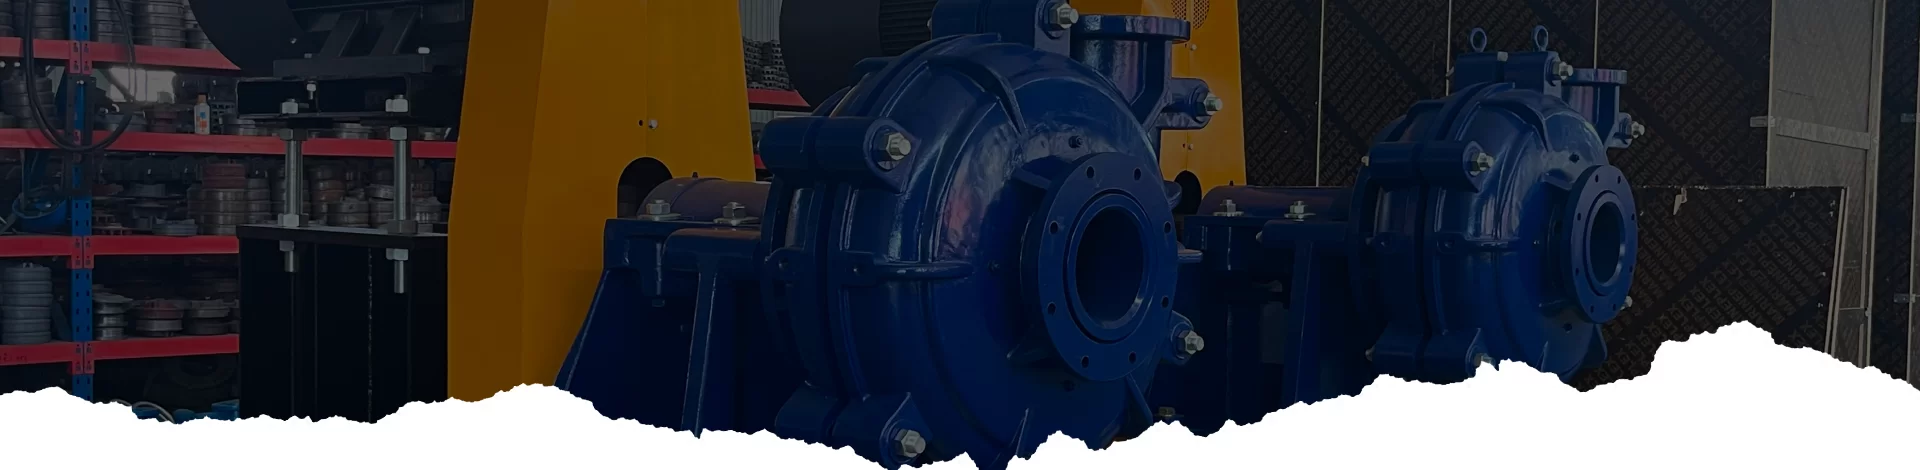
Engineered for reliability and efficiency in demanding mineral processing applications. Leading provider of slurry pump solutions for the mineral processing industry. As a leading manufacturer, we specialize in robust and efficient slurry pumps designed to handle the most abrasive and demanding mineral processing applications. Our pumps incorporate advanced hydraulic designs and durable materials to maximize performance, minimize downtime, and reduce total cost of ownership. Slurry pump for mineral processing plant are known for their reliability and longevity, even in the harshest operating conditions.
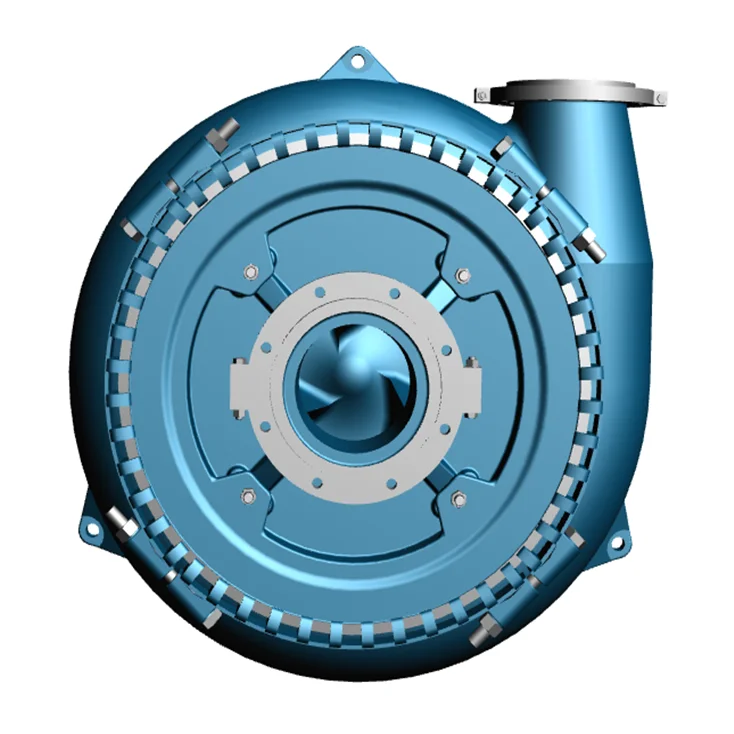
Slurry pumps for sand and gravel are critical components in numerous industries, from mining and construction to dredging and wastewater treatment. Their ability to efficiently transport abrasive mixtures over long distances is essential for project success and minimizing operational costs. Understanding the nuances of these pumps, including their design, materials, and operational parameters, is paramount for engineers, project managers, and operators alike. A properly selected and maintained slurry pump for sand and gravel significantly impacts productivity, reduces downtime, and extends the lifespan of the entire system. The global demand for infrastructure development, resource extraction, and environmental remediation continues to drive the need for reliable and efficient slurry pumping solutions. Growing populations and increasing urbanization necessitate large-scale construction projects, frequently involving significant volumes of sand and gravel. Furthermore, the need for responsible environmental practices demands effective solutions for managing sediment and pollutants in waterways, often relying on robust slurry pump for sand and gravel systems. According to the World Bank, global infrastructure investment is projected to reach $94 trillion by 2040, amplifying the importance of efficient material handling technologies.
Transporting abrasive fluids remains one of the most challenging aspects of mineral processing and chemical engineering. Slurry pumps are specialized machines designed to move mixtures of solids and liquids, where the solidsranging from mine tailings to chemical precipitatesact as aggressive agents that erode internal components. Selecting the right equipment requires a deep understanding of the fluids viscosity, particle size, and chemical composition to prevent premature failure and operational downtime. For industries such as mining, dredging, and metallurgy, off-the-shelf solutions often fail to address specific site conditions or unique material properties. This is where the expertise of a custom slurry pump manufacturer becomes essential.