Jun. 27, 2026
In the demanding realms of mining and mineral processing, the ability to move abrasive and corrosive materials efficiently is the backbone of operational success. A high pressure slurry pump is not merely a piece of equipment but a critical engineering solution designed to maintain flow stability under extreme conditions. Whether managing tailings or facilitating froth flotation, selecting a pump that balances hydraulic power with material durability is essential to prevent costly downtime. This guide explores the technical advantages of the 4E-AHF series and how it redefines performance standards in heavy-duty slurry handling.

The 4E-AHF Horizontal Froth Pump is specifically engineered to tackle the most abrasive slurries. By utilizing a combination of high-chromium metal and premium corrosion-resistant rubber, this pump ensures that internal wear is minimized even when transporting high-density mineral solids. The integration of specialized seal options, such as ZVZ and CV gland seals, allows the high pressure slurry pump to operate continuously without leakage, maintaining system pressure and preventing environmental contamination in harsh industrial sites.
Technical Edge: The optimized internal geometry reduces turbulence, which directly translates to higher hydraulic efficiency and a significant reduction in energy loss during high-volume discharge.
When evaluating a high pressure slurry pump, technical parameters are the primary indicators of suitability. The 4E-AHF series offers a versatile range of discharge sizes and flow rates to accommodate various plant scales. From small-scale pilot operations to massive mining complexes, the ability to scale flow up to 4550m³/hr ensures that the system can meet fluctuating production demands without compromising on head pressure or stability.
The Total Cost of Ownership (TCO) is where the 4E-AHF series truly outperforms standard alternatives. By reducing the frequency of maintenance from every 3 months to every 6-9 months, operators see a dramatic decrease in OpEx. The use of high-chrome impellers extends the wear life, ensuring that the high pressure slurry pump remains operational longer, which is critical for 24/7 mining cycles.
The application of a high pressure slurry pump extends beyond simple transport. In froth flotation, the 4E-AHF ensures a consistent feed of slurry to the cells, which is vital for maximum mineral recovery. Its compact footprint allows it to be integrated into existing pipelines without requiring massive site redesigns. This adaptability makes it an ideal choice for facilities looking to upgrade their capacity while minimizing structural changes.
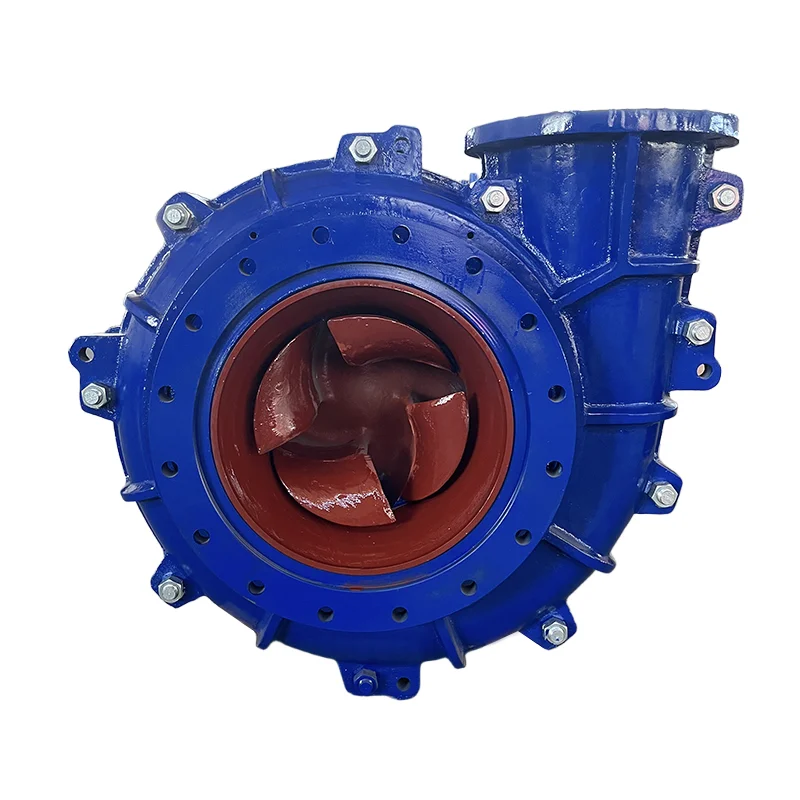
Downtime in a mining operation can cost thousands of dollars per hour. The 4E-AHF high pressure slurry pump is designed for accessibility. Technicians can perform routine checks and replace wear liners with minimal effort. Furthermore, with the integration of modern performance analytics, operators can now utilize predictive alerts to schedule maintenance based on actual operational hours rather than guesswork, ensuring zero unplanned downtime.
Selecting the right wet-end material is the most critical decision when deploying a high pressure slurry pump. For chemically aggressive slurries, corrosion-resistant rubber provides the best defense against degradation. Conversely, for highly abrasive mineral solids, high-chromium metal is the superior choice due to its hardness. The 4E-AHF provides both options, allowing users to customize the pump to their specific slurry chemistry, thereby maximizing the service interval of all internal components.
Investing in a high-performance high pressure slurry pump like the 4E-AHF series is a strategic move toward operational excellence. By combining superior material science with hydraulic efficiency, this pump reduces energy costs and maintenance overhead while maximizing output. In an industry where reliability is everything, choosing equipment that guarantees stability under pressure is the only way to maintain a competitive edge.
The choice depends entirely on the medium being pumped. For chemically aggressive or corrosive slurries, corrosion-resistant rubber is the recommended choice as it prevents chemical erosion. For highly abrasive mineral solids with high quartz or grit content, high-chromium metal is superior due to its extreme hardness and resistance to physical wear. Selecting the wrong material can lead to rapid component failure and increased downtime.
The 4E-AHF utilizes a robust horizontal structural design specifically balanced to handle the centrifugal forces associated with high-pressure discharge. It employs specialized seal configurations (ZVZ, CV, CRZ, and CLZ) that create a tight seal around the shaft, preventing leakage and maintaining the necessary head pressure for efficient slurry transport across long pipeline distances.
No, the 4E-AHF is designed with "Simplified Serviceability." Its layout allows technicians quick access to the impeller and wet-end components without needing to dismantle the entire pipeline. This design focus reduces the time required for routine parts replacement, ensuring that the pump returns to service as quickly as possible to minimize production losses.
The 4E-AHF series is highly scalable, capable of achieving a maximum flow rate of up to 4550m³/hr (approximately 20,000 GPM). The actual flow rate will depend on the specific model selected, the discharge size (ranging from 50mm to 550mm), and the required head pressure for your specific application. You can find detailed sizing guides on the Quality Slurry Pump website.
Mar 14,26
Find a Reliable China Slurry Pump Shaft Sleeve Supplier for Optimal Performance
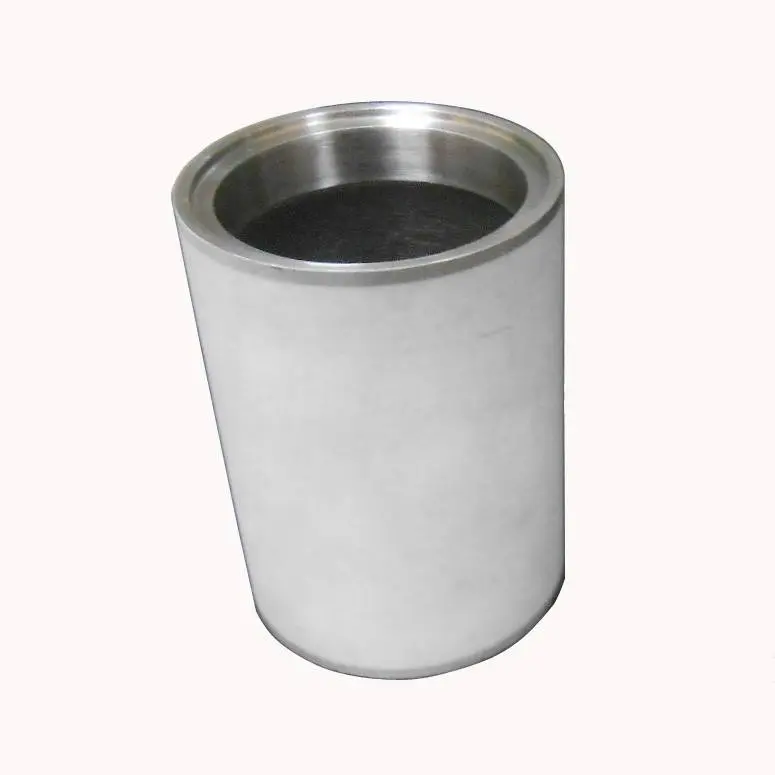
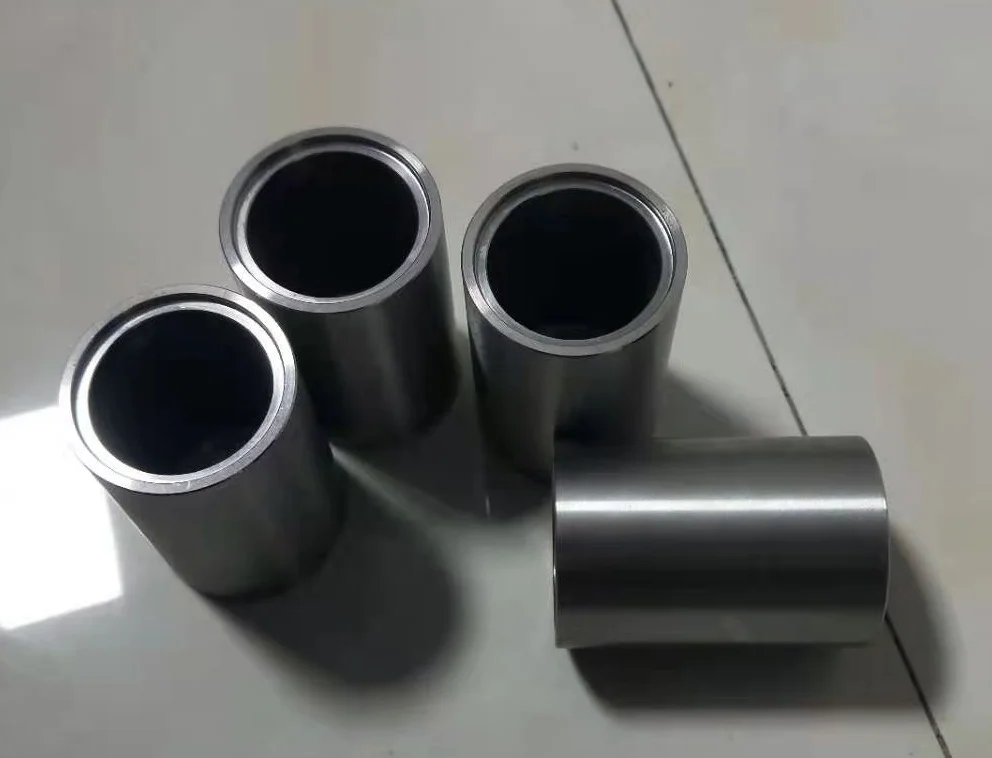
When sourcing replacement parts for your slurry pump, the shaft sleeve is a critical component. A reliable China slurry pump shaft sleeve supplier ensures optimal pump performance, extends equipment lifespan, and minimizes downtime. At Quality Slurry Pump, we specialize in providing high-quality, durable shaft sleeves tailored to a wide range of slurry pump applications. Choosing the right supplier is crucial, and we'll explore the key considerations in this article. We aim to provide a comprehensive guide to understanding shaft sleeve specifications, materials, and the benefits of partnering with a trusted manufacturer. Slurry pump shaft sleeves are cylindrical components that fit over the pump shaft, protecting it from abrasive wear caused by the slurry being pumped. They are essential for maintaining the pump’s efficiency and preventing costly repairs. The sleeve wears out instead of the shaft, offering significant cost savings in the long run. Different applications require different materials and designs, depending on the slurry’s composition, particle size, and concentration.
Oct 31,25
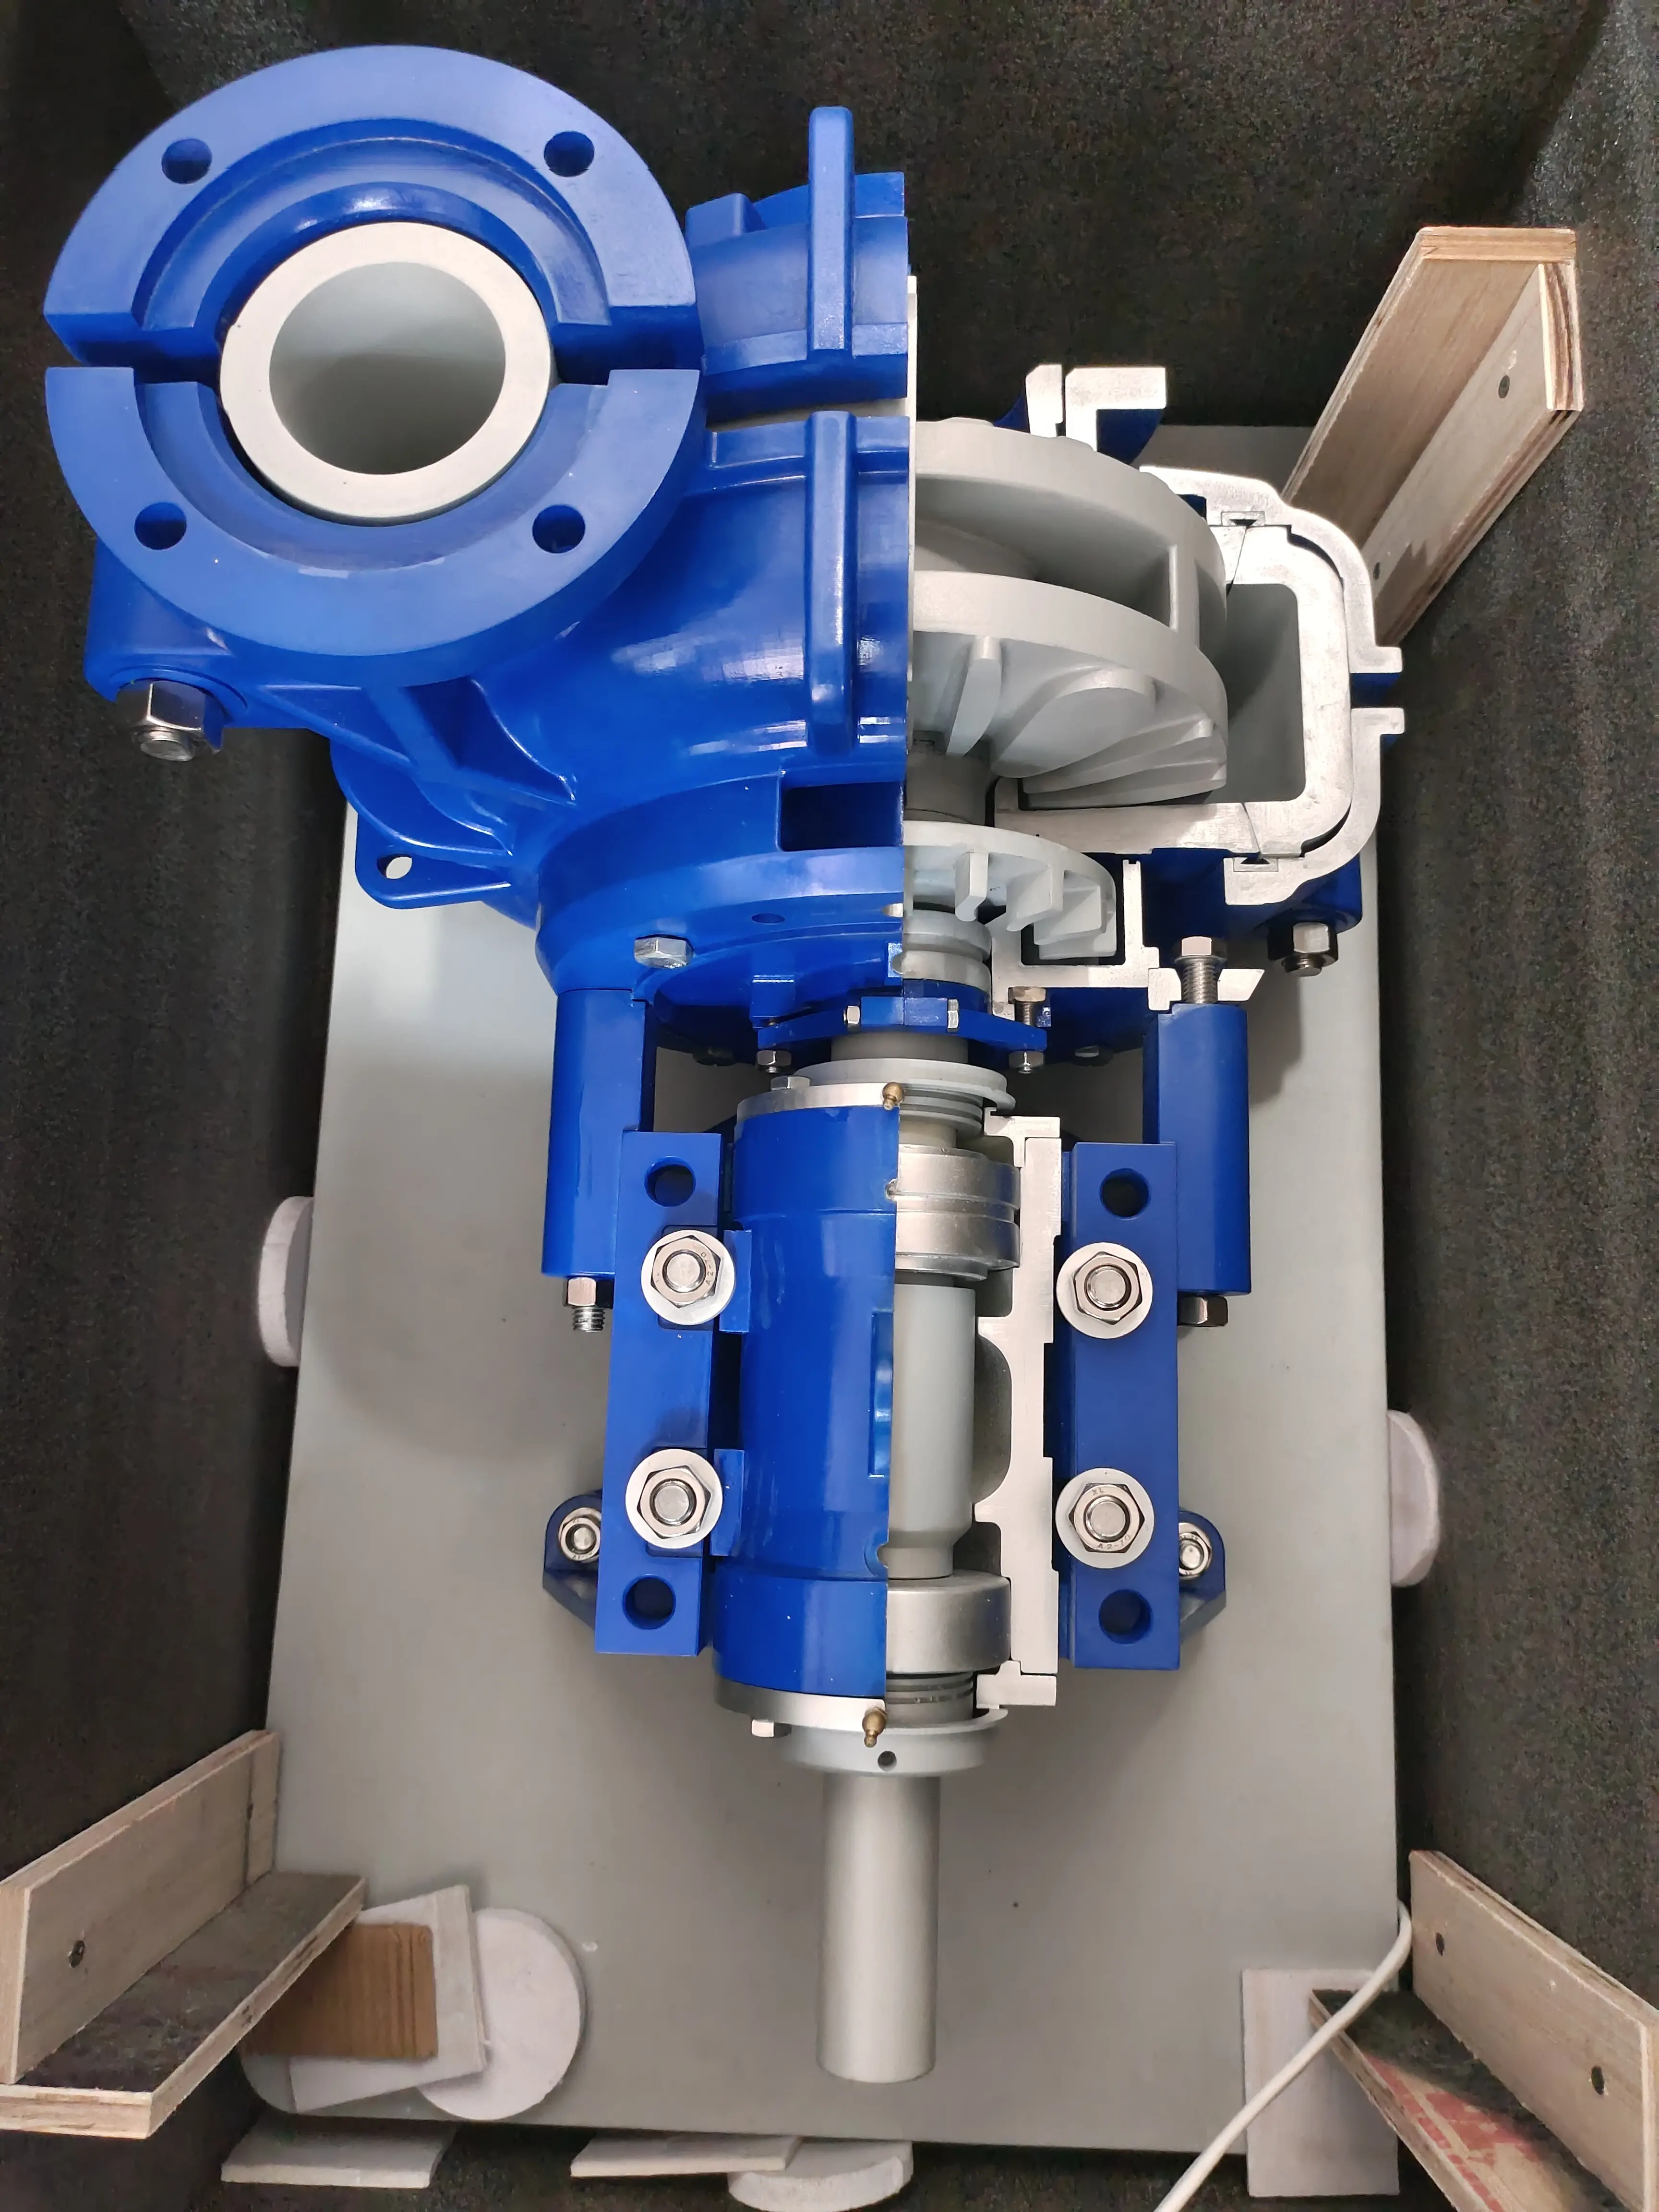
A slurry pump model brought to the exhibition
Feb 27,26
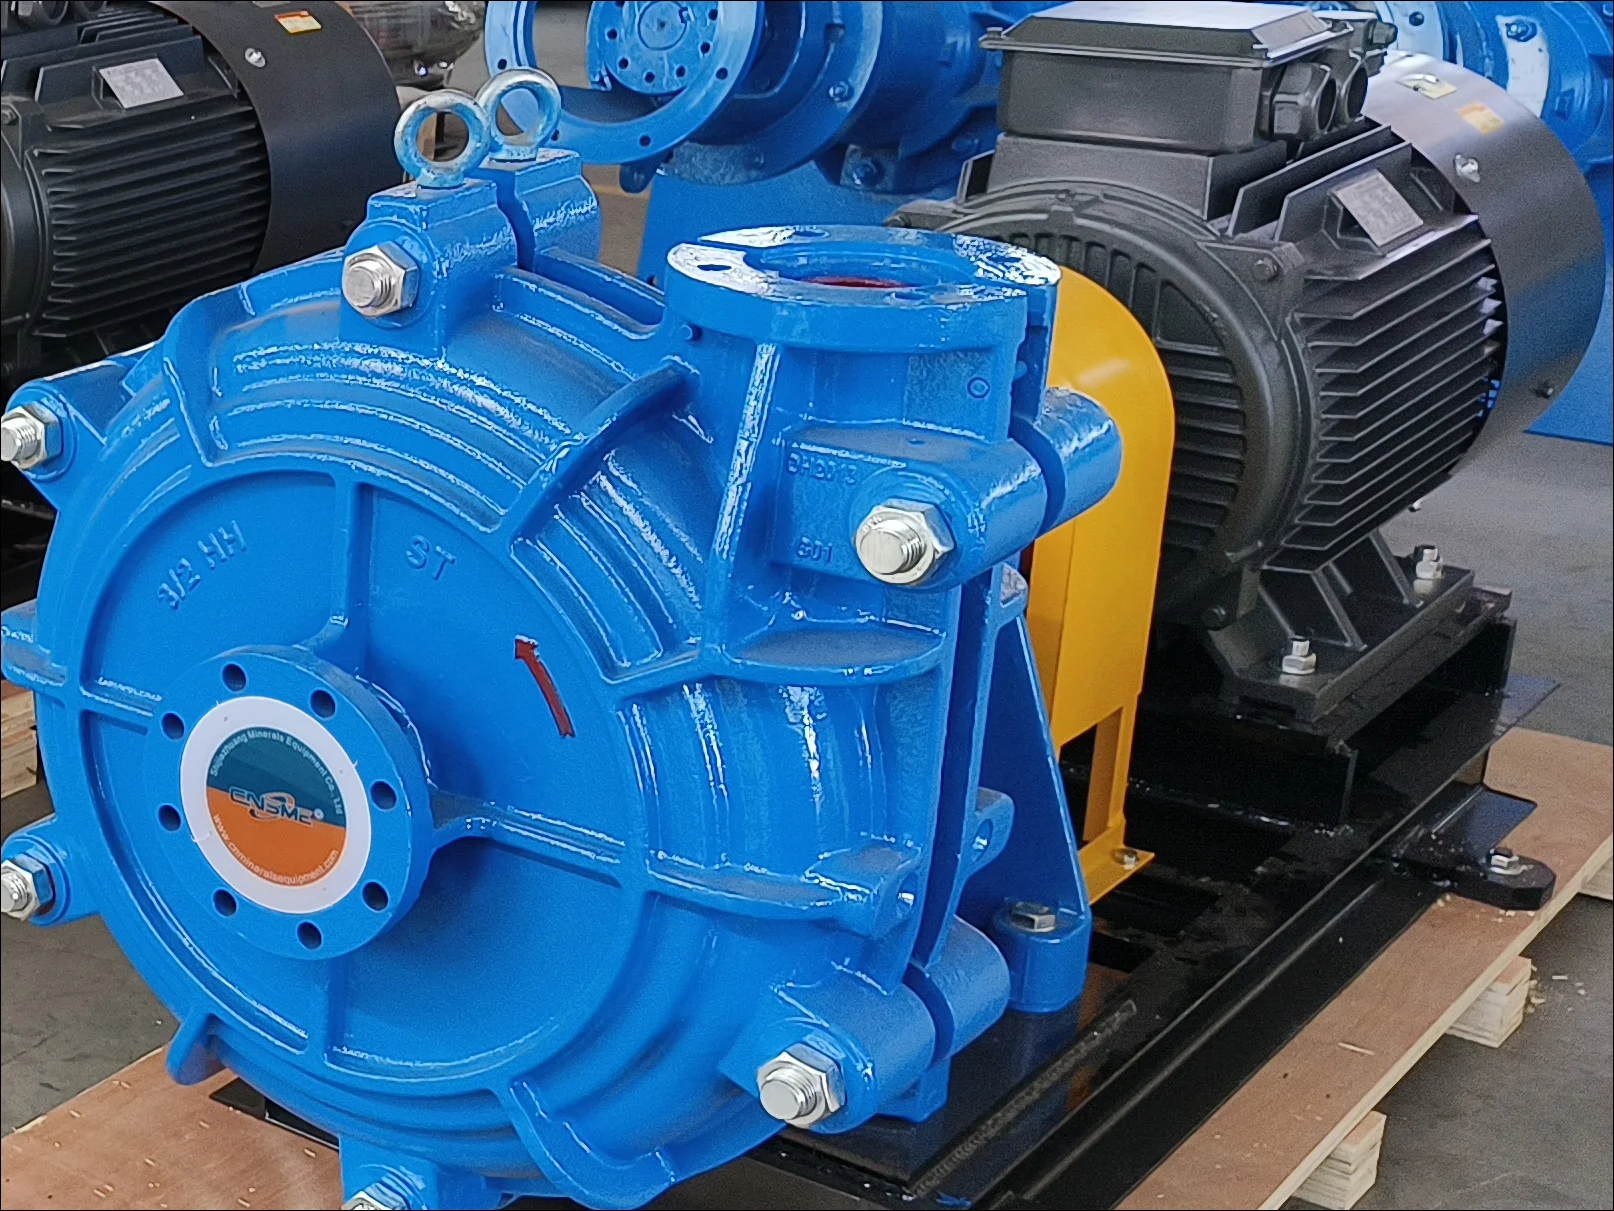
Optimizing Slurry Pump Performance for Efficient Copper Mine Operations

Jul 06,26
Industrial Wear Resistant Slurry Pump for Mining and Chemical
Dec 02,25
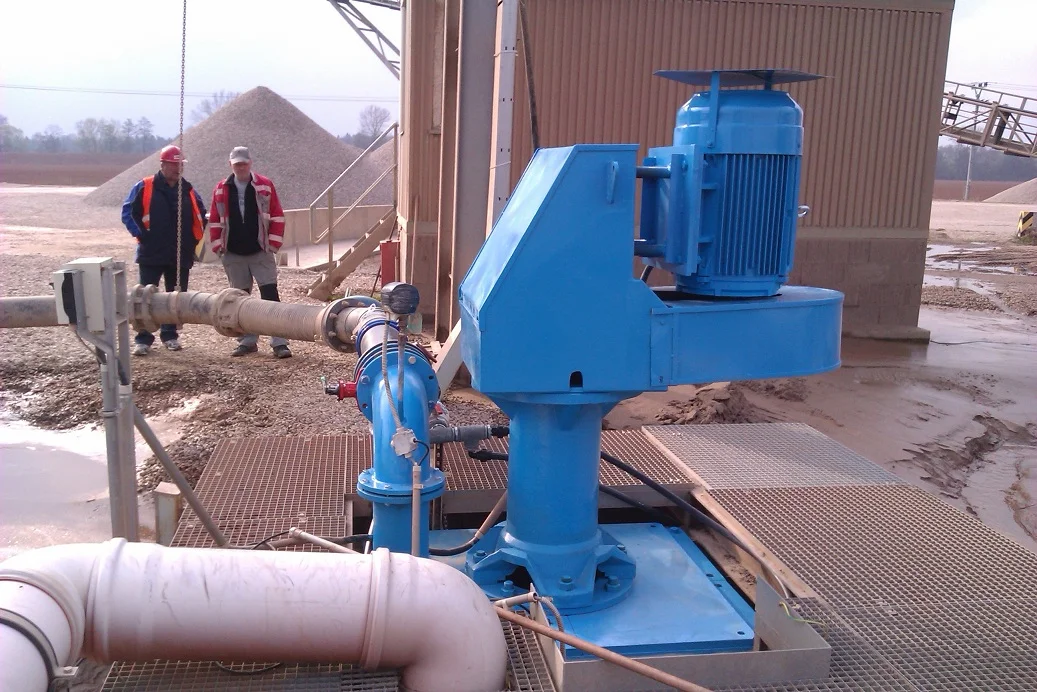
Which Slurry Pump Is Better: Vertical or Horizontal?
Different slurry pumps are designed for different needs: some are ideal for tight spaces, while others are built to move large volumes of material quickly.
Apr 23,26
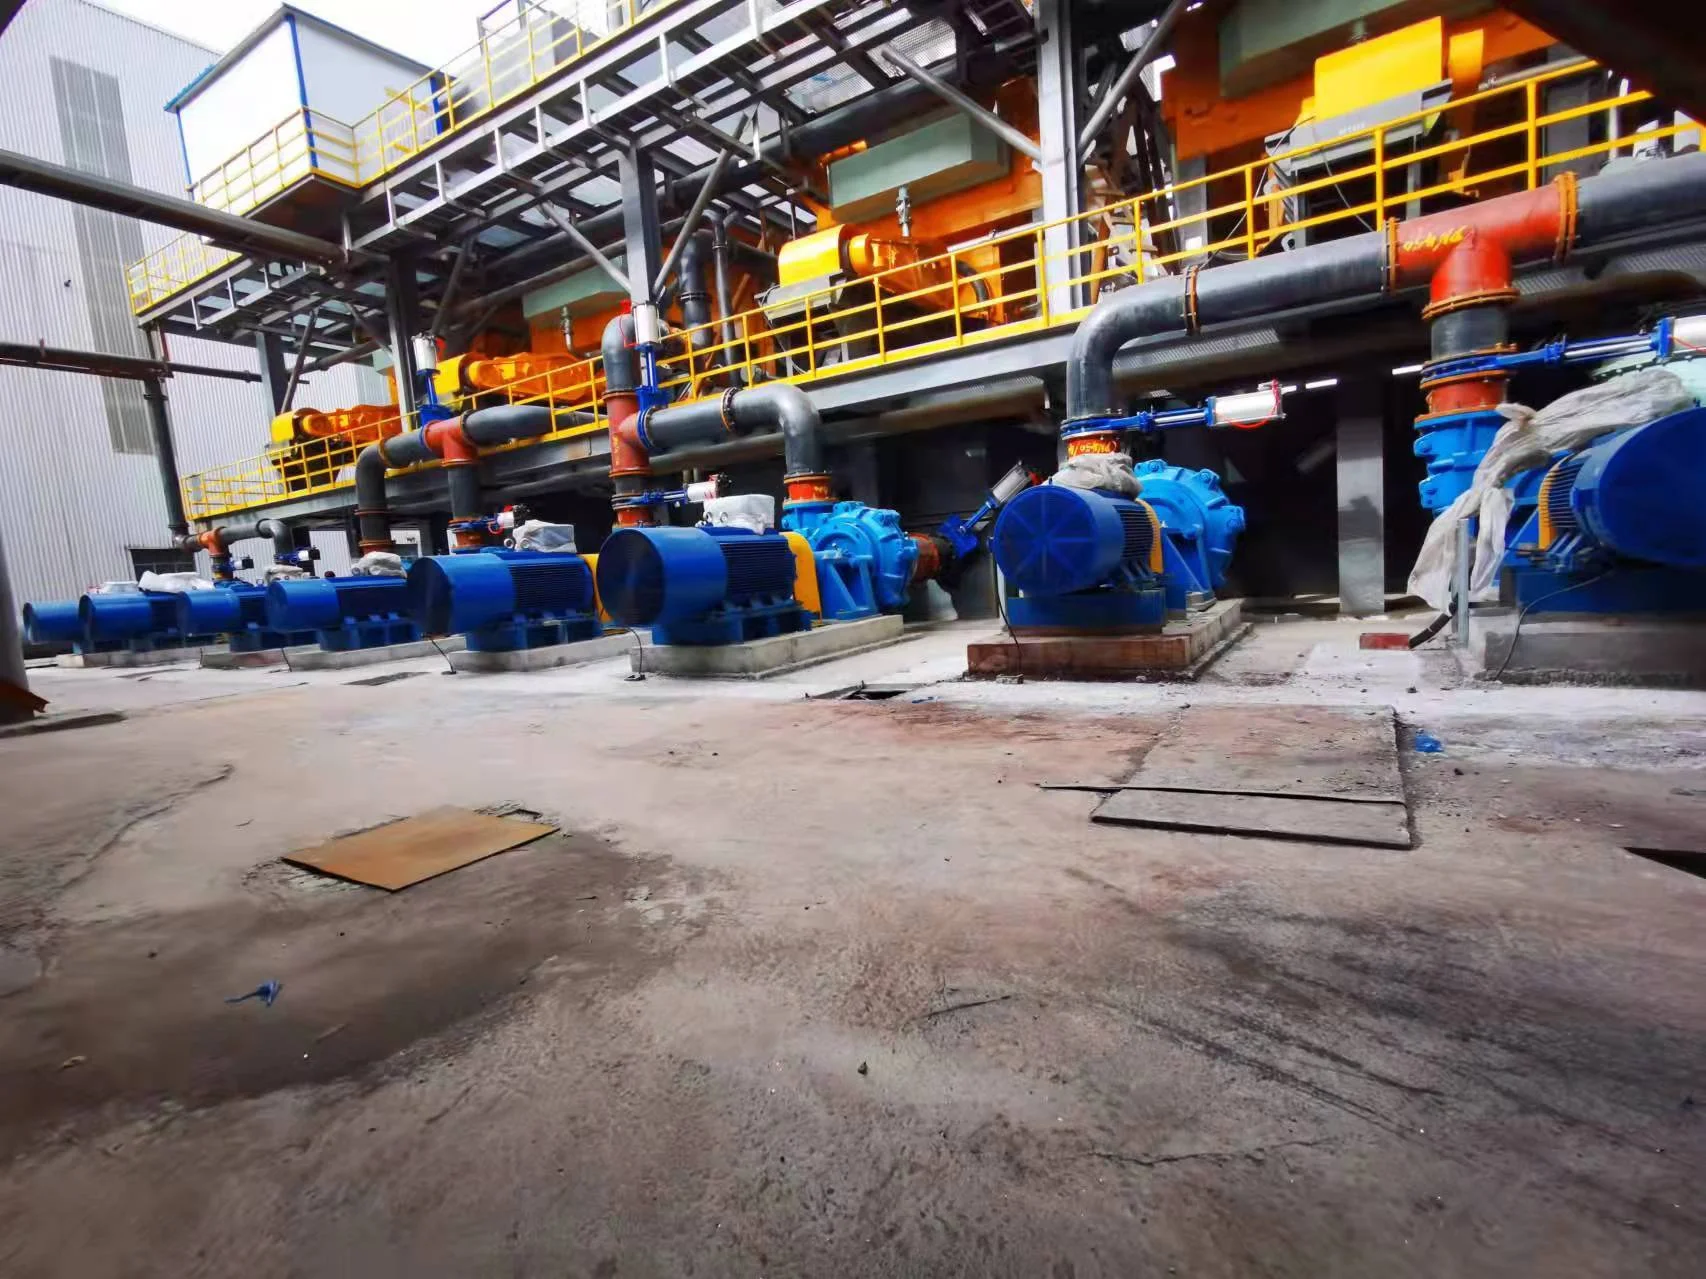
Reliable Heavy Duty Slurry Pump Supplier for Industrial Mining
bscribe newslette