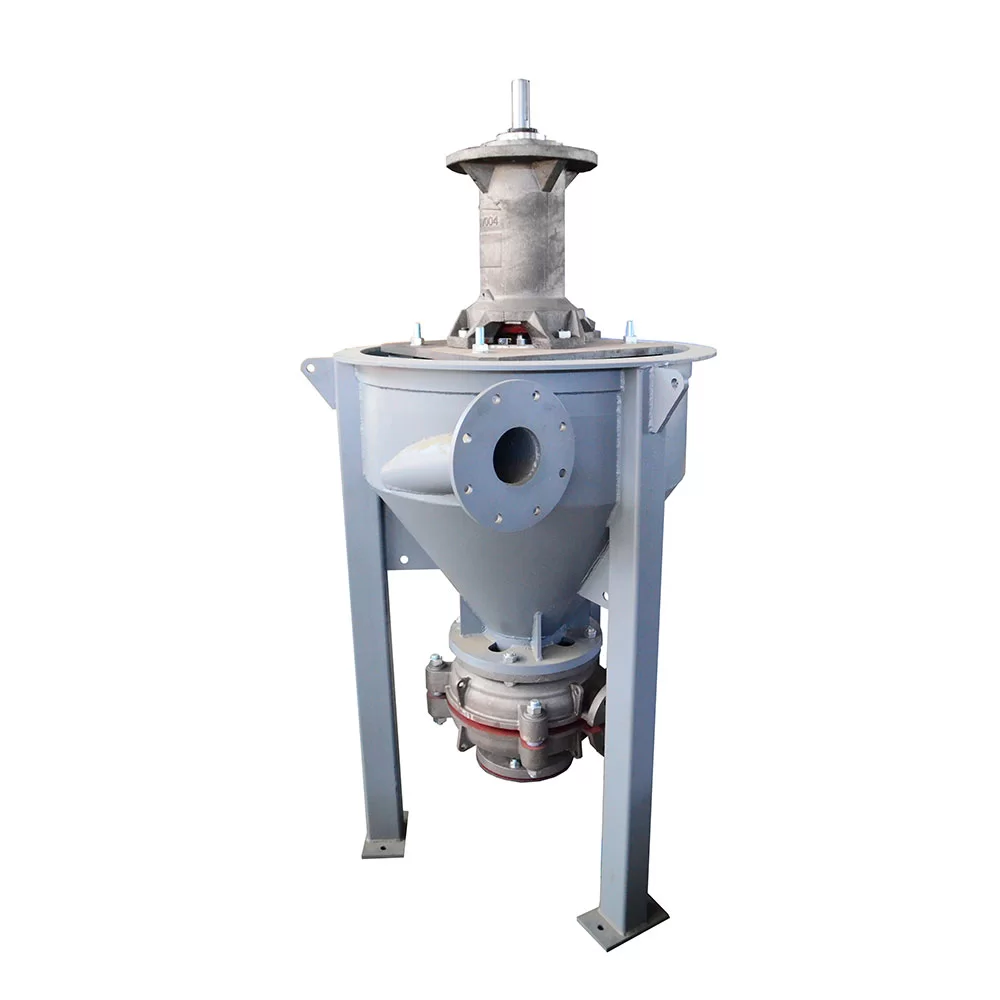
The slurry pump is a pump that conveys a mixture of solids and water. Therefore, the medium will be abrasive to the flowing parts of the slurry pump. Therefore,
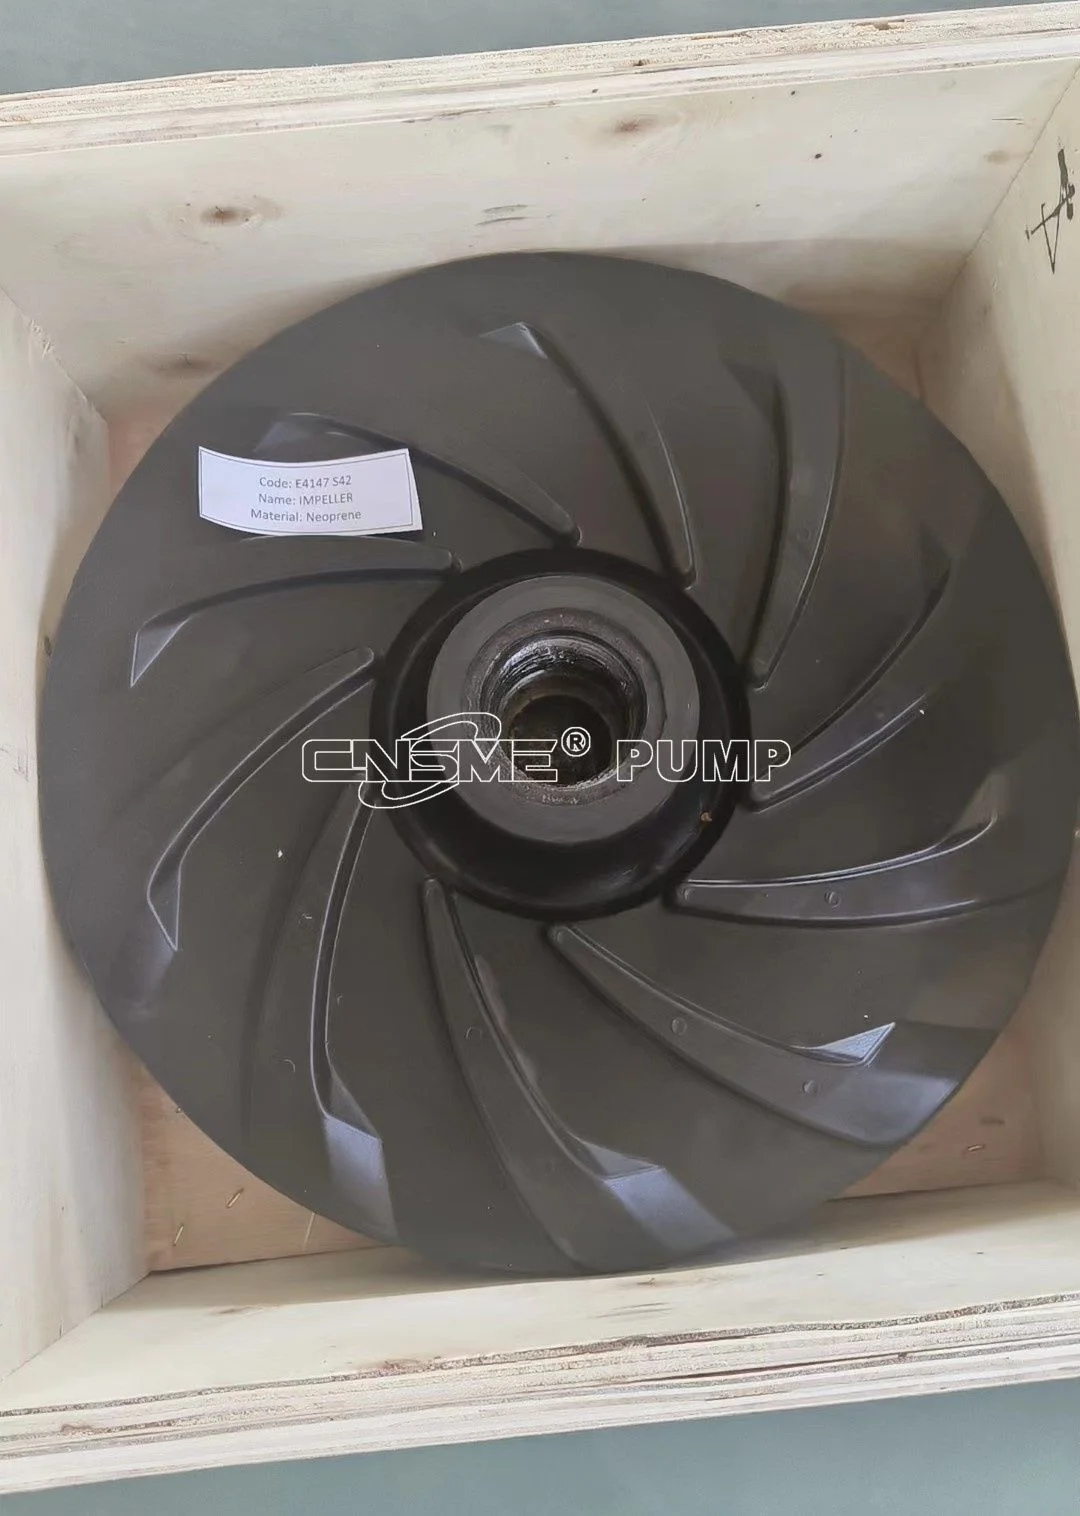
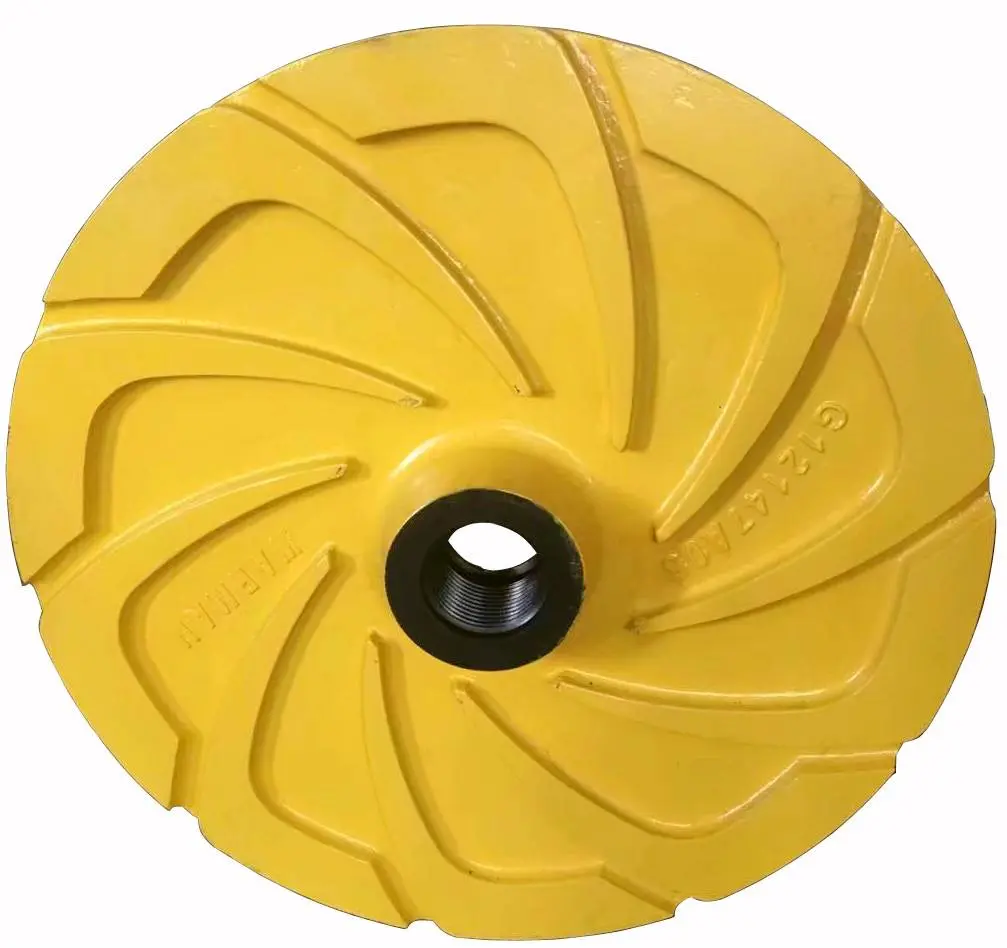
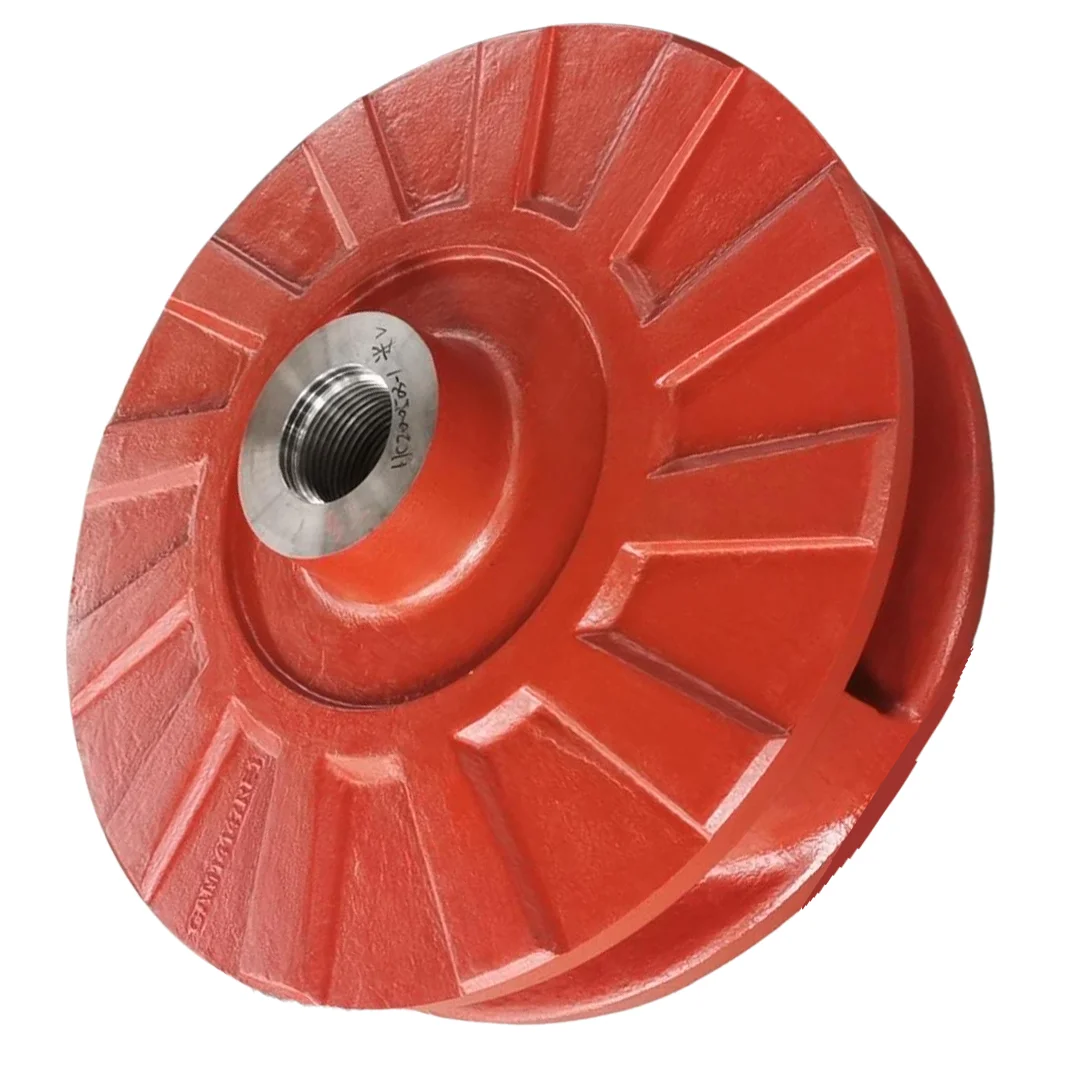
When it comes to demanding applications like mining, wastewater treatment, and industrial processing, the reliability of your slurry pump is paramount. A critical component often overlooked is the slurry pump expeller. As a leading China slurry pump expeller factory, we specialize in manufacturing high-quality, durable expellers designed to optimize pump performance and extend its lifespan. This article will explore the function of slurry pump expellers, the materials used, key considerations when choosing a supplier, and how Quality Slurry Pump can meet your specific needs.
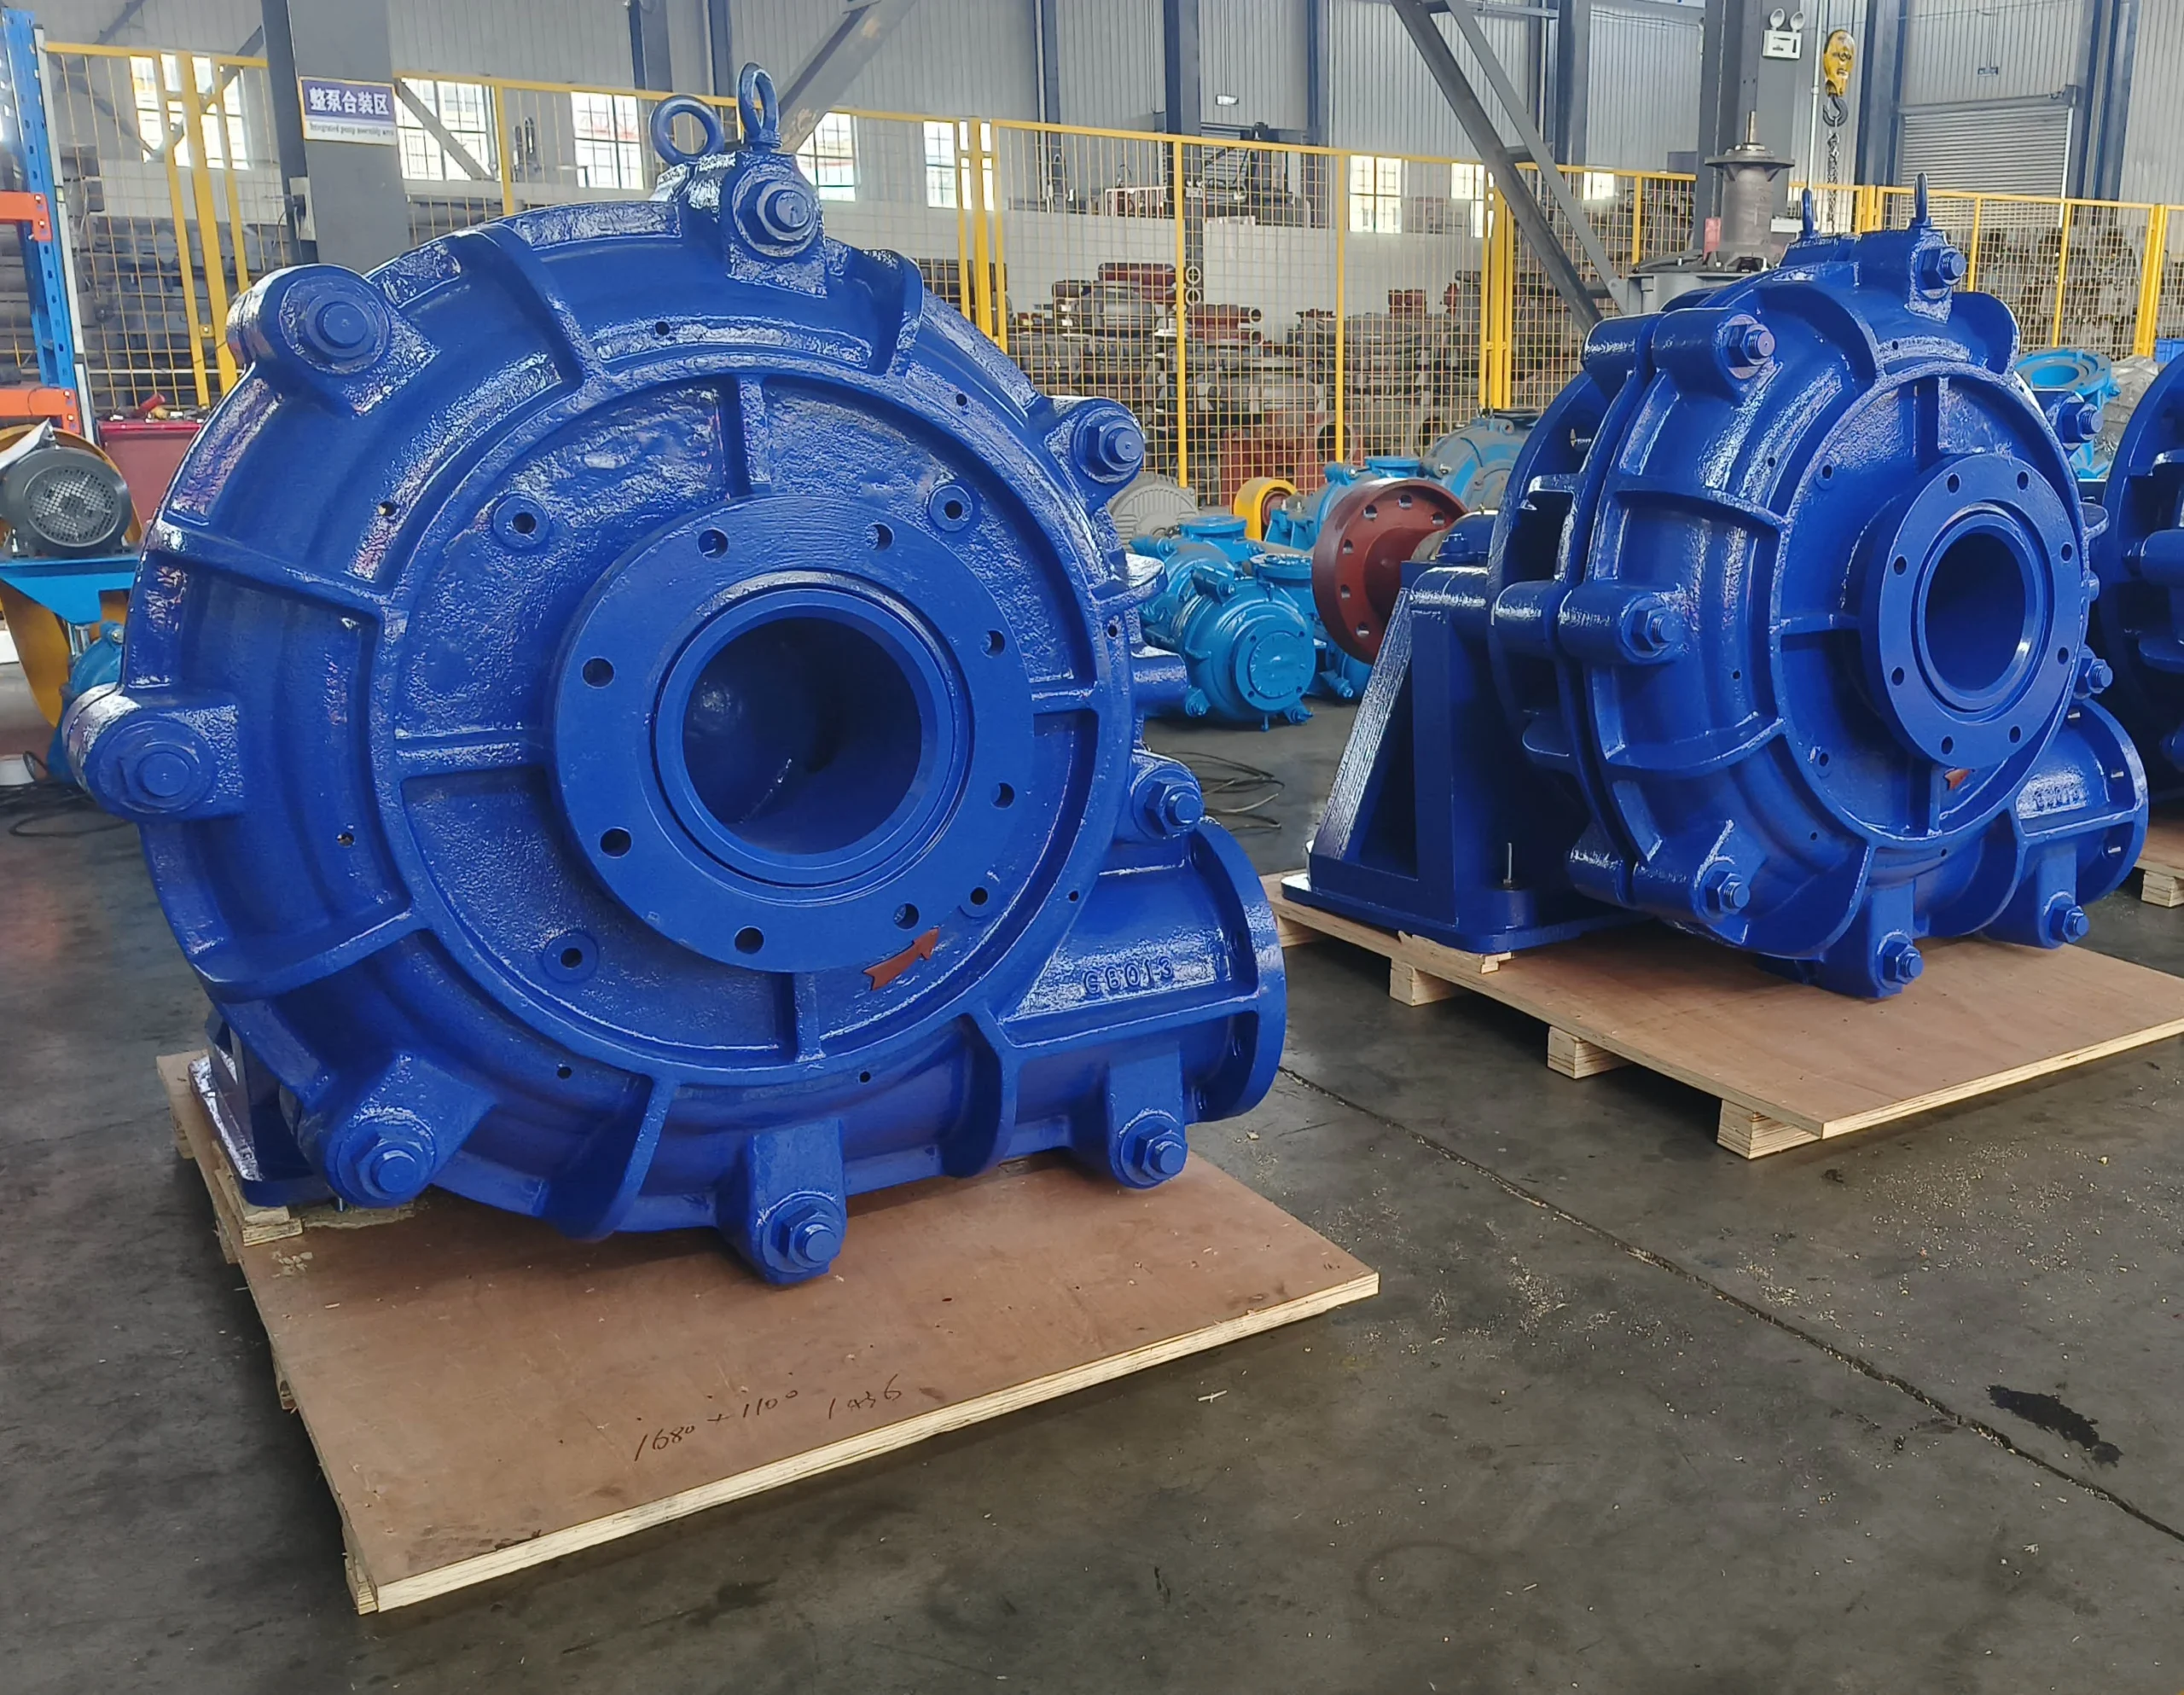
In the demanding world of minerals processing and tailings management, the ability to move abrasive, high-density materials efficiently is a critical operational requirement. The use of a specialized horizontal slurry pump ensures that mining and industrial plants can maintain continuous flow without frequent breakdowns, directly impacting the overall profitability and safety of the site. By leveraging heavy-duty centrifugal designs, these machines bridge the gap between raw material extraction and refined processing. Across the global mining landscape, from copper mines in Chile to iron ore operations in Australia, the challenge of overweight applications such as mill discharge and high-pressure pipeline transport requires equipment
Reliable and efficient slurry transportation is critical in mining, metallurgy, power, and chemical industries! CNSME recommends the AH/AHR heavy-duty slurry
In the demanding world of industrial mineral processing and wastewater management, the double casing slurry pump stands as a critical piece of engineering designed to handle the most abrasive and corrosive fluids. By incorporating a dual-wall structure, these pumps provide an essential layer of protection that ensures operational continuity in environments where standard pumps would fail within weeks. The global shift toward more efficient mining practices and stricter environmental regulations has increased the demand for equipment that minimizes leakage and maximizes uptime. A double casing slurry pump addresses these challenges by isolating the primary wear components from the external environment.
The transportation of abrasive materials in industrial environments requires specialized equipment capable of overcoming significant resistance and elevation. A high head slurry pump is engineered specifically for these demanding conditions, ensuring that thick, abrasive fluids can be moved efficiently over long distances or to elevated discharge points without compromising system integrity. In global mining and mineral processing, the ability to maintain high pressure per stage is critical for operational throughput. By utilizing advanced metallurgy and hydraulic design, these pumps minimize the need for excessive booster stations, thereby reducing both the initial capital expenditure and the long-term energy costs associated with slurry transport.