Dec 05,25
Vietnam Client Visit Update | On-Site Discussion for Vertical Slurry Pump Project Optimization
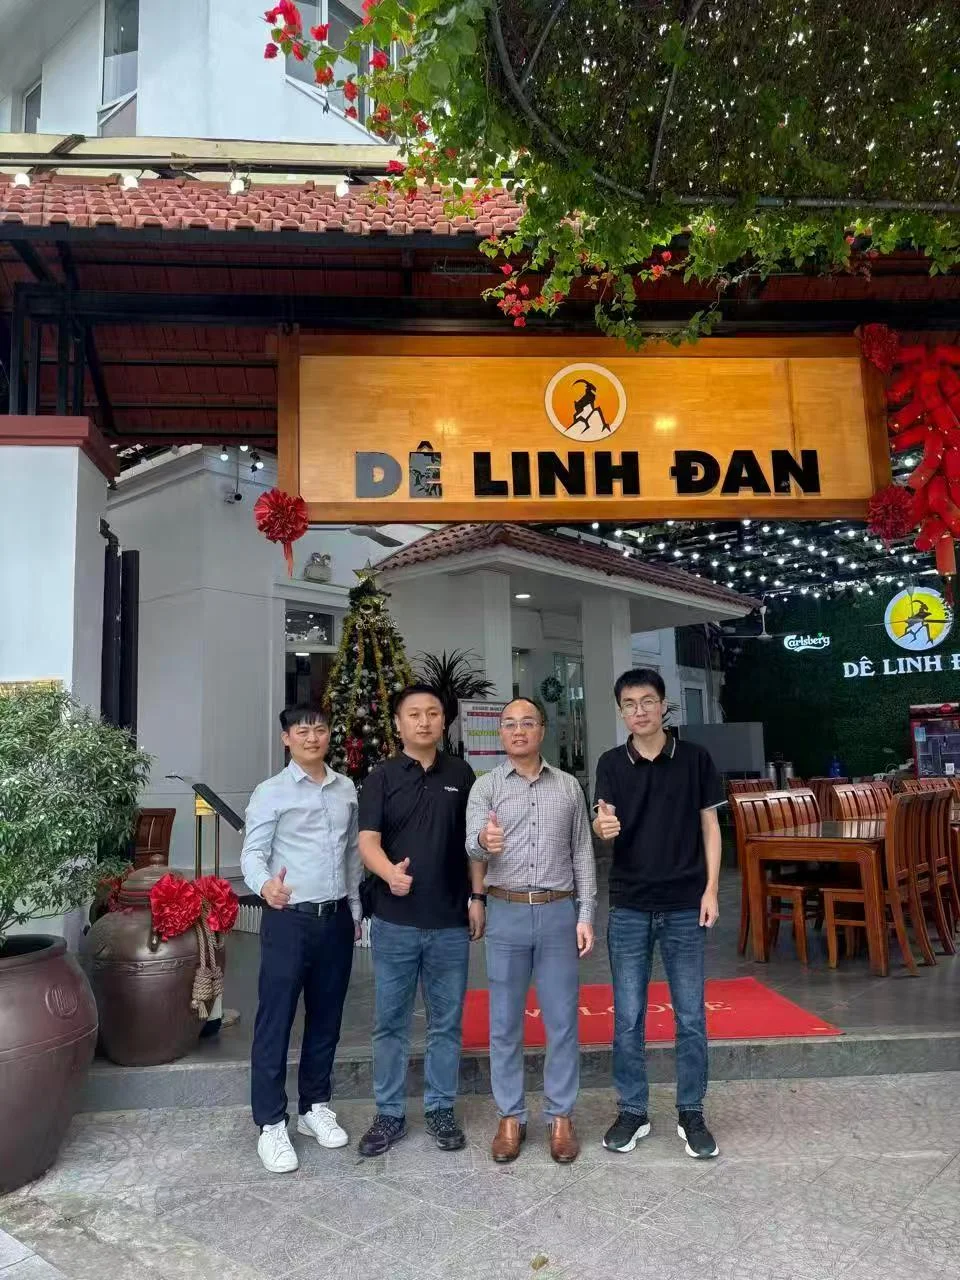
On November 30, 2025, our technical and service team began a 10-day business visit to Vietnam, meeting mining clients face to face to review the operation of vertical sump pumps and discuss technical optimization for upcoming projects.

Aug 10,26
Efficient Horizontal Froth Pump for Industrial Slurry Management
Oct 31,25
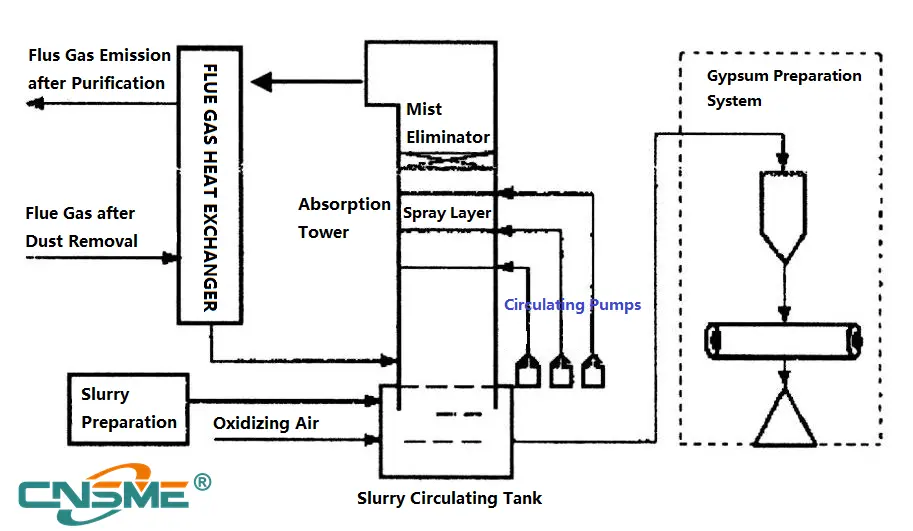
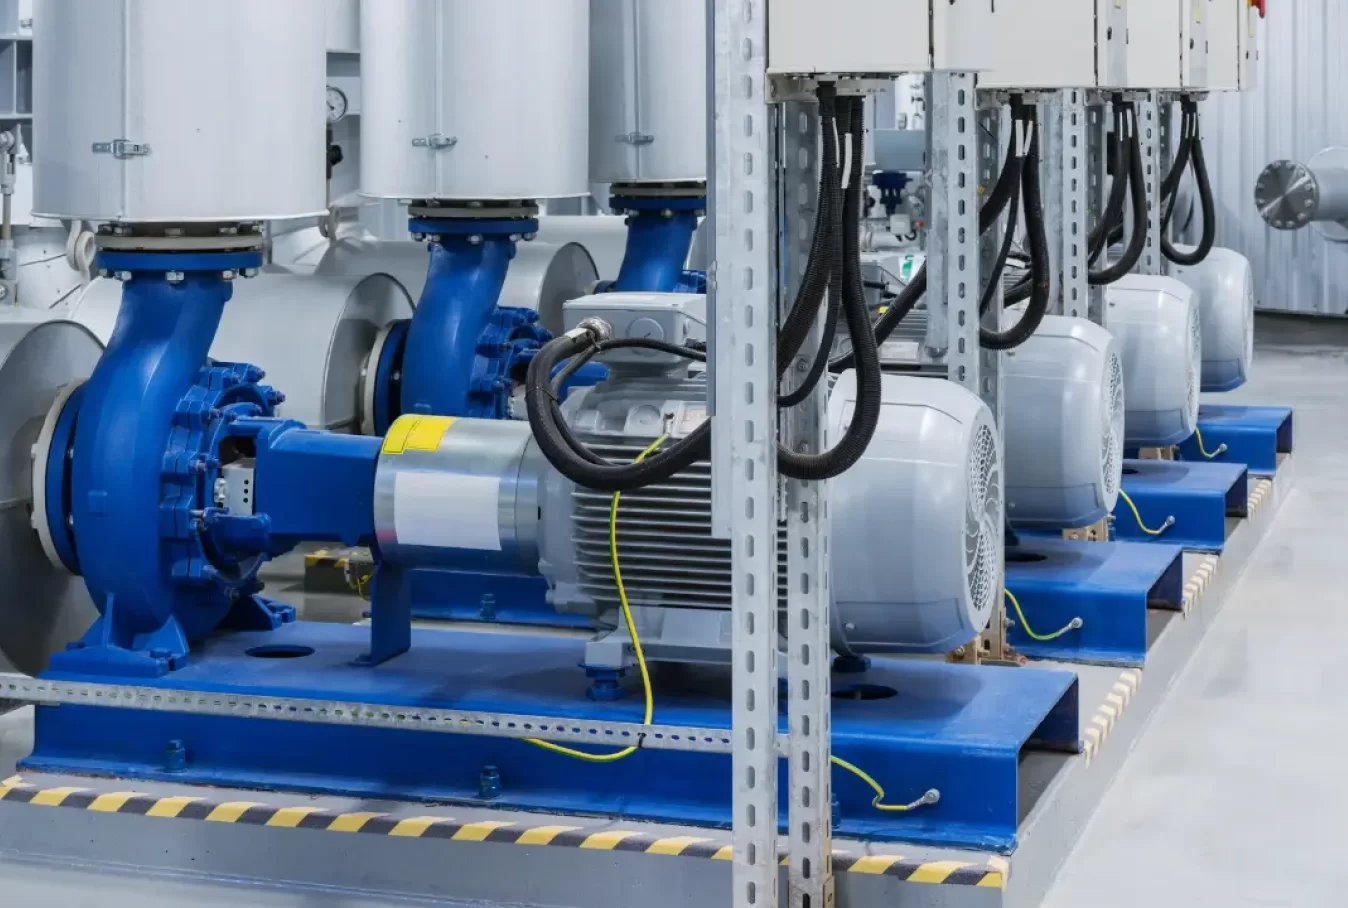
Pumps for Limestone-gypsum wet FGD (Flue Gas Desulfurization) Process
Dec 07,25
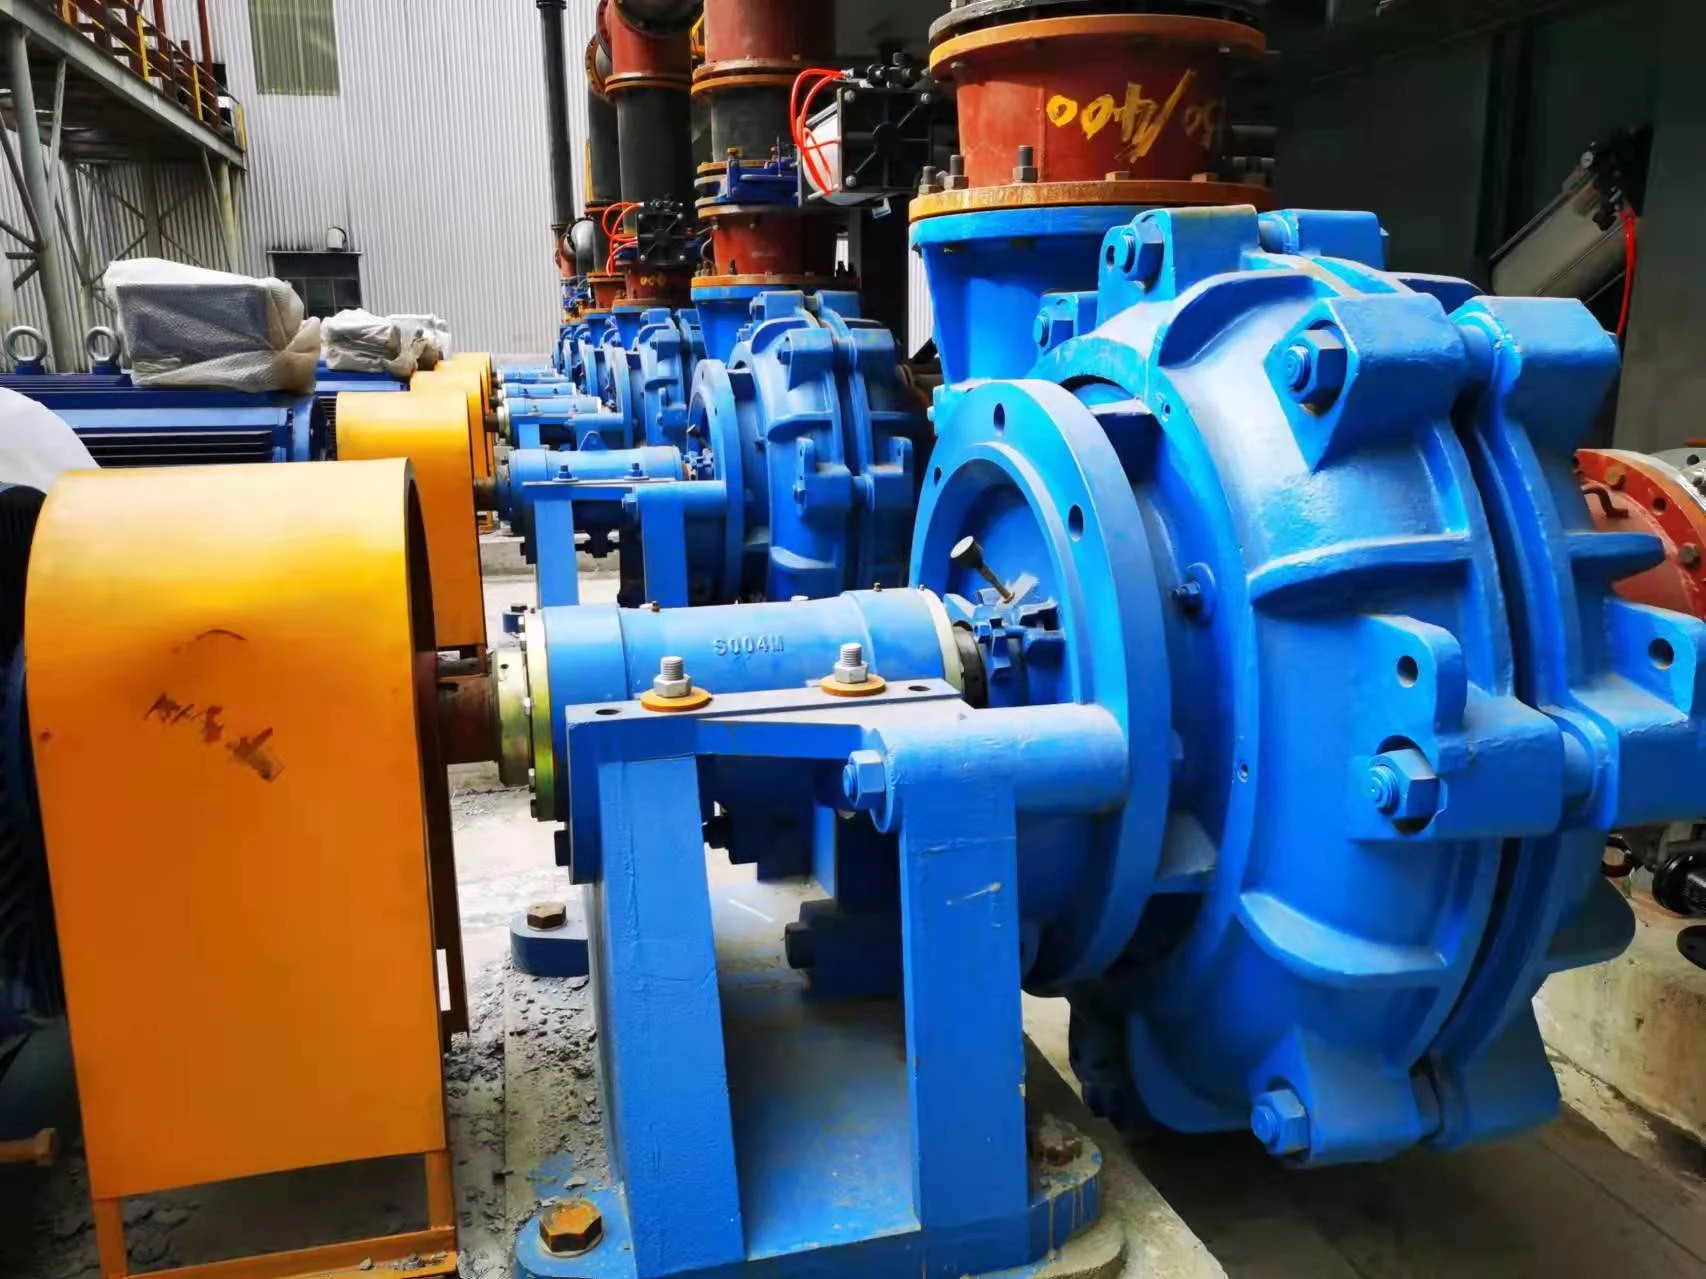
OEM Rubber Lined Slurry Pump Supplier: Durable & Efficient Industrial Solutions
Let's dive into something that might sound niche but is actually a cornerstone of heavy industry worldwide: the OEM rubber lined slurry pump supplier. These suppliers craft pumps that handle the gritty, gritty slurry materials industries churn through daily—think mining, wastewater, chemical processing. Their role? Enabling efficient, reliable movement of abrasive and corrosive mixtures, often in the harshest conditions imaginable. Globally, as industries push for better durability and environmental compliance, understanding these suppliers and their products reveals a story about innovation, sustainability, and economic agility. So why does this matter? Simply put: The right slurry pump drastically cuts downtime, saves costs, and boosts productivity, making all the difference for industrial operations from South America’s mines to Southeast Asia’s processing plants.
Mar 02,26
Optimizing Coal Washing Operations with a Reliable Slurry Pump for Coal Washing Plant
Slurry pump for coal washing plant are critical components in the efficient and economical processing of coal, a vital energy source globally. These pumps are specifically designed to handle the abrasive and corrosive nature of coal slurries, ensuring reliable and continuous operation in demanding environments. Understanding the nuances of these pumps – from their design to their maintenance – is crucial for optimizing coal preparation plants, maximizing recovery rates, and minimizing downtime. The demand for efficient coal washing continues as coal remains a significant part of the energy mix, particularly in developing nations. The global coal market, though facing increasing pressure from renewable energy sources, remains substantial, with significant production and consumption in countries like China, India, and Australia. This drives a consistent need for robust and effective slurry handling solutions. A reliable slurry pump for coal washing plant directly impacts the cost-effectiveness of coal production, influencing energy prices and overall economic stability. The increasing emphasis on environmental regulations also necessitates pumps that minimize water usage and reduce the release of harmful pollutants during the washing process.
Feb 03,26
OEM Dredge Pump Manufacturer Quality Slurry Pump A Comprehensive Guide
Quality Slurry Pump specializes in providing robust and reliable dredge pumps for a wide range of applications.
bscribe newslette