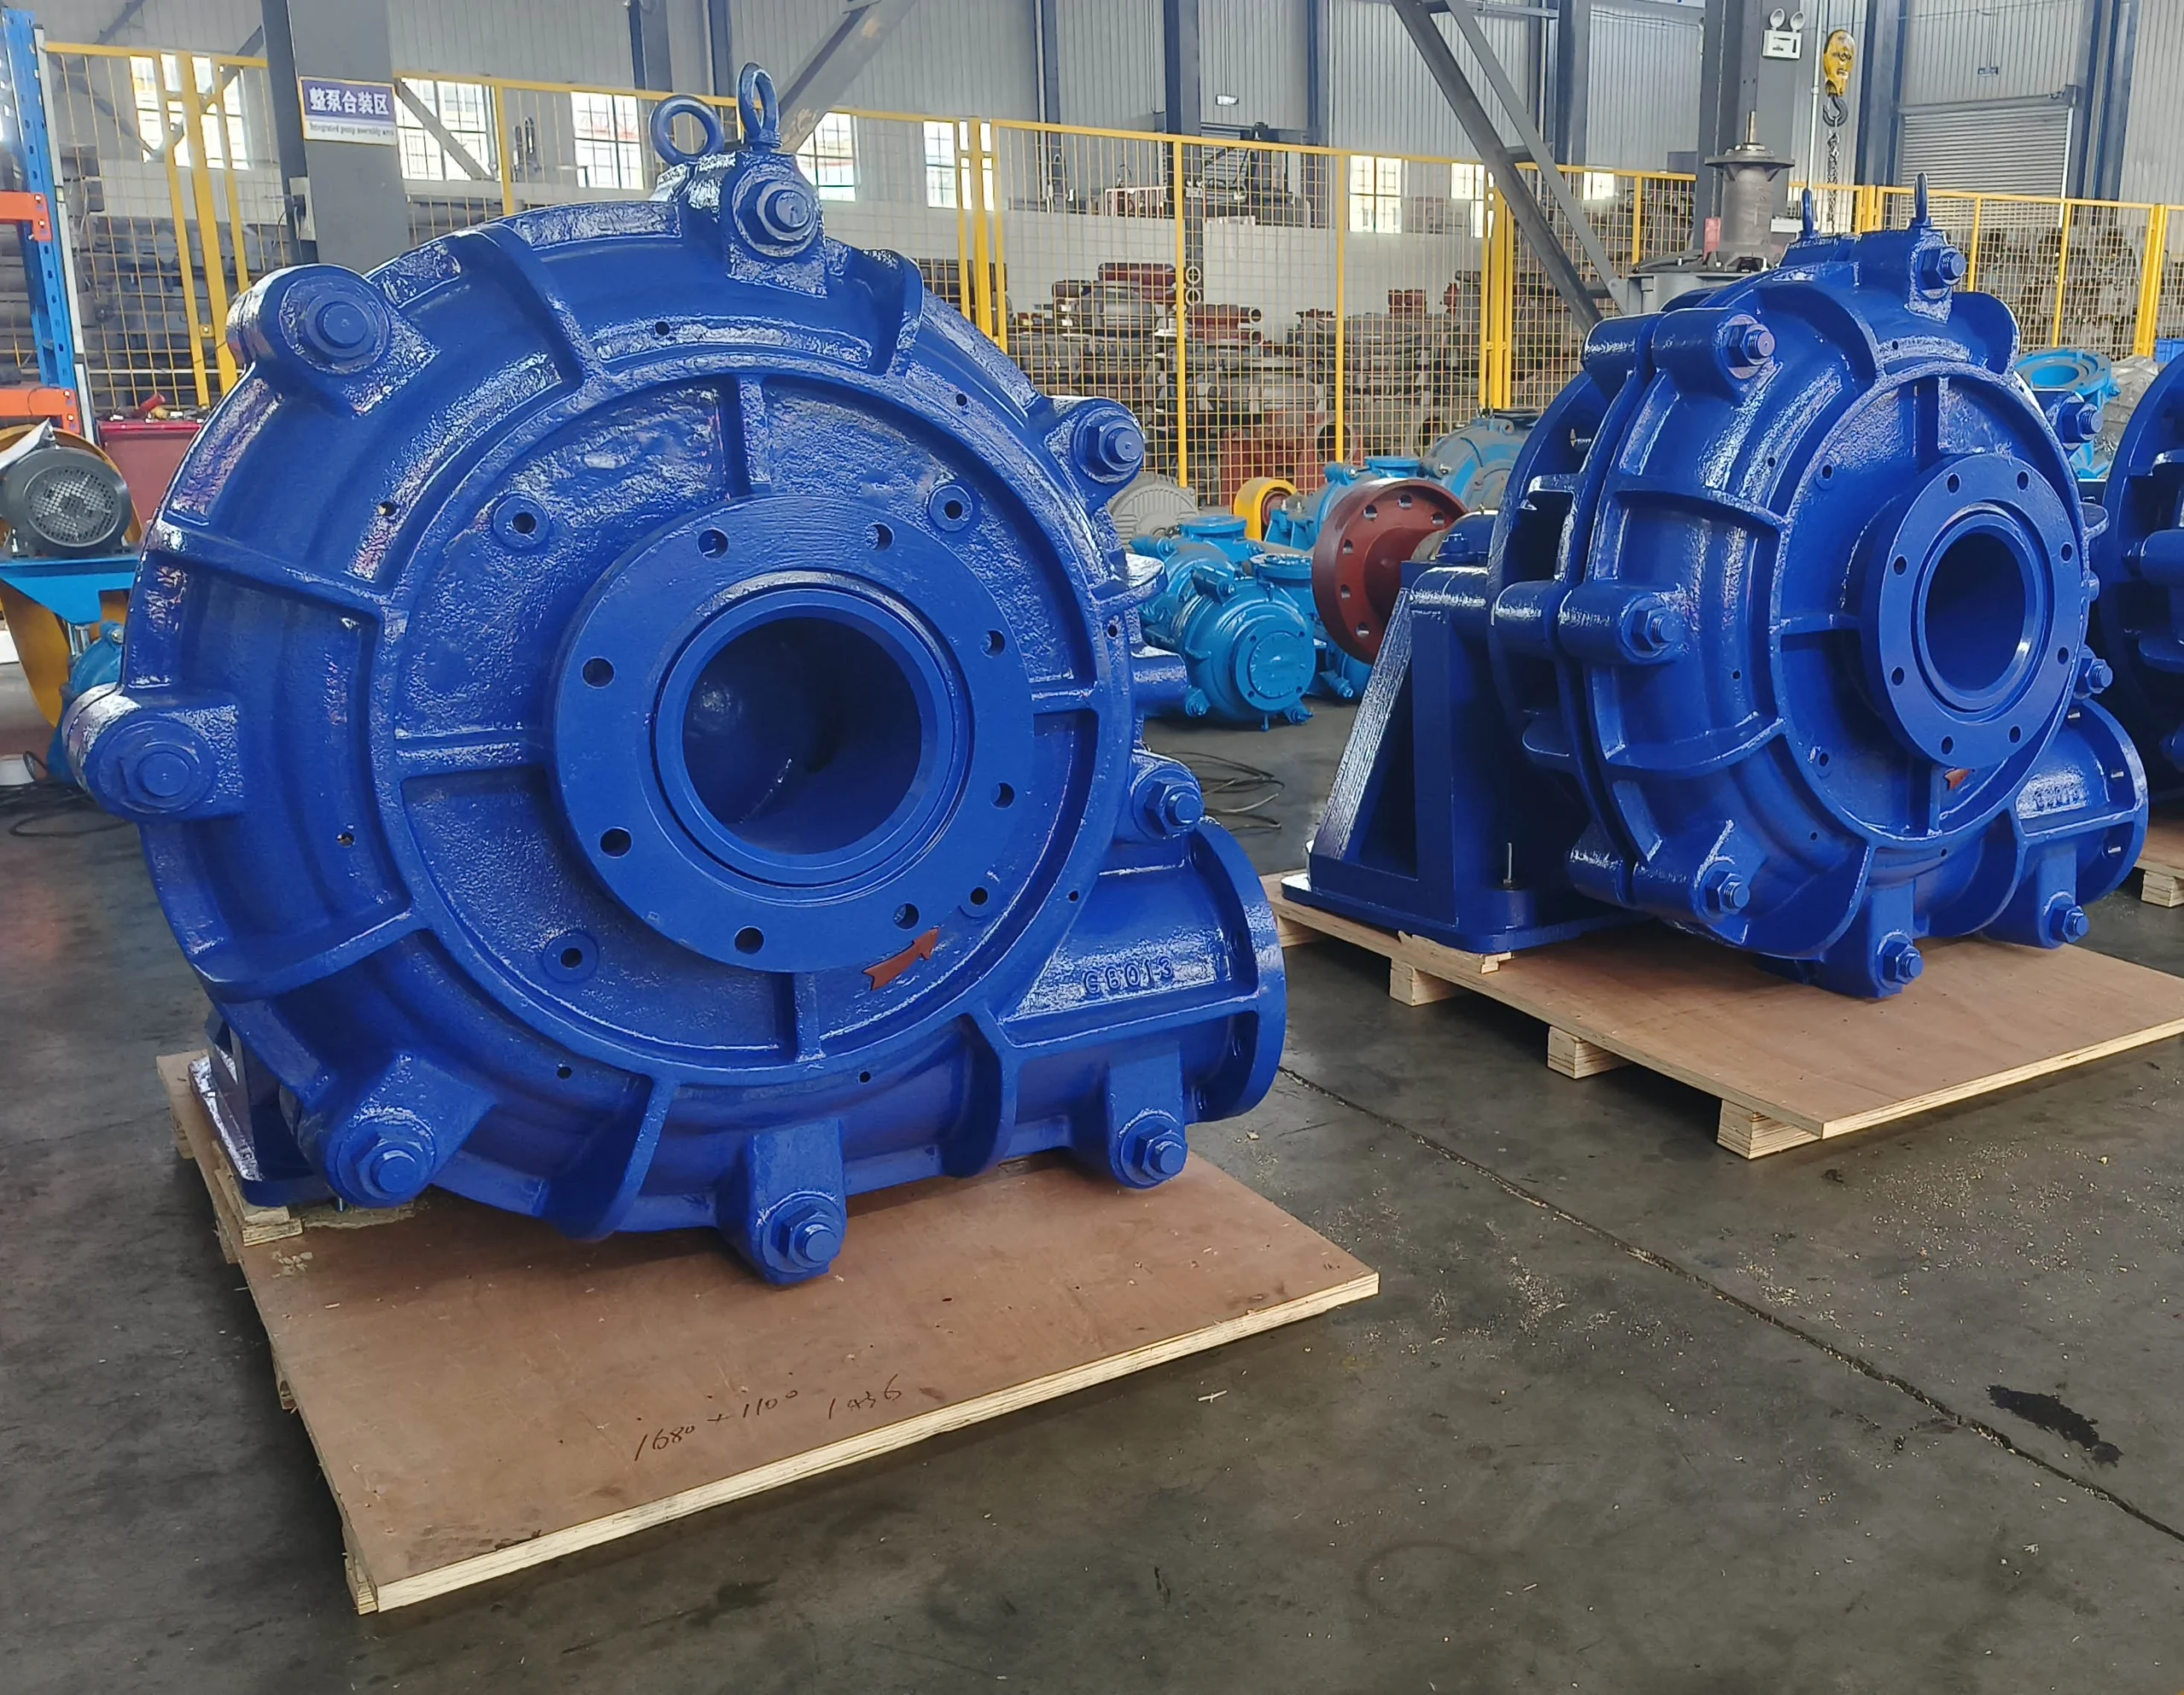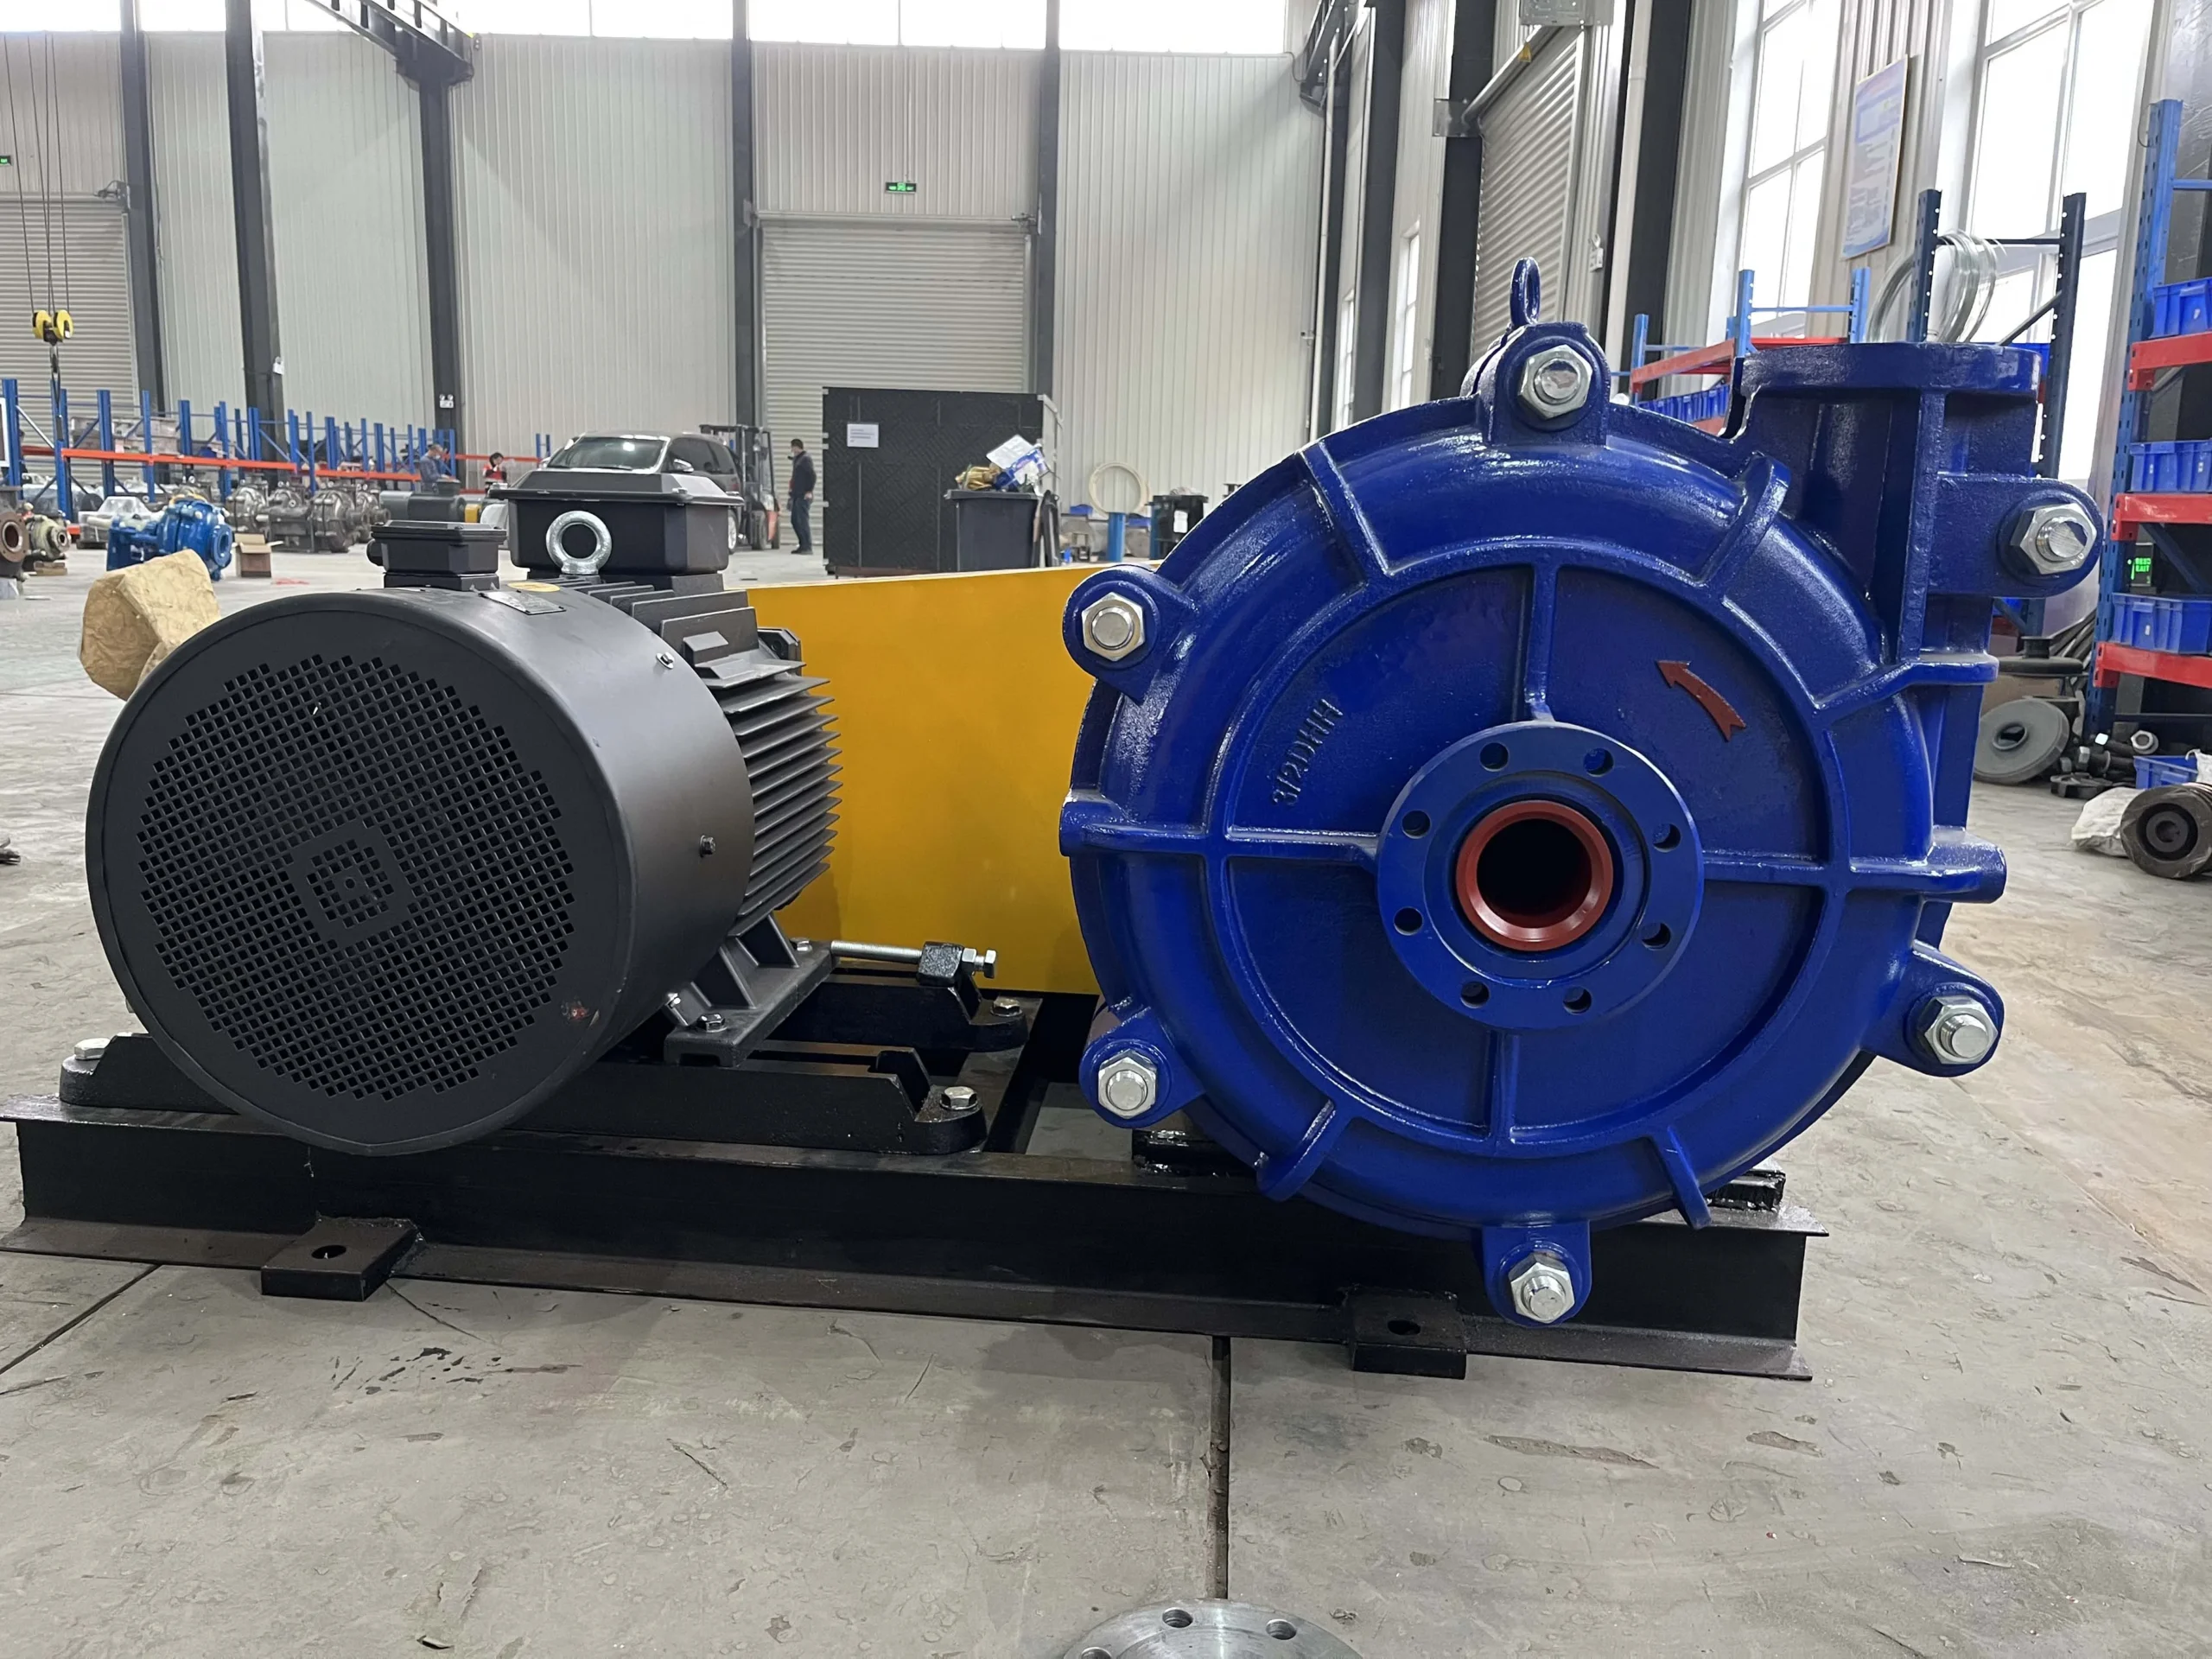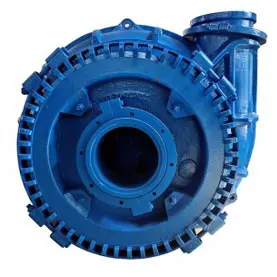
Precision-engineered GAM14147RE1 Impellers for 1614TU-AH pumps, delivering unmatched abrasion resistance and hydrodynamic efficiency in the harshest metallurgical environments. 5000 Annual Output 120 Countries Served 7 Days Sample Lead Time 99.9 On-Time Delivery Industrial Grade Performance for slurry pump for metallurgy plant The GAM14147RE1 Impeller stands as a critical component precision-engineered for 1614TU-AH horizontal heavy-duty slurry pumps. By utilizing premium A05 high chrome alloy, it establishes a new benchmark in metallurgy plants where transporting coarse, highly abrasive slurries is the primary operational challenge. Our technical edge lies in the hydrodynamic optimization of vane angles and flow channels.
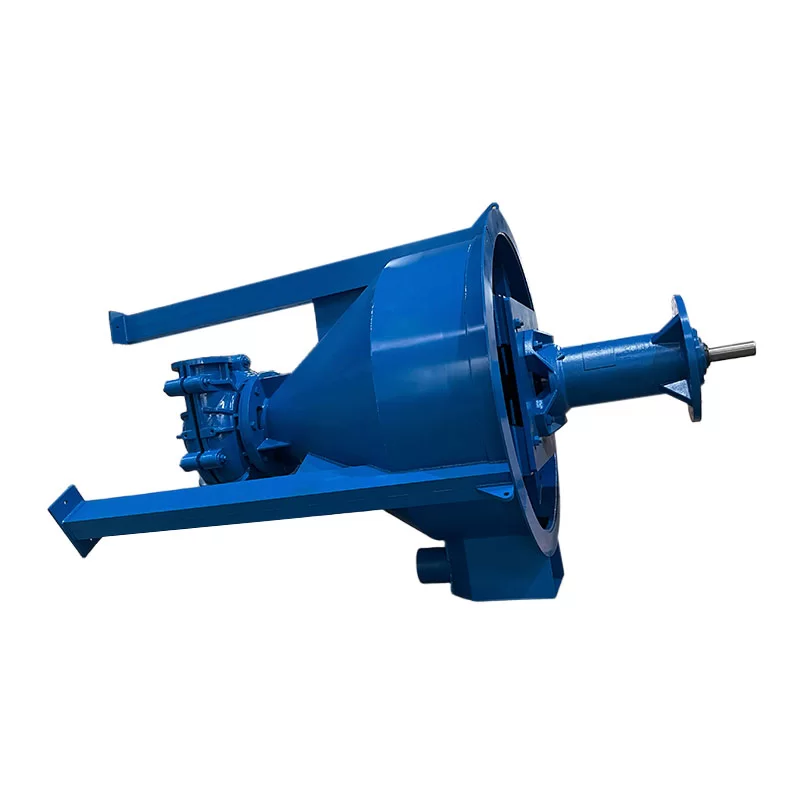
Selecting the right expeller for your slurry pump is crucial for optimal performance and longevity. As a leading OEM slurry pump expeller factory, we at Quality Slurry Pump specialize in manufacturing high-quality, custom-engineered expellers to meet the diverse needs of various industries. This article will delve into the importance of expellers, the materials used, customization options, and why choosing a reliable factory like ours is essential.
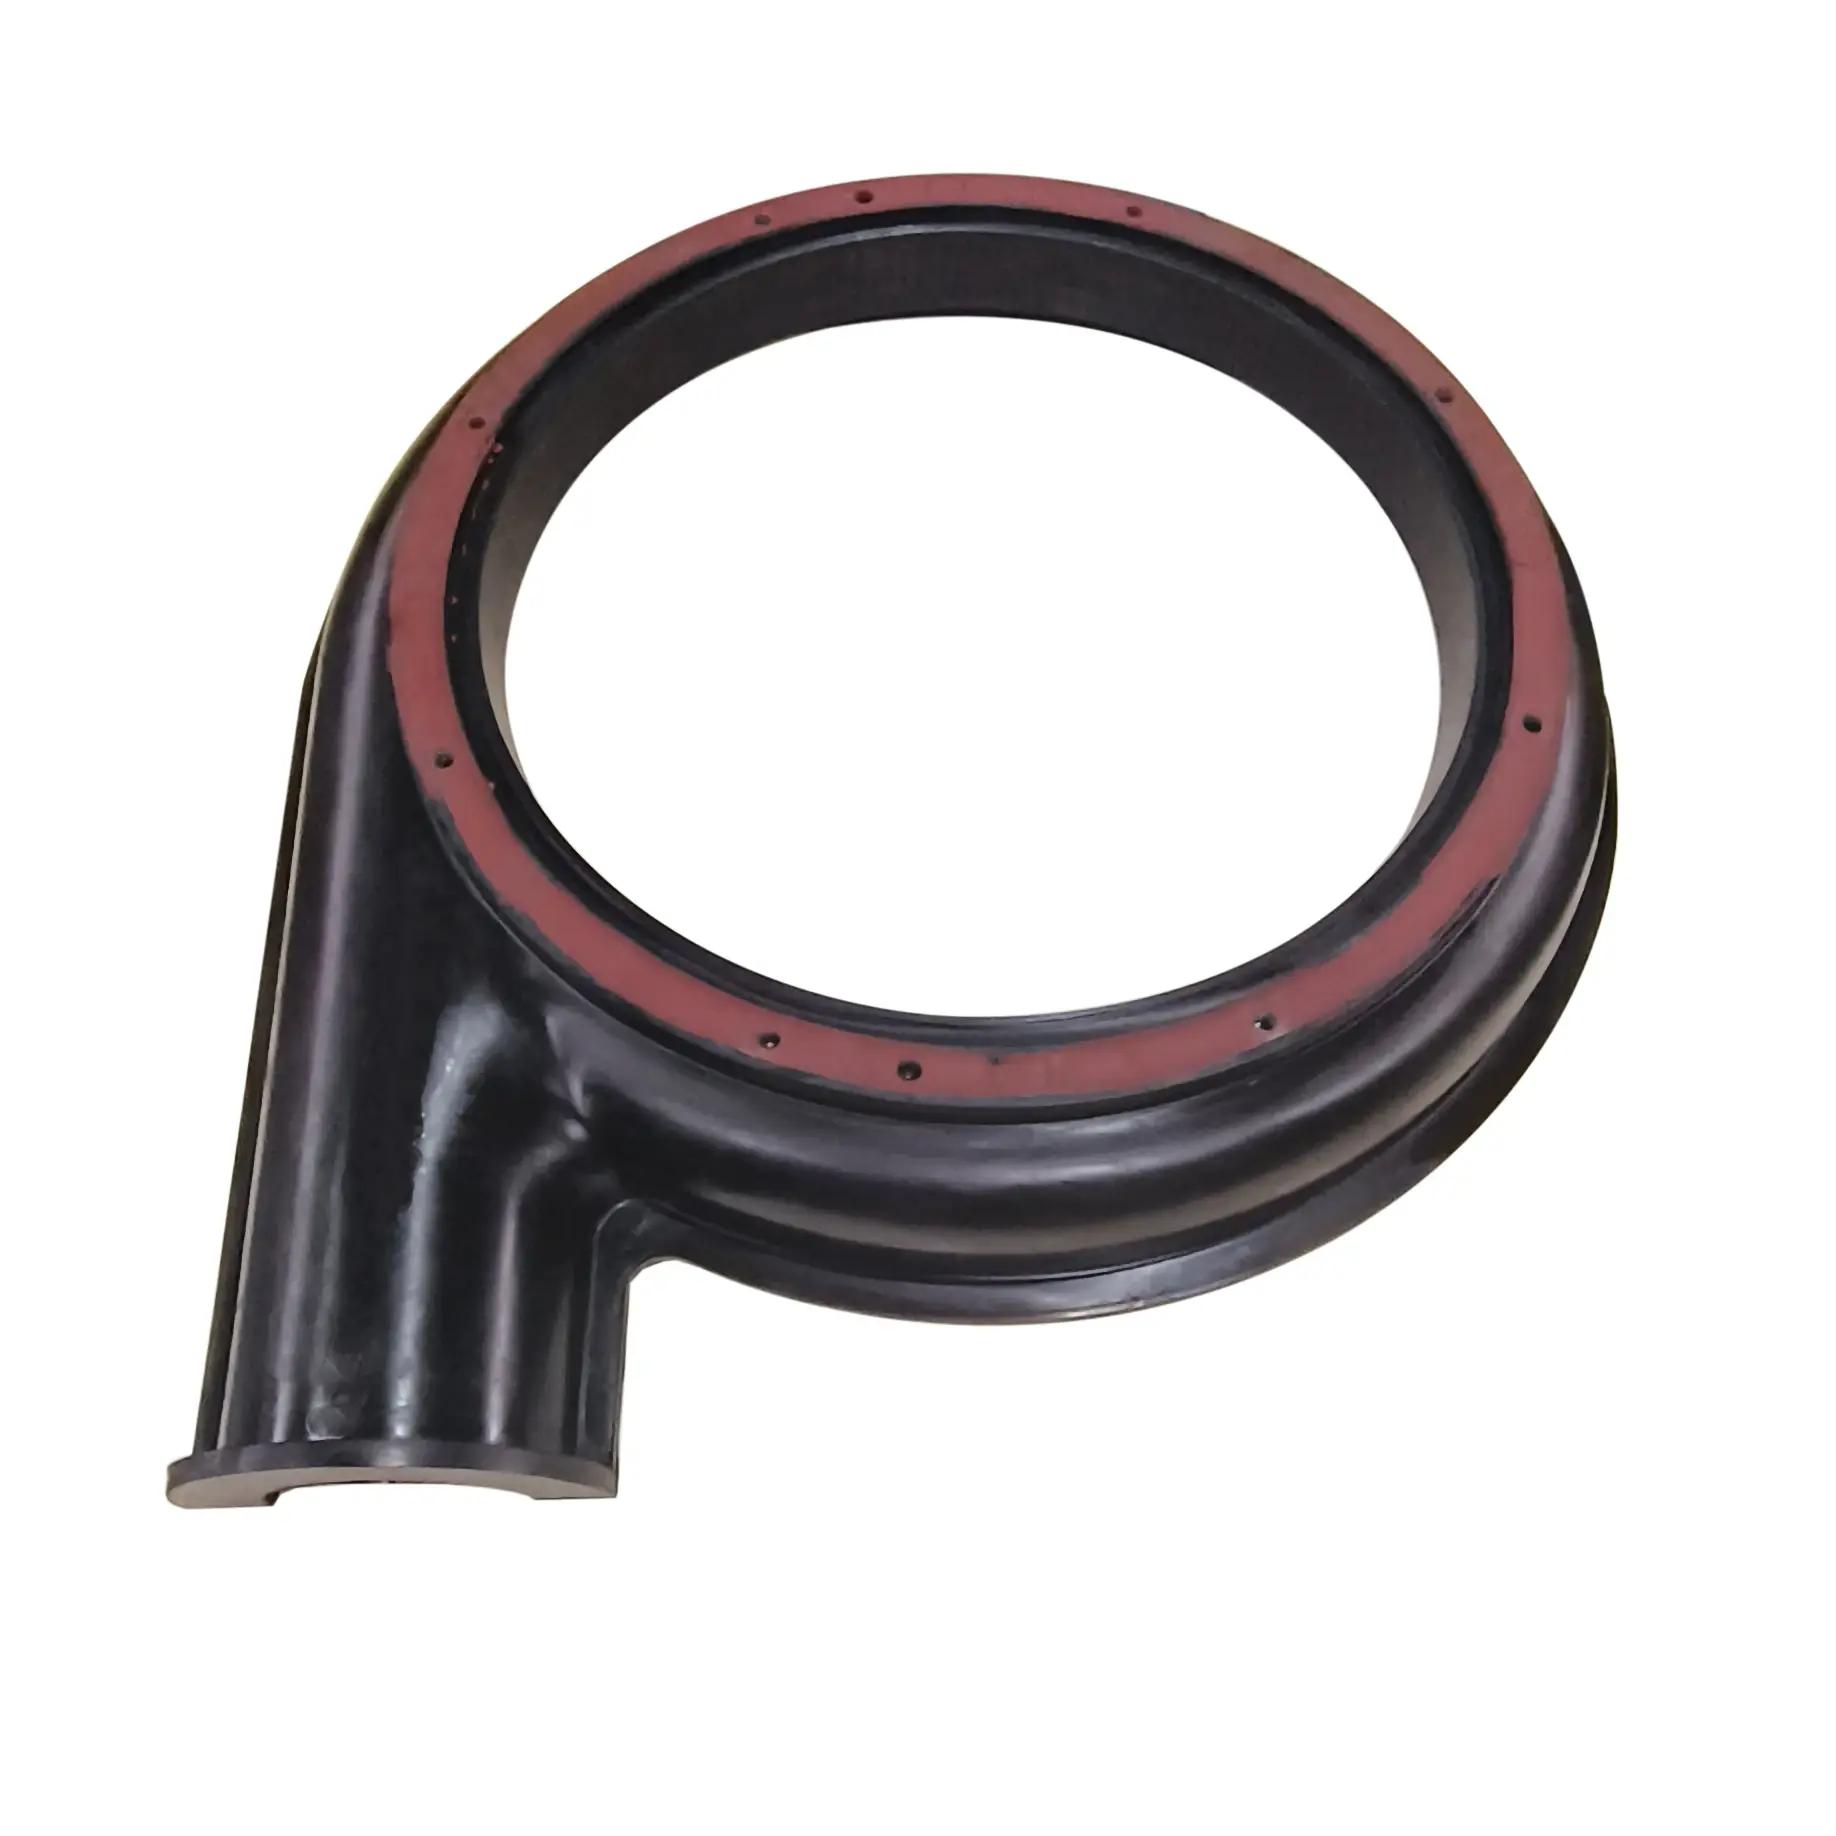
Maintaining the operational efficiency of heavy-duty slurry equipment requires a strategic approach to maintenance, where the quality of warman pump replacement parts plays a pivotal role. In the demanding environments of mining and mineral processing, the continuous abrasion of slurry leads to inevitable wear, making the availability of high-precision components essential for avoiding costly unplanned downtime. Across the global industrial landscape, the reliance on standardized yet high-performance slurry pumps has created a significant market for compatible replacement components. By utilizing premium warman pump replacement parts, operators can extend the mean time between failures (MTBF), ensuring that production targets are met
Slurry pump for mining operations are critical components in mineral processing, handling abrasive and corrosive materials essential for extracting valuable resources. The global mining industry relies heavily on efficient and reliable slurry pumps to transport these mixtures – a vital link in the value chain from extraction to refining. Effective slurry pumping reduces operational costs, enhances productivity, and minimizes environmental impact by optimizing material handling processes. The demand for slurry pump for mining solutions is intrinsically linked to global economic growth, particularly in developing nations with expanding mining sectors. As resource demand increases, so does the need for robust and scalable pumping systems. Recent advancements focus on improving pump efficiency, reducing energy consumption, and extending operational lifespan in harsh mining environments, contributing to more sustainable mining practices. Understanding the intricacies of slurry pump for mining is essential for mining engineers, plant managers, and industry stakeholders.
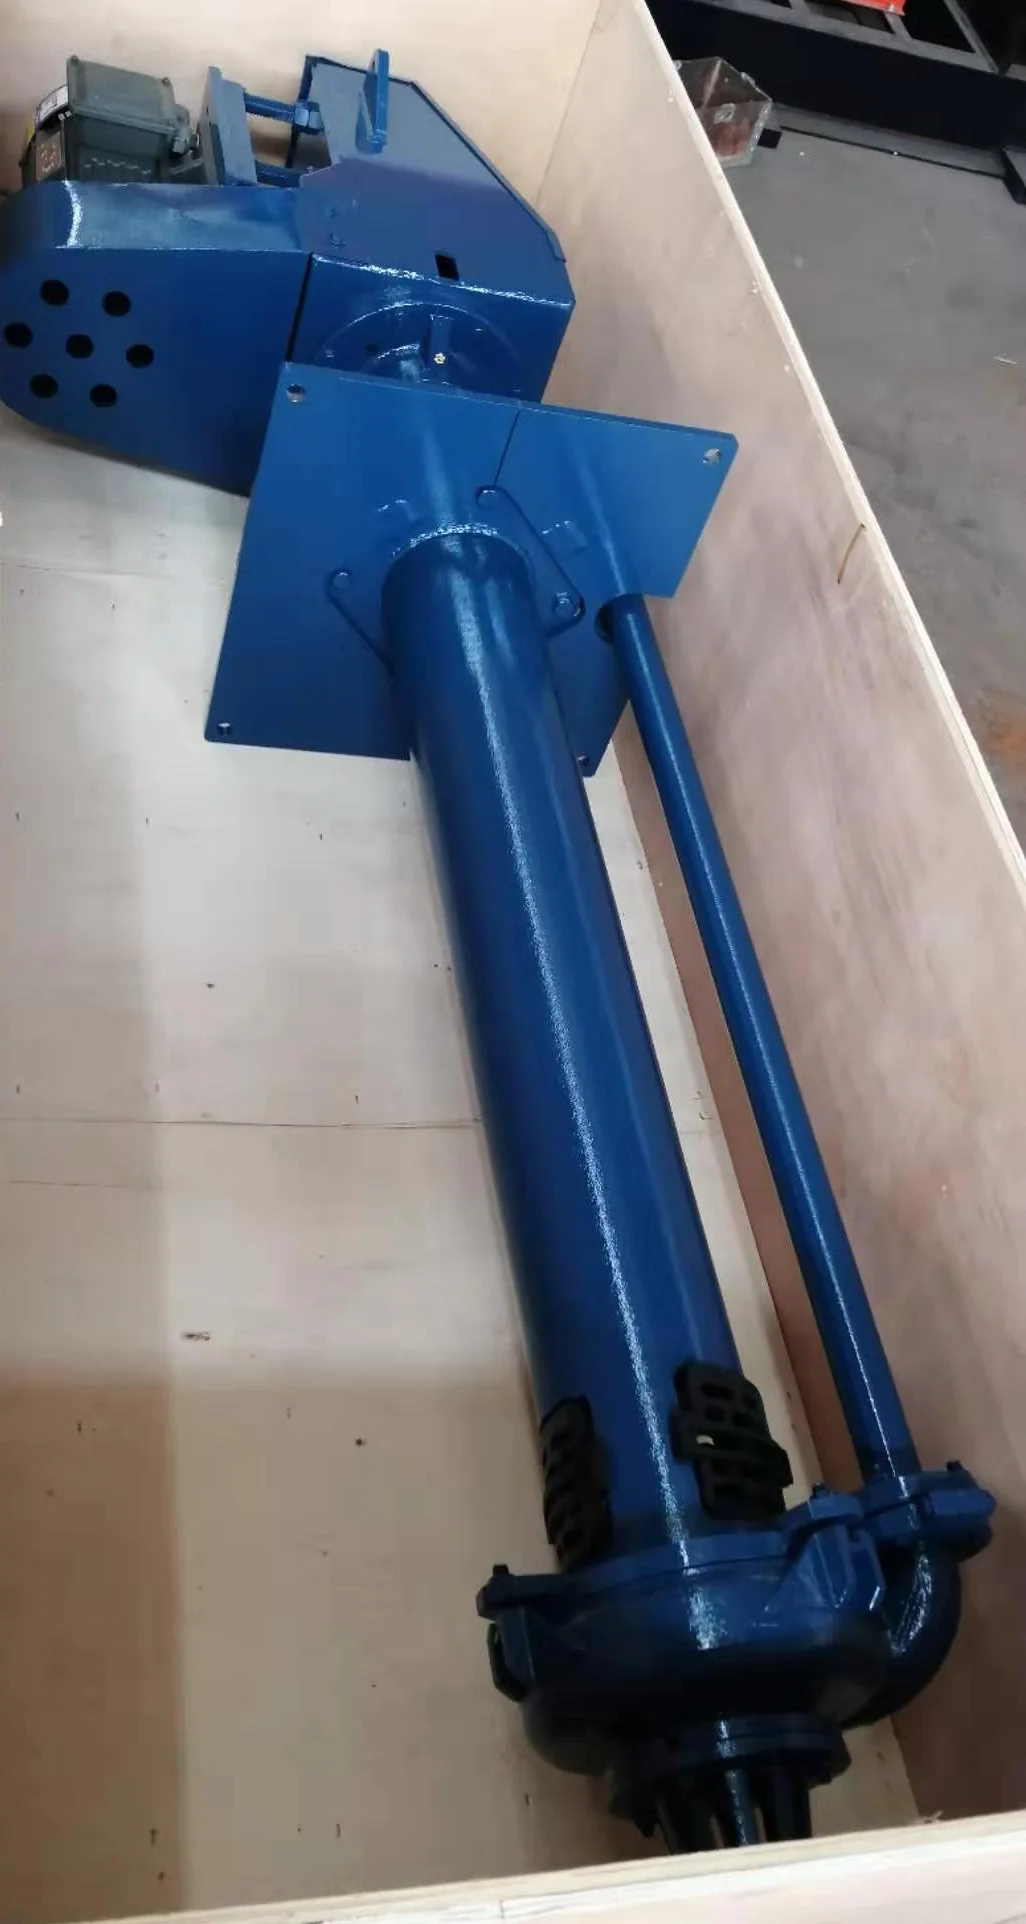
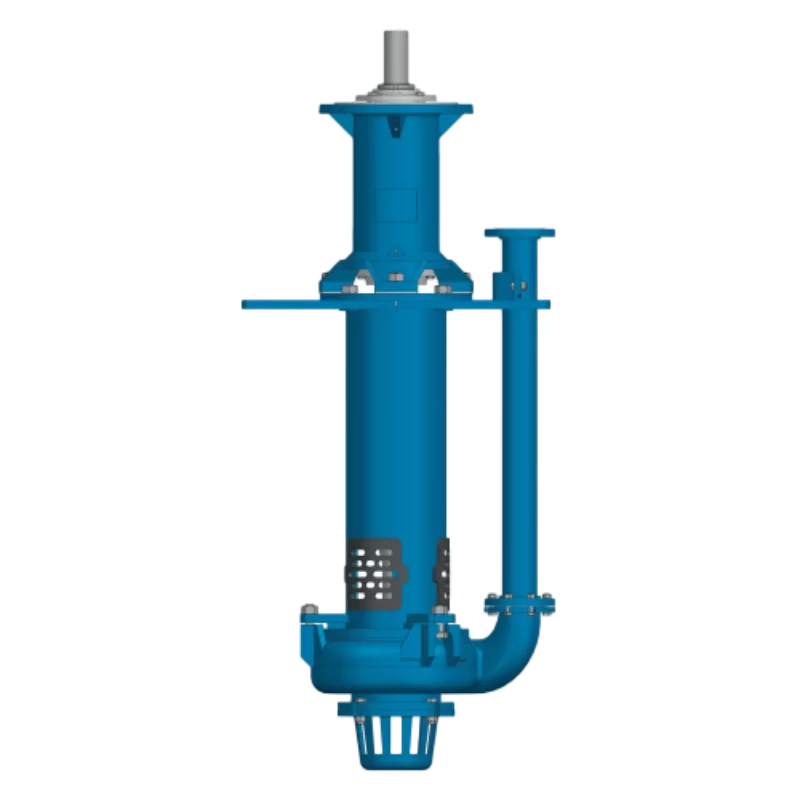
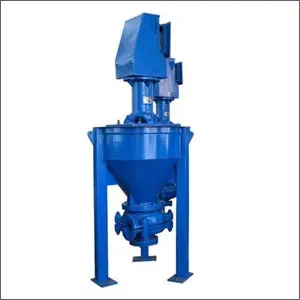
Vertical sump pump design is more than just moving water; it’s about keeping operations running smoothly, safely, and efficiently. From massive dewatering projects in mining to reliable wastewater management in industrial plants, the right pump can be the difference between productivity and costly downtime. As someone who’s spent years on sites, wrestling with equipment and troubleshooting issues, I can tell you that a well-designed vertical sump pump is an absolute workhorse. It's the foundation of so many processes, and getting it right upfront saves a world of headache later.