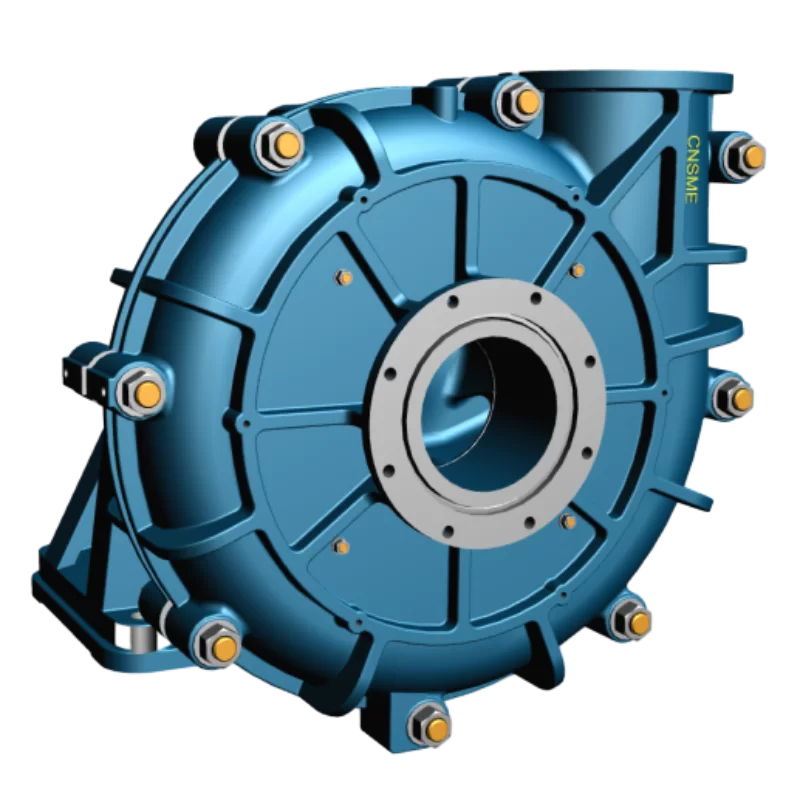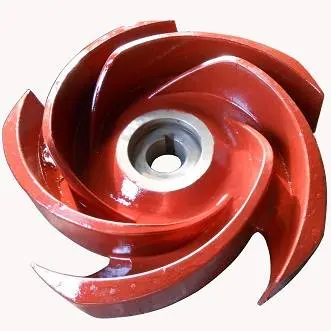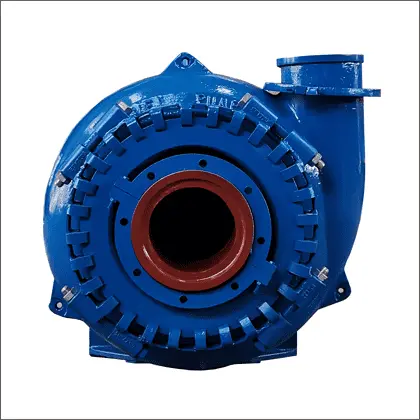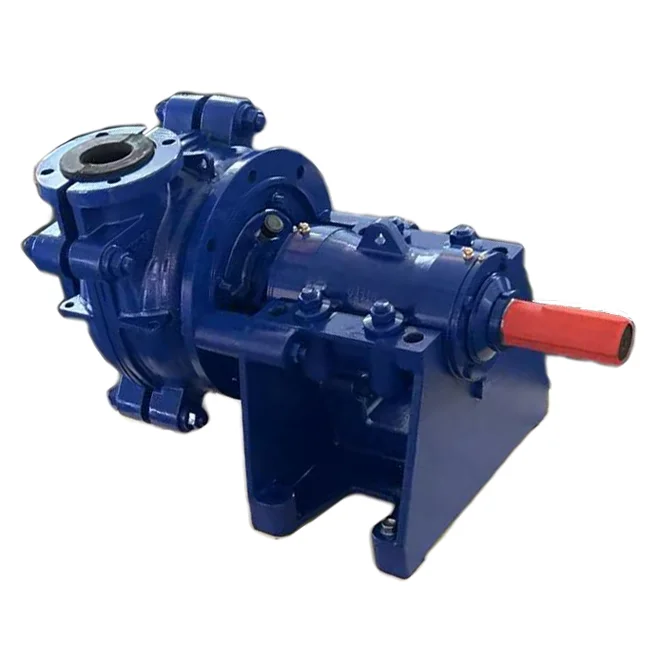
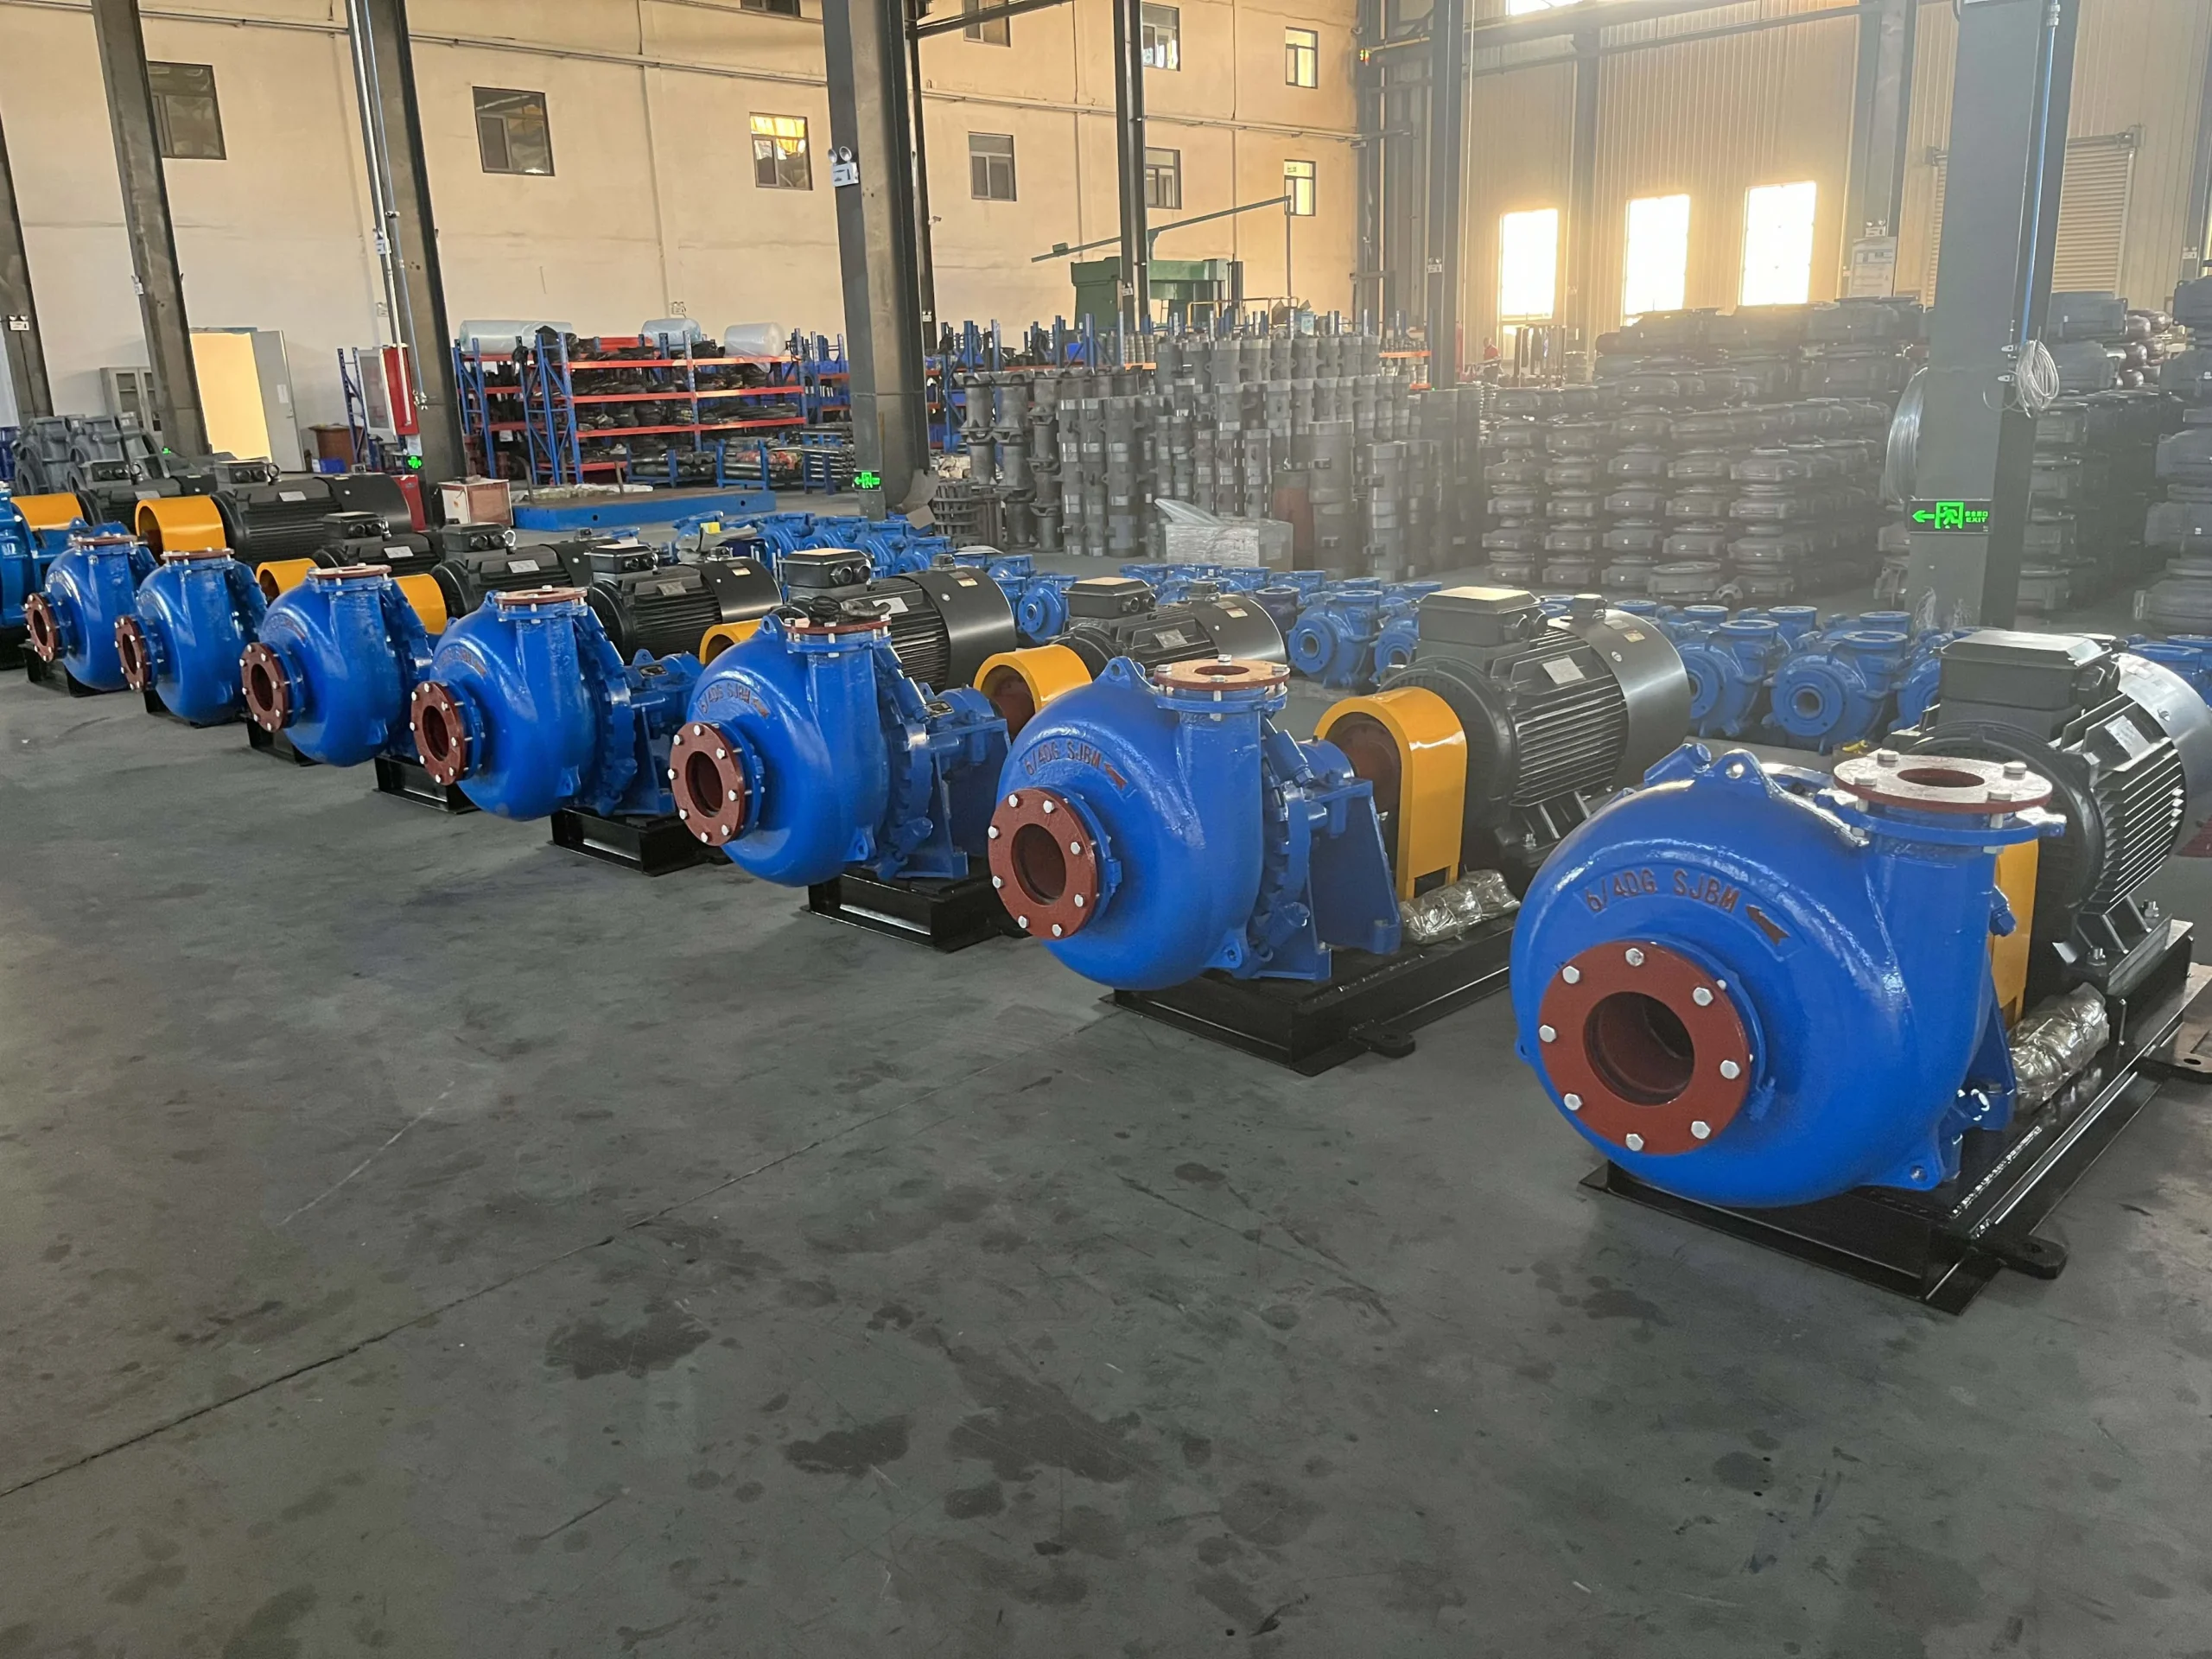
Slurry pump casings are critical components in a vast array of industrial processes, responsible for containing and directing abrasive and corrosive fluids. Their design and material selection directly impact the efficiency, reliability, and longevity of slurry pumping systems. Understanding the intricacies of slurry pump casing construction is paramount for engineers, operators, and maintenance personnel involved in industries like mining, wastewater treatment, and chemical processing. The global demand for robust and effective slurry handling solutions continues to grow, driving innovation in casing materials and designs. The significance of a well-engineered slurry pump casing extends beyond simply housing the impeller and volute. It directly affects hydraulic performance, minimizing energy consumption and maximizing throughput. A compromised casing can lead to catastrophic failures, resulting in costly downtime, environmental damage, and safety hazards. Consequently, the selection and maintenance of slurry pump casings are essential for sustainable and profitable operations.
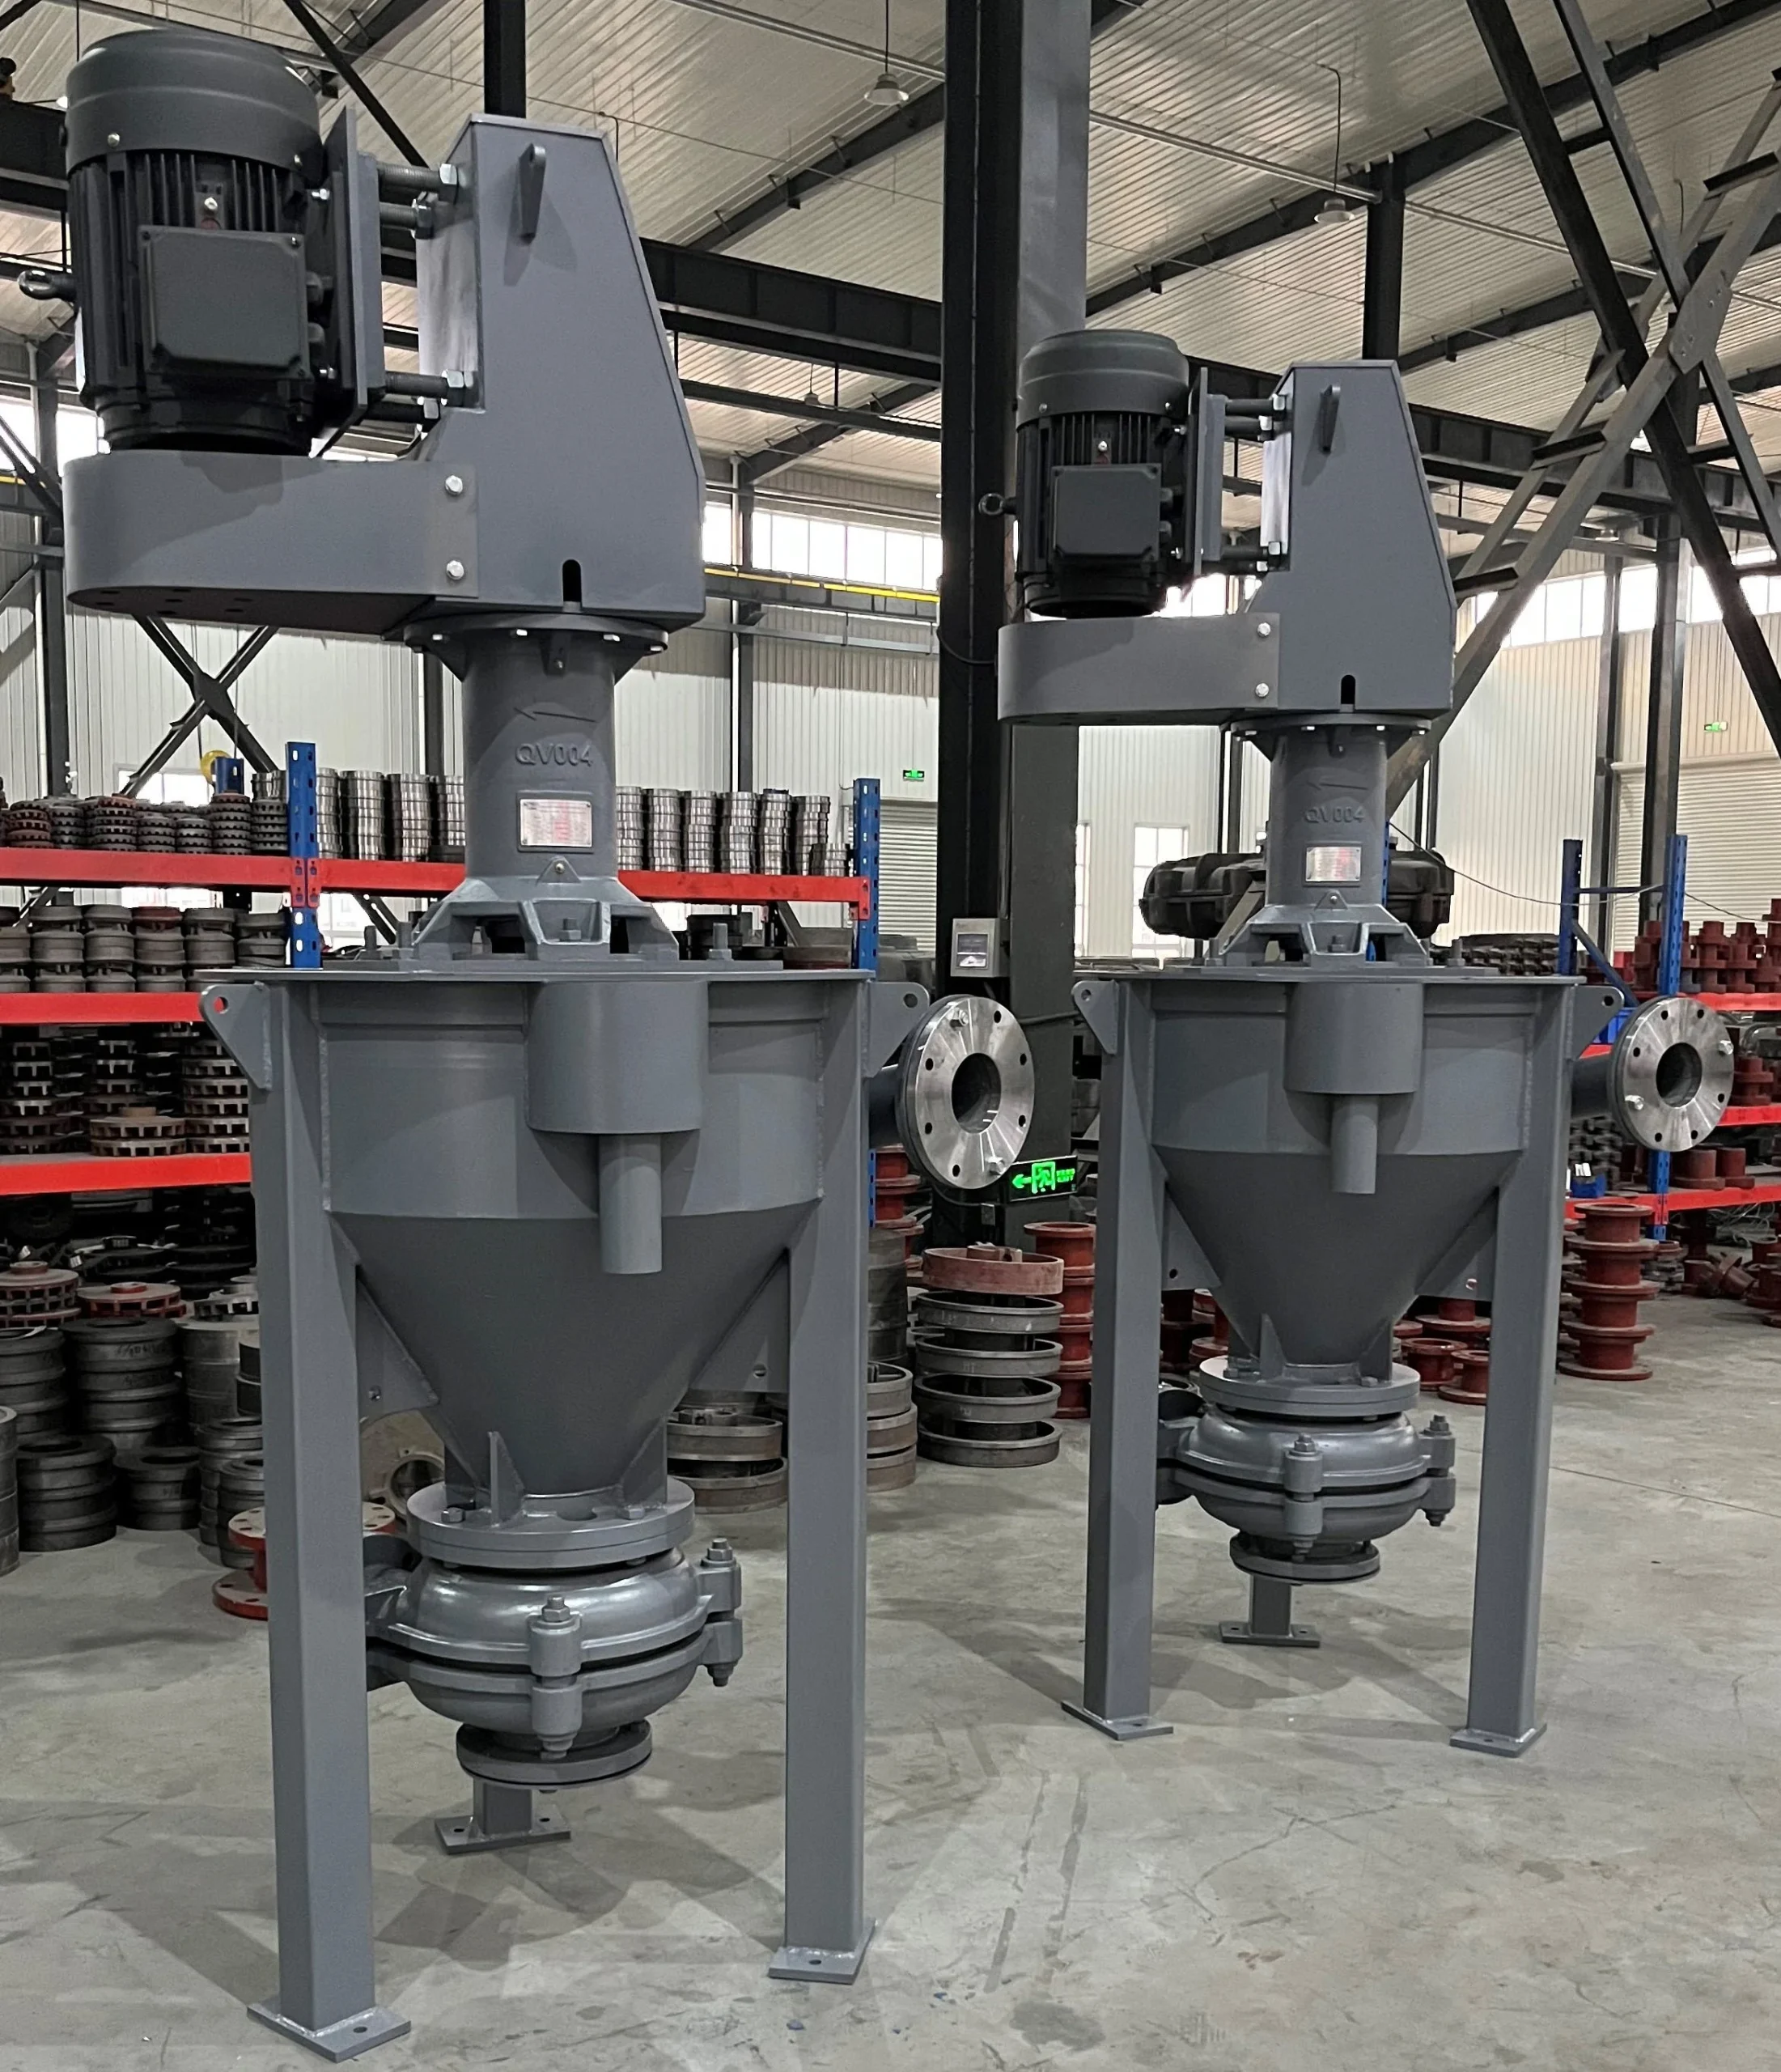
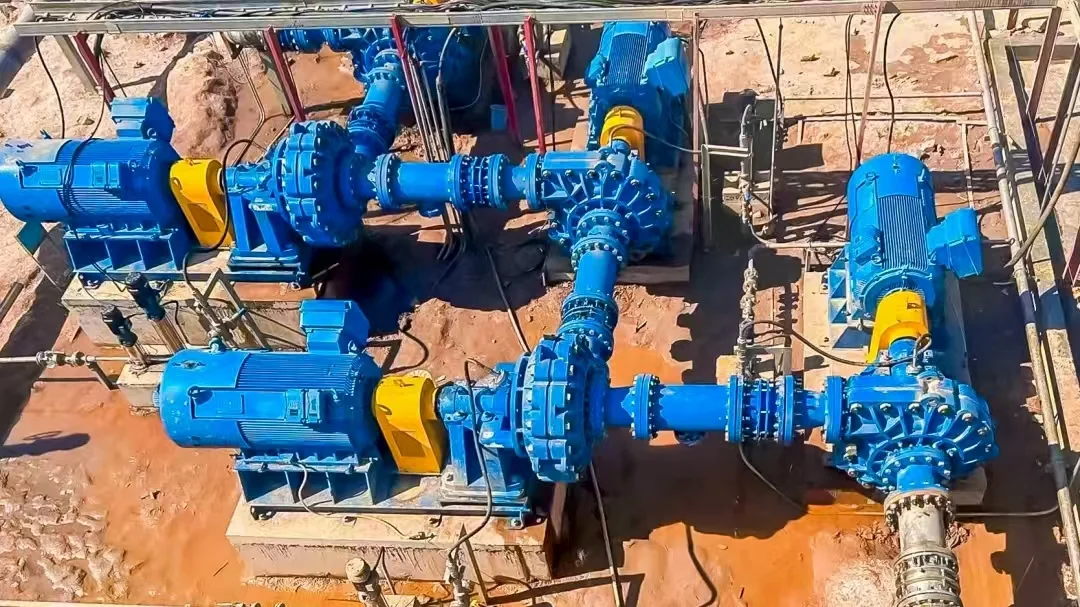
Slurry pumps are designed to convey high-concentration, high-viscosity, corrosive media with substantial particulate content. For large volumes of highly viscous slurry, it is sometimes necessary to employ two or more slurry pumps to accomplish the task.
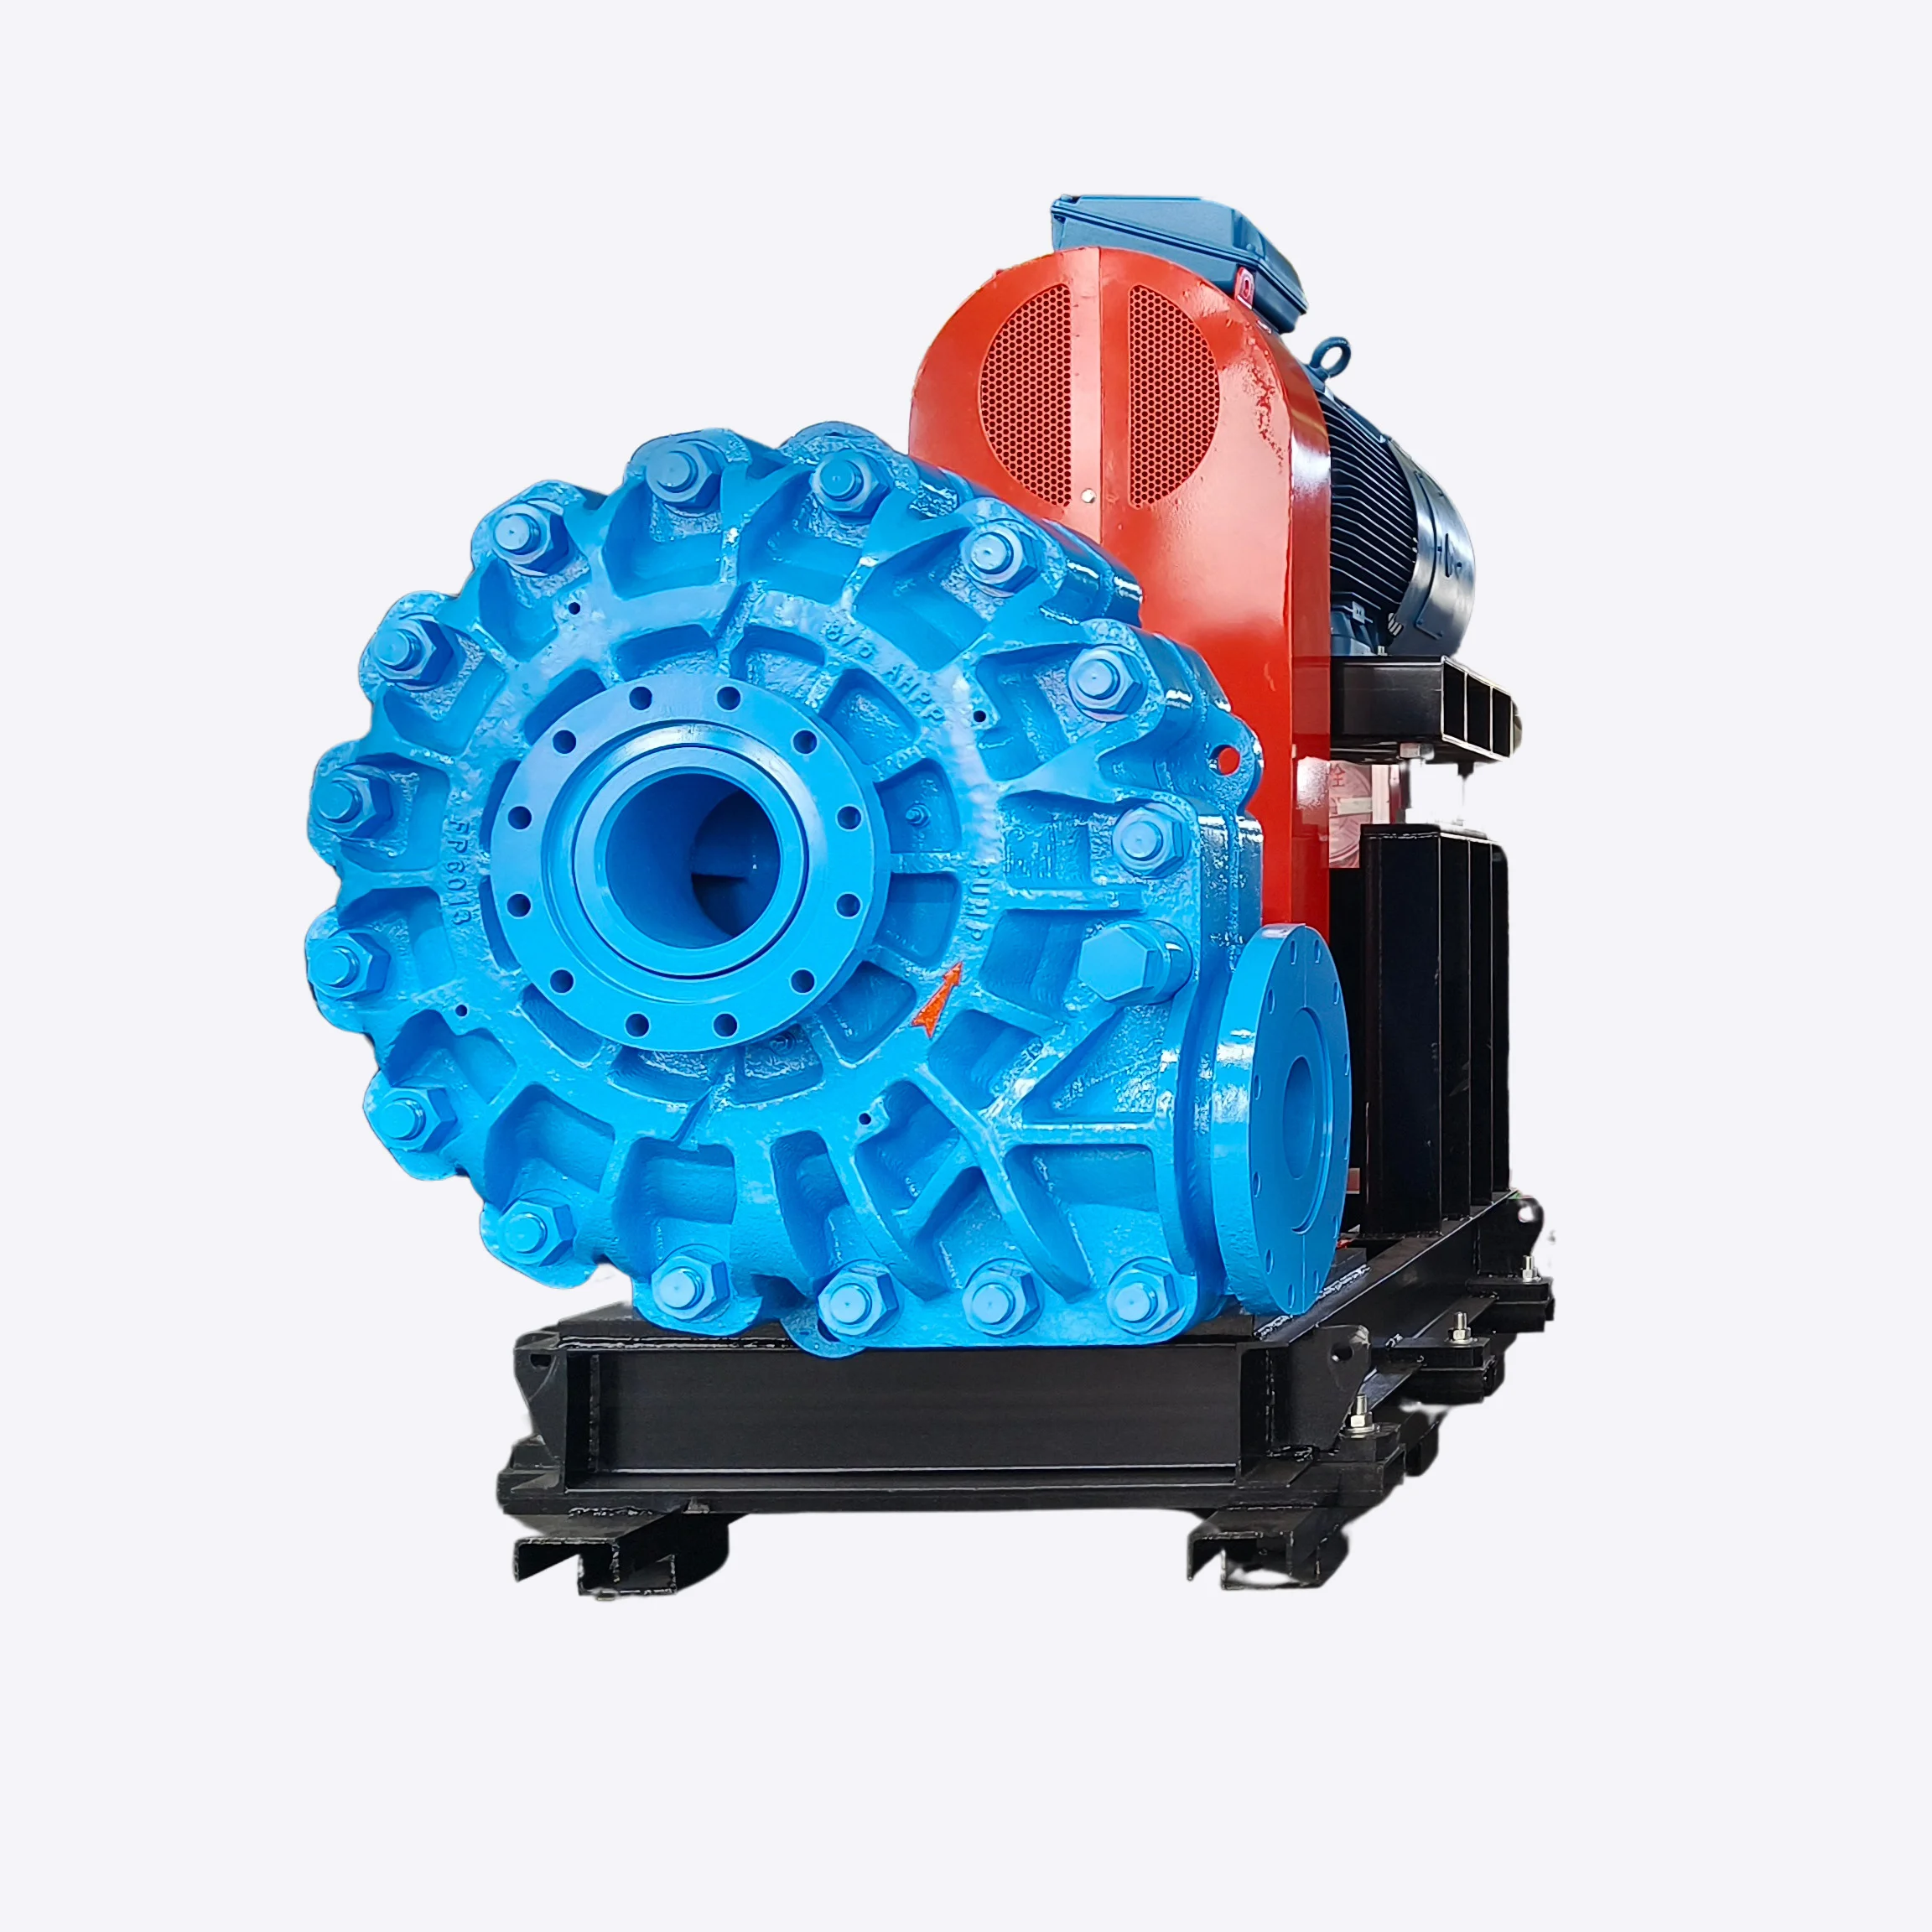
Slurry pump for gold mining plays a crucial role in the extraction and processing of gold, a globally significant precious metal. From alluvial deposits to hard rock mining operations, efficient slurry pumping is essential for moving ore, tailings, and process water. The demand for gold, driven by economic factors, investment, and industrial applications, necessitates robust and reliable slurry pump systems. This makes understanding the nuances of slurry pump technology for gold mining vital for efficient and sustainable operations. The global gold mining industry faces increasing challenges, including dwindling high-grade ore reserves, stricter environmental regulations, and the need for cost optimization. Slurry pumps are at the heart of addressing these challenges. Selecting the right slurry pump for gold mining is no longer simply a matter of capacity; it requires careful consideration of abrasion resistance, solids handling capabilities, energy efficiency, and long-term reliability. The success of a gold mining project is intrinsically linked to the performance of its slurry pumping infrastructure.
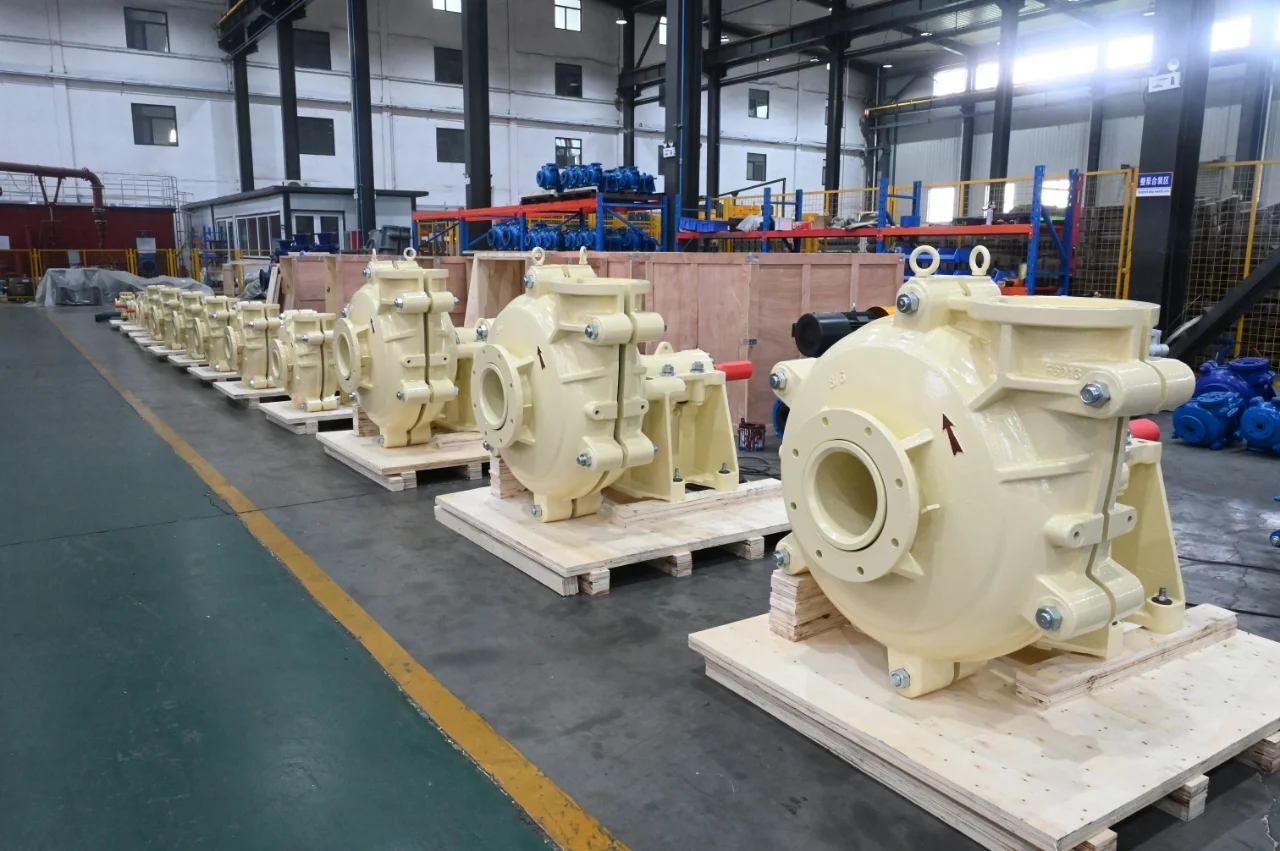
In the demanding world of industrial mineral processing and waste management, the efficiency of slurry transport systems is paramount. Finding reliable Warman interchangeable slurry pump parts is not merely a maintenance requirement but a strategic necessity to ensure continuous operational uptime and prevent costly unplanned shutdowns. The global demand for high-performance pumping solutions has surged as mining and chemical industries move toward more corrosive and abrasive media. Utilizing precision-engineered components ensures that the pumps hydraulic efficiency remains peak, significantly reducing the total cost of ownership through extended wear-life and reduced energy consumption.
Selecting a reliable OEM slurry pump factory is a critical strategic decision for mining, dredging, and industrial processing operations worldwide. Slurry pumps are the heart of material transport in harsh environments, handling abrasive solids and corrosive liquids that would destroy standard pumping equipment. By partnering with an Original Equipment Manufacturer (OEM), companies can ensure that their hardware is engineered to the exact specifications of their unique slurry chemistry and flow requirements.